







Net price: €126.32
Description
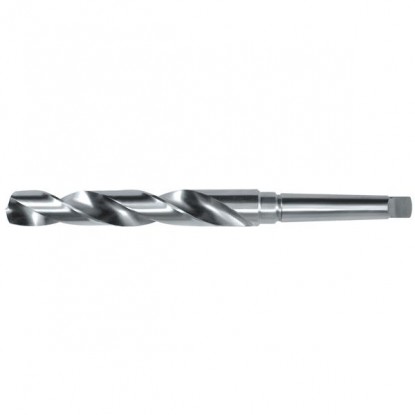
Twist drill with Morse taper shank
| TECHNICAL DATA | |
|---|---|
| Diameter | Ø50 NWKc HSS |
| Standard | DIN 345 |
| Drill type | NWKc — twist drill with taper shank |
| Material | HSS (high-speed steel) |
| Overall length l1 | 369 mm |
| Flute length l2 | 220 mm |
| Morse taper | MT4 |
| Point angle | 118° |
| Diameter tolerance | h8 |
| Cutting direction | Right-hand |
Product description and key benefits
The Ø50 mm metal drill bit with an MT4 Morse taper is a large-diameter tool whose mechanical loads require an MT4 taper with a diameter of 31.27 mm. At Ø50, torque in S355 steel is high enough to require a rigid machine base. The Ø50 Morse taper drill bit can operate at full speed only with abundant emulsion cooling and power spindle feed.
The Ø50 Morse taper drill is designed for drilling holes in machine housings, frames, and foundation plates. At MT4 diameters, the tool requires a machine with power feed — manual drilling will not provide uniform pressure. Holes within tolerance class H12, Ø50.000–Ø50.250 mm; tighter fits are achieved by boring.
Dimension table for all Morse tapers MT0–MT6
| Taper | Diameter D [mm] | Length [mm] |
|---|---|---|
| MT0 | 9.045 | 49.8 |
| MT1 | 12.065 | 53.5 |
| MT2 | 17.780 | 64.0 |
| MT3 | 23.825 | 80.5 |
| MT4 | 31.267 | 117.5 |
| MT5 | 44.399 | 149.5 |
| MT6 | 63.348 | 210.0 |
REDUCTION SLEEVES COMPATIBLE WITH THE Ø50 MM DRILL BIT:
| ✓ | MT4 → MT5 — for a spindle with an MT5 socket |
| ✓ | MT4 → MT3 — for a spindle with an MT3 socket |
| ✓ | MT4 drill drift — for removing the drill bit from the spindle |
Recommended machining conditions for a diameter of Ø50 mm
| ISO symbol | Workpiece material | Vc [m/min] | f [mm/rev] | n [rpm] | Vf [mm/min] |
|---|---|---|---|---|---|
| P Steel | Structural steel up to 900 N/mm² | 11÷20 | 0.25 | 70÷127 | 18÷32 |
| K Cast iron | Gray cast iron GG20–GG30 | 13÷16 | 0.25 | 83÷102 | 21÷26 |
| N Copper and Al alloys | Cu, CuZn, Al, and alloys | 25÷28 | 0.32÷0.40 | 159÷178 | 51÷71 |
At a diameter of 50 mm, the volume of chips generated per centimeter of depth is approximately 19.6 cm³. Use a 6–8% emulsion at a minimum flow rate of 6 l/min. Without pressurized cooling, limit the depth per pass to 75 mm.
Range of workpiece materials and application limitations
1) Clean the taper and spindle socket. 2) Check runout (maximum 0.03 mm). 3) Replace the drill if the taper is damaged or worn. 4) Do not stack reduction sleeves (e.g., MT4→MT3→MT5).
For diameters up to approximately 40 mm, drilling into solid material is possible after spot drilling with an NC 90° drill. Above 40 mm, a Ø20–25 mm pilot hole is recommended to reduce axial force by 40–50% and eliminate vibration from the chisel edge.
When drilling S355 steel with a Ø50 mm drill, the torque is approximately 125 Nm. This requires a drilling machine with a minimum power rating of 3.0 kW and power spindle feed.

Reference: 1186 In stock < 10 items
€45.32 brutto
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


