







Net price: €6.58
Description
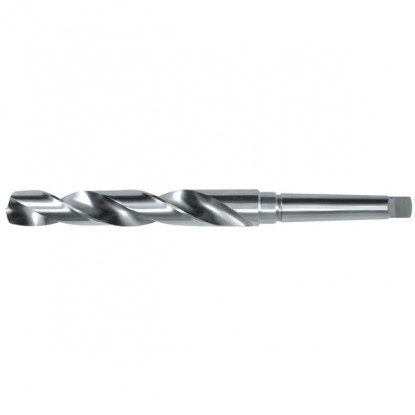
Twist drill with Morse taper shank
| TECHNICAL DATA | |
|---|---|
| Diameter | Ø11.25 NWKc HSS |
| Standard | DIN 345 |
| Drill type | NWKc — twist drill with taper shank |
| Material | HSS (high-speed steel) |
| Overall length l1 | 175 mm |
| Flute length l2 | 94 mm |
| Morse taper | MT1 |
| Point angle | 118° |
| Diameter tolerance | h8 |
| Cutting direction | Right-hand |
Product description and key benefits
The Ø11.25 mm twist drill with an MT1 taper shank solves the problem of tool slippage in a three-jaw chuck under full load. The Morse taper is self-holding — the higher the cutting torque, the more securely it seats in the spindle. The Ø11.25 Morse taper drill for a diameter of 11.25 mm ensures stability even during prolonged batch drilling at a single workstation.
The Ø11.25 mm Morse taper drill is used in metalworking shops for bolt and dowel holes in steel components. In batch production, it provides repeatable dimensional accuracy within tolerance class H12 (Ø11.250–Ø11.430 mm). H7 fits require finish reaming.
Dimension table for all Morse tapers MT0–MT6
| Taper | Diameter D [mm] | Length [mm] |
|---|---|---|
| MT0 | 9.045 | 49.8 |
| MT1 | 12.065 | 53.5 |
| MT2 | 17.780 | 64.0 |
| MT3 | 23.825 | 80.5 |
| MT4 | 31.267 | 117.5 |
| MT5 | 44.399 | 149.5 |
| MT6 | 63.348 | 210.0 |
REDUCTION SLEEVES COMPATIBLE WITH THE Ø11.25 MM DRILL BIT:
| ✓ | MT1 → MT2 — for a spindle with an MT2 socket |
| ✓ | MT1 → MT3 — for a spindle with an MT3 socket |
| ✓ | MT1 drill drift — for removing the drill bit from the spindle |
Recommended machining conditions for a diameter of Ø11.25 mm
| ISO symbol | Workpiece material | Vc [m/min] | f [mm/rev] | n [rpm] | Vf [mm/min] |
|---|---|---|---|---|---|
| P Steel | Structural steel up to 900 N/mm² | 11÷20 | 0.12 | 311÷566 | 37÷68 |
| K Cast iron | Gray cast iron GG20–GG30 | 13÷16 | 0.12 | 368÷453 | 44÷54 |
| N Copper and Al alloys | Cu, CuZn, Al, and alloys | 25÷28 | 0.16÷0.20 | 707÷792 | 113÷158 |
Sharpen the Ø11.25 mm drill bit on a tool grinder, maintaining the 118° point angle and cutting edge symmetry. Asymmetric sharpening enlarges the hole diameter and loads the spindle unevenly. Each sharpening reduces the flute length by approximately 1–2 mm.
Range of workpiece materials and application limitations
The maximum drilling depth is the flute length l2 = 94 mm minus the drill point length (approximately 3 mm). The effective usable depth is therefore approximately 91 mm.
In S235/S355 structural steels, spot drilling is not necessary — the 118° angle provides self-centering. Spot drilling with an NC 90° drill is recommended when drilling on milled surfaces, castings with machining allowance, or difficult-to-machine materials.
A cooling and lubricating emulsion at a concentration of 5–8% is recommended. For stainless steels, increase the concentration to 8–10%. Cast iron can be drilled dry with compressed air to remove chips.

Reference: 1179 In stock > 10 items
€19.42 brutto
Reference: 1184 In stock > 10 items
€14.57 brutto
Reference: 1185 In stock > 10 items
€27.51 brutto
Reference: 2586 In stock < 10 items
€11.33 brutto
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


