








Net price: €92.11
Description
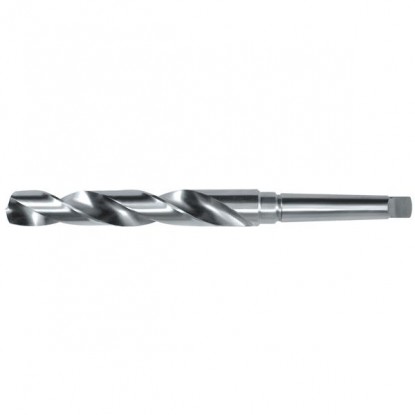
Twist drill with Morse taper shank
| TECHNICAL DATA | |
|---|---|
| Diameter | Ø41.5 NWKc HSS |
| Standard | DIN 345 |
| Drill type | NWKc — twist drill with taper shank |
| Material | HSS (high-speed steel) |
| Overall length l1 | 354 mm |
| Flute length l2 | 205 mm |
| Morse taper | MT4 |
| Point angle | 118° |
| Diameter tolerance | h8 |
| Cutting direction | Right-hand |
Product description and key benefits
The Ø41.5 mm NWKc metal drill bit is an industrial-grade tool — both in terms of cutting-edge material (HSS) and mounting method (MT4 Morse taper to DIN 345). At this diameter, every millimeter of drilling depth generates a substantial volume of chips that must be efficiently evacuated through the helical flutes. The Ø41.5 Morse taper drill bit requires emulsion cooling — dry drilling reduces cutting-edge life by as much as 70%.
The Ø41.5 Morse taper drill is designed for drilling holes in machine housings, frames, and foundation plates. At MT4 diameters, the tool requires a machine with power feed — manual drilling will not provide uniform pressure. Holes within tolerance class H12, Ø41.500–Ø41.750 mm; tighter fits are achieved by boring.
Dimension table for all Morse tapers MT0–MT6
| Taper | Diameter D [mm] | Length [mm] |
|---|---|---|
| MT0 | 9.045 | 49.8 |
| MT1 | 12.065 | 53.5 |
| MT2 | 17.780 | 64.0 |
| MT3 | 23.825 | 80.5 |
| MT4 | 31.267 | 117.5 |
| MT5 | 44.399 | 149.5 |
| MT6 | 63.348 | 210.0 |
REDUCTION SLEEVES COMPATIBLE WITH THE Ø41.5 MM DRILL BIT:
| ✓ | MT4 → MT5 — for a spindle with an MT5 socket |
| ✓ | MT4 → MT3 — for a spindle with an MT3 socket |
| ✓ | MT4 drill drift — for removing the drill bit from the spindle |
Recommended machining conditions for a diameter of Ø41.5 mm
| ISO symbol | Workpiece material | Vc [m/min] | f [mm/rev] | n [rpm] | Vf [mm/min] |
|---|---|---|---|---|---|
| P Steel | Structural steel up to 900 N/mm² | 11÷20 | 0.25 | 84÷153 | 21÷38 |
| K Cast iron | Gray cast iron GG20–GG30 | 13÷16 | 0.25 | 100÷123 | 25÷31 |
| N Copper and Al alloys | Cu, CuZn, Al, and alloys | 25÷28 | 0.32÷0.40 | 192÷215 | 61÷86 |
The Ø41.5 mm drill requires a drilling machine with at least 2.2 kW of power and power spindle feed. Stability is difficult to maintain with manual feed — uneven pressure leads to vibration and accelerated cutting edge wear. A box-column or radial drilling machine is recommended.
Range of workpiece materials and application limitations
When drilling S355 steel with a Ø41.5 mm drill, the torque is approximately 103 Nm. This requires a drilling machine with a minimum power rating of 2.5 kW and power spindle feed.
For a drilling machine with an MT5 spindle: MT4→MT5 sleeve. For a smaller MT3 spindle: MT4→MT3 sleeve (check that the operating load does not exceed the socket capacity). For removal: MT4 drill drift.
Depth greater than 3×D (124 mm): reduce feed by 30–50%, retract every 1×D, and use a 6–8% emulsion at a minimum flow rate of 6 l/min. Peck drilling prevents chips from jamming in the flutes.

Reference: 1186 In stock < 10 items
€45.32 brutto
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


