









Net price: €25.53
Description
| Technical data | |
|---|---|
| Thread size D1 | M15x1.25 |
| Thread Pitch P | 1.25 mm |
| Outside Diameter D2 | 38 mm |
| Thickness H1 | 10 mm |
| Number of Chip Holes | 5. |
| Required Shaft Diameter | 14.88 mm |

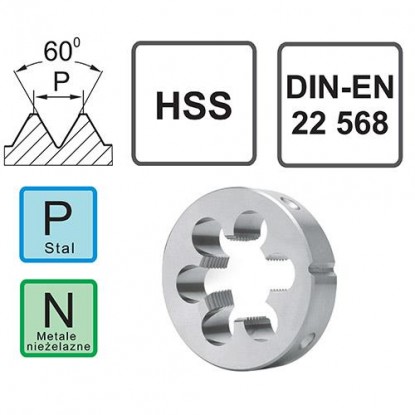
The M15x1.25 die is a professional round tool made of high-speed steel (HSS) with a hardness of 64 HRC, designed for cutting external metric fine threads with a diameter of 15 mm and a pitch of 1.25 mm. At this diameter, the fine thread provides increased vibration resistance and higher fatigue strength compared with the standard M15x1.75 thread. A design compliant with DIN 22 568 and a tolerance of 6g guarantee proper mating with 6H nuts in automotive and machinery industry applications and wherever connections resistant to dynamic loads are required. This tool is widely used in machine shops, maintenance departments, and the production of components exposed to vibration.
The M15x1.25 die is a tool selected by machine shops, maintenance departments, and manufacturing plants specializing in components exposed to dynamic loads and vibration. It is particularly recommended for cutting threads on rods, pins, and studs in the automotive industry, precision machinery, and industrial equipment. Use with threading lubricants is recommended to obtain a smooth surface and extend cutting edge life.
Prepare a rod (diameter 14.7-14.75 mm) with its end chamfered at 45°. Clamp the workpiece securely and keep the die strictly perpendicular, making two full turns forward, then reversing half a turn to remove chips. With a fine pitch of 1.25 mm, lubricate every 3 turns and check perpendicularity regularly to ensure quality.
For structural steels, use threading oils or standard machine oil applied before starting and replenished every few turns. Kerosene with added oil works well for aluminum, while machine oil is suitable for brass. A metric fine thread requires somewhat more intensive lubrication: apply lubricant every 3 turns instead of every 4 to keep the process running smoothly.
Causes include reversing too infrequently, insufficient lubrication, or an oversized rod. Stop the process immediately and unscrew the die completely by turning it in the opposite direction. Clean the flutes with a brush or compressed air and check the rod diameter with a micrometer. Resume with ample lubrication and more frequent reversing: for a metric fine thread, every 1.5 turn instead of every 2.

Reference: 0000006103 In stock > 10 items
€71.21 brutto
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


