








Description
| Technical data | |
|---|---|
| Thread size D1 | M16x1 |
| Thread Pitch P | 1 mm |
| Outside Diameter D2 | 45 mm |
| Thickness H1 | 14 mm |
| Number of Chip Holes | 5 |
| Required Shaft Diameter | 15.88 mm |

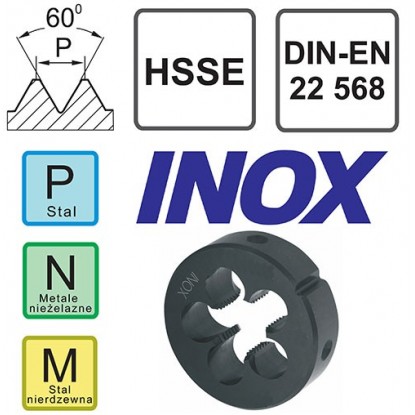
The M16x1 HSSE Inox die is a highly specialized round tool made of high-performance high-speed steel (HSSE), designed for cutting external metric ultra-fine threads with a diameter of 16 mm and a pitch of 1 mm in stainless steel. This unusual combination of a small diameter and an ultra-fine pitch in a difficult-to-machine material is used in the food, medical, and chemical industries, and wherever corrosion resistance is required together with maximum leak tightness and vibration resistance. The HSSE Inox designation indicates a version with alloying additions that increase resistance to high temperatures and wear during stainless steel machining. Compliance with DIN 22 568 and a tolerance of 6g ensure proper fit with 6H nuts.
The M16x1 HSSE Inox die is a tool for workshops serving the high-end medical, food, pharmaceutical, and chemical industries, and wherever corrosion resistance is required together with maximum leak tightness and vibration resistance. It is particularly recommended for cutting ultra-fine threads on stainless steel rods and pins in critical applications. The use of products specifically designed for stainless steel, such as Terebor Inox, is strongly recommended as essential, along with very frequent backing off and a slower working speed than with carbon steel, due to the combination of a difficult-to-machine material and an ultra-fine pitch.
Prepare a stainless steel rod (diameter 15.85-15.9 mm) with a chamfer. Clamp it as securely as possible – stainless steel work-hardens during machining, and an ultra-fine pitch intensifies this effect. Keep the die perpendicular, making one turn forward and half a turn back. With Inox steel and an ultra-fine pitch of 1 mm, back off very frequently – every 1 turn instead of every 2, and work more slowly than with carbon steel.
Top-quality specialized products for stainless steel, such as Terebor Inox Premium, are absolutely essential – standard oils are completely inadequate. Cutting ultra-fine threads in stainless steel generates extreme temperatures and causes the material to adhere to the tool without a suitable high-quality lubricant. Apply as generously as possible before starting and on every turn. Never skimp on lubrication when cutting ultra-fine threads in stainless steel – it is absolutely critical.
Stainless steel adheres to the tool and work-hardens severely, and an ultra-fine pitch intensifies all these problems. Causes: completely inadequate lubrication with Inox Premium or excessive working speed. Stop immediately, unscrew the die with extreme care (steel adheres very strongly at an ultra-fine pitch), and clean the flutes completely with a specialized cleaning product. Resume with the most generous possible application of a top-quality Inox lubricant, extremely frequent backing off (every 0.75-1 turn), and a much slower working speed – cutting ultra-fine threads in stainless steel requires maximum patience and the highest level of operator skill.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


