





- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot
navigate_next
navigate_next
navigate_next

Machine Tap M15X1.25 DIN 374 B HSSE
Narex Zdanice spol. s r.o. Narex Zdanice spol. s r.o.
0000006103
Thread size: M15x1,2561 sizes of this tap
M5x0,5M10x1M10x1,25M11x0,75M12x1M12x1,25M12x1,5M14x1M14x1,25M14x1,5M15x1M15x1,25M15x1,5M16x1M16x1,5M17x1M18x1M18x1,5M18x2M20x0,75M20x1M20x1,25M20x1,5M20x2M22x1,5M22x2M24x1M24x1,5M24x2M25x1M25x1,5M25x2M26x1,5M27x1,5M28x1,5M30x1,5M30x2M30x3M32x1M32x1,5M32x2M33x1,5M33x2M35x1,5M36x1,5M36x2M36x3M38x1,5M39x1,5M39x2M40x1,5M42x1,5M42x2M42x3M48x1,5M50x2M52x2M56x3M60x3M64x3M64x4
€71.21 tax inc.
Net price: €57.89
Instant Shipping
W magazynie: 10-100 szt.
Description
Material HSSE
Thread size M15x1.25
ChamferB (3.5–5.5) threads
Standard DIN 374
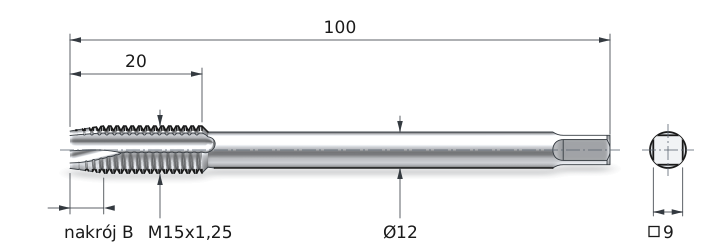
Technical data for the M15x1.25 machine tap
| Technical Data | |
|---|---|
| Nominal Diameter d1 | M15x1.25 |
| Thread Pitch P | 1.25 mm |
| Overall Length l1 | 100 mm |
| Flute Length l2 | 20 mm |
| Shank Diameter d2 | 12 mm |
| Square Drive Size a | 9 mm |
| Tap Drill Diameter | 13.75 mm |
| Chamfer | B (3.5÷5.5) P |
| Thread tolerance | 6H |
How the type B through-hole chamfer pushes chips down the hole
Chips exit at the bottom instead of returning through the thread
The form B chamfer for through holes has a chip breaker at the tip of the tap – an angled cut in the cutting edges. The chip breaker directs the chip down the hole, ahead of the tap tip. The chip curls into a coil, breaks into short pieces and exits the hole on the other side of the workpiece. The threads already cut remain clean because the chip does not pass through them on its way up. The M15x1.25 tap has a reduced shank according to DIN 374: diameter 12 mm, square size 9 mm.
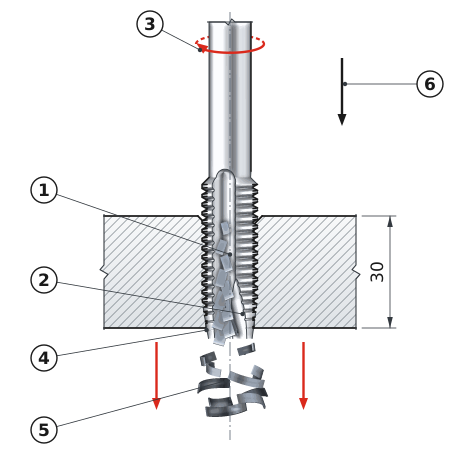
1
Straight flute – chips do not enter it; the flute carries lubricant to the cutting edges.
2
The chip breaker at the tip of the tap directs chips down the hole.
3
The tap rotates clockwise to cut a right-hand thread.
4
B chamfer: 3.5–5.5 incomplete threads on the entry taper.
5
The chips break into segments: individual pieces at the top of the hole, with progressively more farther down. They fall out below the workpiece.
6
Feed 1.25 mm/rev, equal to the pitch of the M15x1.25 thread.
M15x1.25 fine-thread machine tap – HSSE for precision engineering
The M15x1.25 fine-thread machine tap from the HSSE series is designed to produce internal threads with a nonstandard diameter of 15 mm and an intermediate pitch of 1.25 mm for precision applications. High-speed steel construction with 5% cobalt provides a hardness of 65-67 HRC and high heat resistance in the cutting zone up to 650°C, essential for machining materials. The M15 size with a 1.25 mm pitch is used in specialized precision engineering applications where standard sizes do not meet requirements. The tool is intended for professional toolrooms and prototype workshops handling custom orders.
Key advantages of the M15x1.25 metric fine thread machine tap
- Nonstandard M15 size fills the gap between the popular M14 and M16 sizes in structures with specific dimensional or strength requirements in the mechanical design
- Fine thread with a 1.25 mm pitch offers a balance between the adjustment precision of the M15x1 thread and assembly speed while maintaining good joint strength
- HSSE steel with 5% cobalt guarantees a hardness of 65-67 HRC and heat resistance up to 650°C, extending cutting edge life under intensive use
- The 6H tolerance in accordance with DIN 374 ensures thread accuracy and full interchangeability with fasteners used in precision engineering and prototype workshops
- Compatibility with ER20 and ER25 holders and tapping chucks with axial compensation for CNC machining centers with synchronous tapping capability
- The recommended tap drill diameter of 13.8 mm for the M15x1.25 metric fine thread ensures optimal thread engagement with minimal tool load
The M15x1.25 machine tap is used in precision engineering, prototype workshops, and special applications requiring a nonstandard diameter with an intermediate fine pitch. Form B with straight flutes directs chips forward when tapping through holes. Cooling with an oil emulsion at a concentration of 6-8% is recommended to maintain optimal tool life.
| Material | Cutting speed Vc [m/min] | Spindle speed n [rpm] | Feed f [mm/min] |
|---|---|---|---|
| PSteel | 5-20 | 106-424 | 132-530 |
| MStainless steel | 5-10 | 106-212 | 132-265 |
| KCast iron | 5-15 | 106-318 | 132-398 |
| NAluminum | 10-25 | 212-531 | 265-664 |
Thread preparation M15x1.25 in a through hole
1 Spot drilling
NC spotting drill 90°
2 Drilling
Ø 13.75 mm
3 Tapping
M15x1.25
✓ Done!
Tolerance 6H
Standard: DIN 374 | Chamfer: B (straight) | Application: through holes
Tolerance 6H — metric thread tolerance classes
| Class | Accuracy | Application | Status |
|---|---|---|---|
| 4H / 4g | High | Precision connections, hydraulics | — |
| 6H / 6g | Standard | Machine building, general-purpose | SELECTED |
| 7H / 8g | Low | Large clearance, easy assembly | — |
6H = internal thread (nut, hole) | 6g = external thread (screw)
Frequently asked questions
The M15x1.25 thread is used in precision engineering, prototype workshops, and special applications requiring a nonstandard diameter with an intermediate fine pitch.
The recommended tap drill diameter for the M15x1.25 metric fine thread is 13.8 mm. Precise hole machining ensures full thread engagement.
M15x1.25 is a special thread, and fasteners must be specially ordered from precision component suppliers. Checking availability in advance is recommended.
Product accessories


Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Machine Tap M15X1.25 DIN 374 B HSSE Podgląd zdjęć produktu
01 / 01

Powiększenie 100%
Użyj strzałek, aby zmieniać zdjęcia. Powiększaj przyciskami albo gestem szczypania. Zamknij galerię klawiszem Escape.
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.