








Net price: €8.95
Description
| Technical data | |
|---|---|
| Thread size D1 | M12x0.75 |
| Thread Pitch P | 0.75 mm |
| Outside Diameter D2 | 30 mm |
| Thickness H1 | 10 mm |
| Required Shaft Diameter | 11.93 mm |

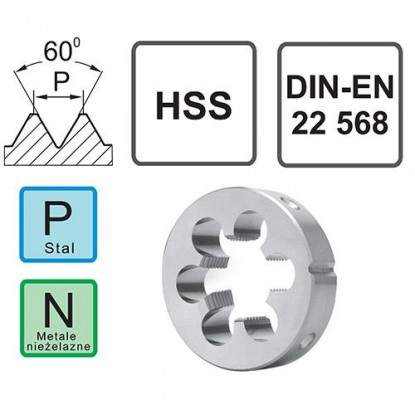
The M12x0.75 die is a specialized round tool made of high-speed steel (HSS) with a hardness of 64 HRC, designed to cut external metric threads with a small diameter of 12 mm and an ultrafine pitch of 0.75 mm. A thread with this pitch requires high manufacturing precision and is used in precision engineering, instrumentation, and equipment requiring maximum sealing performance and vibration resistance at small dimensions. Compliance with DIN 22 568 and a tolerance class of 6g ensure a proper fit with 6H nuts in applications requiring high accuracy. This tool is intended for specialized precision workshops manufacturing small-diameter components with elevated requirements.
The M12x0.75 die is a tool for specialized workshops involved in precision engineering and the manufacture of instrumentation, inspection and measuring equipment, and components requiring the highest sealing performance at small dimensions. It is ideally suited for cutting ultrafine threads on small spindles, pins, and components requiring maximum vibration resistance. Due to this unusual combination, threading requires highly qualified operators, very secure clamping, and intensive lubrication with lubricants dedicated to small-diameter ultrafine threads.
Prepare the rod (diameter 11.9-11.95 mm) with a carefully machined chamfer. Clamp the workpiece very securely, preferably under a magnifier for inspection of the small dimensions. Position the die perfectly perpendicular and make one full turn forward, followed by half a turn back. With small dimensions and an ultrafine pitch of 0.75 mm, check perpendicularity very frequently and lubricate every turn.
An ultrafine pitch requires intensive lubrication regardless of diameter. Use precision threading oils applied generously before every turn. A diameter of 12 mm and a pitch of 0.75 mm generate a very large number of chips – lubricant must be present at all times, but with a small diameter, avoid excess that obstructs visual inspection.
An ultrafine pitch at a small diameter is sensitive to overload. At the slightest increase in resistance, immediately back off the die gently and clean the flutes very thoroughly. Verify the rod diameter with a micrometer (tolerances are very tight with an ultrafine pitch). Resume with the highest possible reversal frequency (every 0.75-1 turns) and fresh, highest-quality lubricant for small precision components.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


