






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot

Hand Tap M17X2 ISO 529/2 6H HSS
13165
Thread size: M17x2172 sizes of this tap
M1x0,2M1,2x0,2M1,4x0,2M1,6x0,2M1,7x0,2M1,8x0,2M2x0,25M2,2x0,25M2,2x0,35M2,3x0,25M2,3x0,35M2,5x0,35M3x0,35M3,5x0,35M4x0,5M4,5x0,5M5x0,5M5,5x0,5M6x0,5M6x0,75M7x0,5M7x0,75M8x0,5M8x0,75M8x1M9x0,5M9x0,75M9x1M10x0,5M10x0,75M10x1M10x1,25M11x0,75M11x1M11x1,25M12x0,5M12x0,75M12x1M12x1,25M12x1,5M13x1M13x1,25M14x0,75M14x1M14x1,25M14x1,5M15x1M15x1,5M16x0,75M16x1M16x1,25M16x1,5M17x1M17x1,5M17x2M18x0,75M18x1M18x1,25M18x1,5M18x2M19x1M19x1,5M20x0,75M20x1M20x1,25M20x1,5M20x2M21x1,5M22x1M22x1,25M22x1,5M22x1,75M22x2M24x1M24x1,5M24x2M25x1M25x1,5M25x2M26x1M26x1,25M26x1,5M26x2M27x1M27x1,5M27x2M28x1M28x1,5M28x2M30x1M30x1,5M30x2M30x2,5M30x3M32x1,5M32x2M32x3M33x1,5M33x2M33x3M34x1,5M34x2M35x1,5M36x1M36x1,5M36x2M36x3M38x1,5M38x2M38x3M39x1M39x1,5M39x2M39x3M40x1,5M40x2M40x3M42x1,5M42x2M42x3M42x4M45x1,5M45x2M45x3M45x4M46x1,5M46x2M48x1,5M48x2M48x3M48x4M50x1,5M50x2M50x3M52x1M52x1,5M52x2M52x3M52x4M55x2M55x3M56x1,5M56x2M56x3M56x4M58x2M58x4M60x1,5M60x2M60x3M62x1,5M62x2M62x3M62x4M64z1,5M64x2M65x2M65x4M68x1,5M68x2M68x3M68x4M70x1,5M70x2M72x1,5M72x4M75x1,5M75x2M76x1,5M80x1,5M85x2M90x2
€15.86 tax inc.
Net price: €12.89
Description
Technical data for the M17x2 hand tap
| Technical data | |
|---|---|
| Nominal diameter d1 mm | M17 |
| Thread pitch P mm | 2 mm |
| Overall length l1 | 102 mm |
| Flute length l2 | 32 mm |
| Shank diameter d2 | 12.5 mm |
| Square drive size a | 10 mm |
| Tap drill diameter | 15 mm |
| Thread angle G | 60° |
| Tap tolerance | ISO2 6H |

Roughing tap and finishing tap – how much material each removes
Division of work in the 1–2 set
The M17x2 thread is cut into the wall of a hole with a diameter of 15 mm. The thread groove extends 1 mm into the wall. A single tap would have to cut the entire groove at once, requiring substantial hand torque and risking breakage. The set divides this work into two passes.
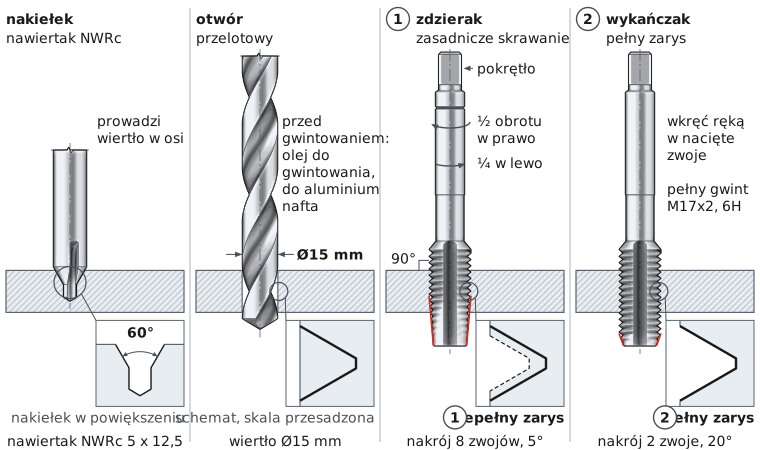
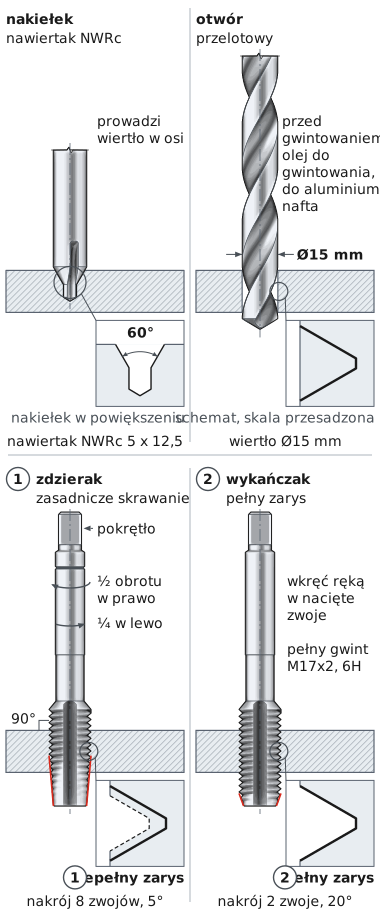
The drawing shows the entire set in operation. Both taps have the same shank and the same length. They differ in their chamfer, the tapered tip: No. 1 has a chamfer spanning 8 threads, while No. 2 spans only 2 threads. The detail windows at the hole wall show how the thread groove deepens after each tap.
| Tap | Chamfer | Chamfer angle | Material removed | How it works in the hole |
|---|---|---|---|---|
| No. 1 – roughing tap | long, 8 threads | 5° | the main portion of the groove | enters smoothly and establishes thread alignment |
| No. 2 – finishing tap | short, 2 threads | 20° | the remainder, to the full profile | follows the cut threads and produces the full 6H profile |
How to distinguish the taps in the set
The chamfer on No. 1 is 4 times as long as the chamfer on No. 2 — the difference is immediately visible when you place them side by side. No. 1 has an incomplete thread profile; only No. 2 has the full profile. The number is also indicated on the shank: No. 1 has one ring, No. 2 has none. Keep the set together and always start with the roughing tap.
How to tap an M17x2 hole – sequence 1, 2
Hand tapping step by step
Thread M17x2 in four steps
ØDrilling
Drill bit 15 mm
1Roughing tap
Chamfer 8 threads
2Finishing tap
Chamfer 2 threads
✓Finished thread
Tolerance 6H
Turning sequence: half a turn clockwise, a quarter turn counterclockwise | Between taps: remove chips from the hole
Start with the hole. The drill diameter is easy to calculate: thread diameter 17 mm minus pitch 2 mm gives 15 mm. An undersized hole is a common cause of a tap twisting off in the workpiece.
Through hole or blind hole – how deep to drill
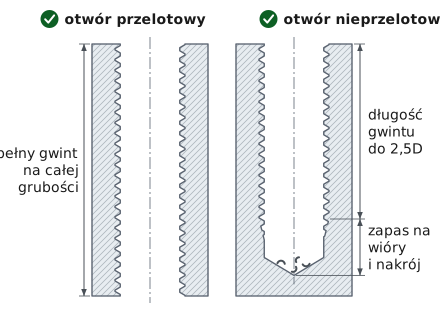
The set taps both types of holes. In a through hole, the thread extends through the full material thickness. In a blind hole, cut the thread to 42.5 mm, or 2.5 times the thread diameter (2.5 x 17 mm, shown as 2.5D in the drawing). Drill the hole deeper than the thread. The finishing tap has a chamfer spanning 2 threads, so approx. 2 incomplete threads remain near the bottom. The extra depth below the thread accommodates them along with the chips.
No. 1 – the roughing tap establishes thread alignment
Fit the roughing tap in the tap wrench and position it perpendicular to the surface. Check the angle from two sides, for example with a square. Turn half a turn clockwise, then a quarter turn counterclockwise. Reversing breaks the chip into short pieces – a slight crunch is normal. The first threads determine whether the thread will be straight.
No. 2 – the finishing tap produces the full profile
Back out the roughing tap and remove chips from the hole. Screw the finishing tap into the cut threads by hand – it should engage them on its own. Continue turning at the same rhythm as with the roughing tap. The finishing tap removes the remaining material and cuts the groove to the full profile within tolerance 6H. When it screws in smoothly all the way, the thread is complete – check it with an M17x2 screw.
M17x2 fine-thread hand taps
Hand Tap M17x2 ISO 529/2 6H HSS is designed to cut precise metric threads with a pitch of two millimeters in structural steels, nonferrous alloys and harder plastics. Its careful construction and stable profile geometry enable a clean, repeatable thread profile in one-off and small-batch machining.
Technical parameters: nominal diameter seventeen millimeters, pitch two millimeters, sixty° profile conforming to ISO 68-1, internal thread tolerance class 6H per ISO 965, right-hand thread. The ground high-speed steel (HSS) version guarantees long cutting edge life and reduces the risk of microchipping. The two-tap design conforming to ISO 529/2 — starter (I) and finisher (II) — equalizes torque and helps maintain axial alignment. In workshop practice, the tapping process is improved by M17x2 Hand Tap Set, which helps maintain the correct working sequence and ensures consistent results across successive passes.
- Optimal profile formation — the two-stage operation limits torsional vibration and reduces the risk of jamming.
- Long cutting edge life — precision-ground high-speed steel (HSS) provides longer service life and maintains a sharp cutting edge.
- Class 6H accuracy — guarantees an ideal fit and maintains profile geometry throughout the full depth of the hole.
- Process control and organization — a properly matched tap sequence in the Hand Tap Set M17x2 enables consistent machining and easy dimensional inspection.
Compliance with ISO 529/2, ISO 68-1 and ISO 965 ensures full compatibility with inspection equipment and predictable results in production cycles. Combining precision design with the durability of HSS, Hand Tap M17x2 ISO 529/2 6H HSS provides a reliable solution for assembly and workshop operations with high accuracy requirements.
Stages of cutting an M17x2 thread with a 2-piece set: roughing tap and finishing tap

Frequently asked questions
The set consists of two taps — a roughing tap and a finishing tap, which guarantee a fully formed thread when used in sequence.
The HSS tool works well in low-carbon steel, aluminum, brass, and other materials with good machinability.
High-speed steel (HSS) provides high durability, abrasion resistance, and stable operation even under demanding conditions.
Product accessories


Tapered countersink 20.5/90 DIN 335 C HSS
Reference: 11248 In stock > 10 items
€14.47
€17.80 brutto

Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you


This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.