






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot

Adjustable reamer 18.25-19.75 NRZe
15027
€25.89 tax inc.
Net price: €21.05
Description
Adjustable reamer 18.25-19.75 mm – hand reamer for 19 mm
Technical data – HSS blades, shank with square drive for a tap wrench
| Technical data | |
|---|---|
| Adjustment range | 18.25–19.75 mm |
| Designation | NRZe to PN |
| Blades | HSS, in inclined grooves |
| Diameter adjustment | two nuts |
| Shank diameter | 11.4 mm |
| Shank square | 9 mm |
| Overall length | 182 mm |
| Blade length | 60 mm |
| Drive | tap wrench |
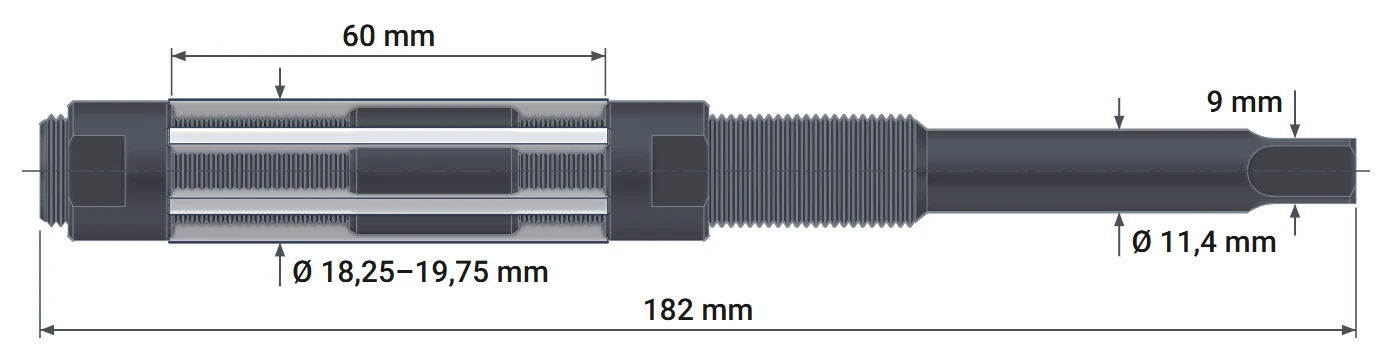
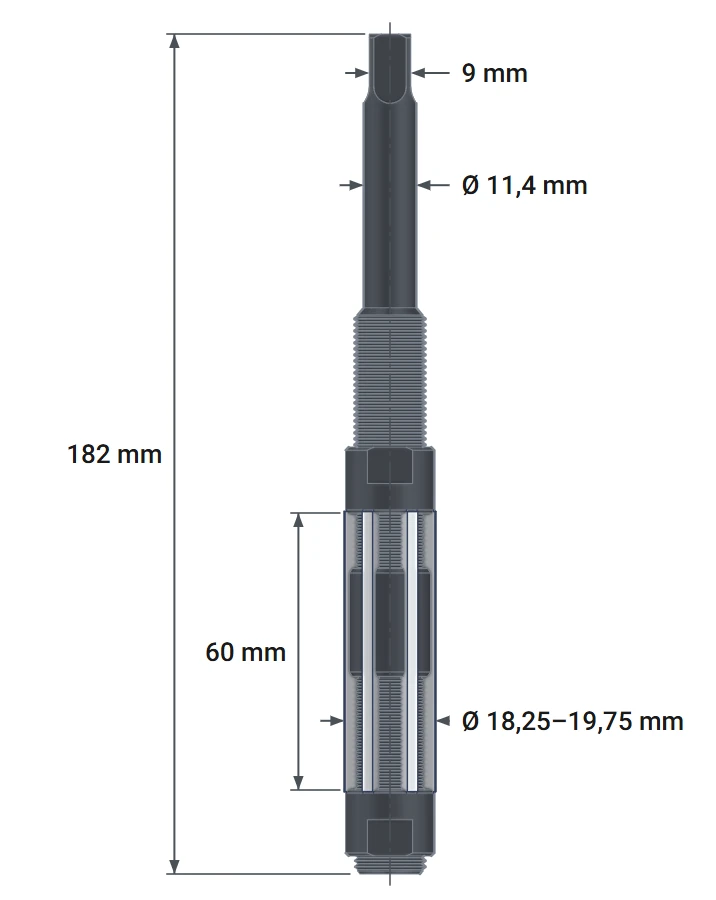
Adjustable reamer 18.25-19.75 mm The NRZe finishes holes from 18.25 to 19.75 mm, including the full 19 mm size. Set the diameter with two nuts that move the high-speed steel (HSS) blades along inclined grooves in the body. The shank square measures 9 mm, the same as on M14 and M16 hand taps. For a 19 mm hole, use a 18.75 mm drill bit. Operate it by hand with a tap wrench fitted over the square on the shank.
Manufacturers design adjustable blade reamers for repair and assembly work. They are useful wherever a hole needs to be fitted to the part at hand. The diameter is then set to the size of the part, rather than to the standard size series of fixed reamers.
Which size to choose: 18.25-19.75 mm and adjacent sizes
Below 18.25 mm, use the 16.5-18.25 mm reamer; from 19.75 mm, use the 19.75-21.5 mm reamer. The ranges meet but do not overlap. Holes of 18.25 and 19.75 mm therefore require two adjacent reamer sizes. The 19.75-21.5 mm reamer has a 9.6 mm square and uses the same No. 3 tap wrench.
How diameter adjustment works – blades and two nuts
NRZe reamer construction and measuring the diameter setting
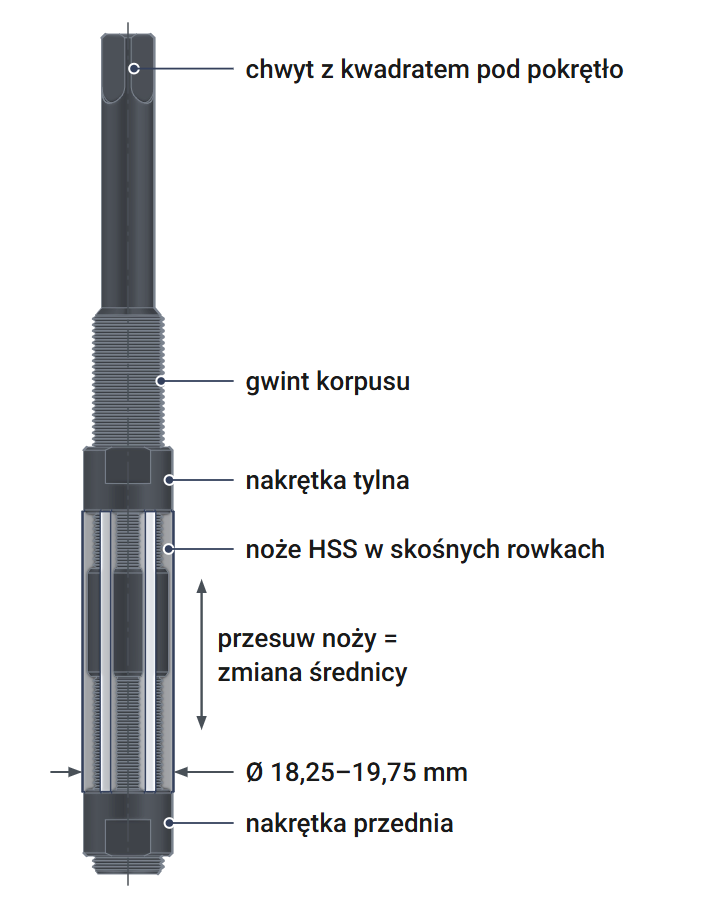
The body has inclined grooves around its circumference, each holding an HSS blade. Two nuts, front and rear, retain the blades at both ends. Moving the blades along the grooves moves their cutting edges away from or toward the axis. This changes the cutting diameter over a range of 1.5 mm, from 18.25 to 19.75 mm. This is why the tool is also called an adjustable reamer.
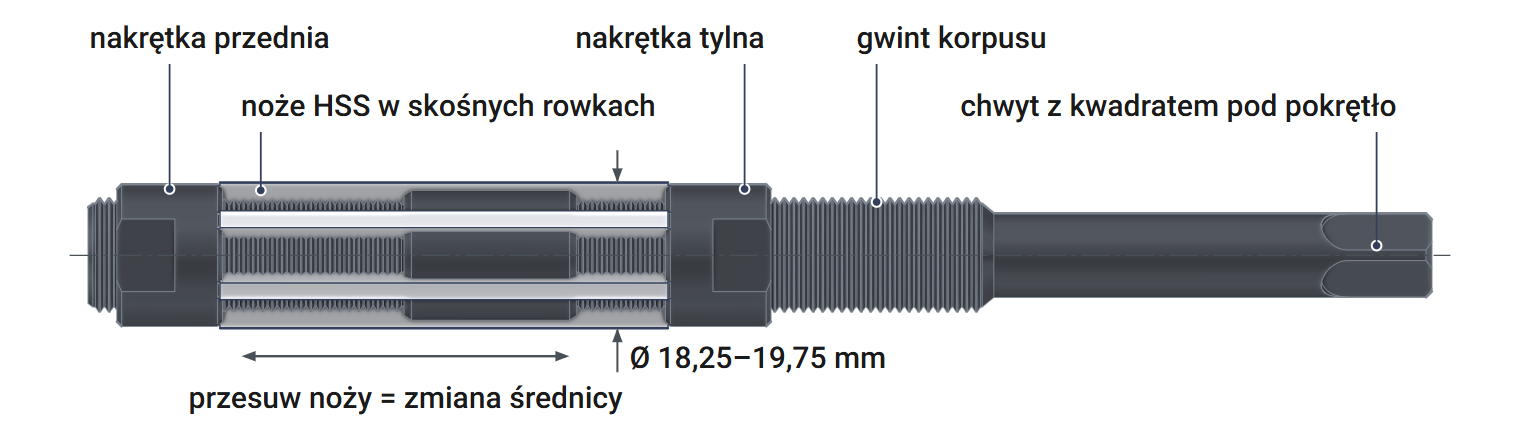
Adjustment in three steps
First, loosen one nut. Then tighten the other — the blades will move to the new diameter. Finally, lock the blades by tightening the first nut. The rear nut, on the shank side, provides the main clamping force; the front nut is only snugged up. Tighten carefully. Excessive force bows the blades outward and causes the reamer to catch in the hole.
How to measure the set diameter
With an even number of blades, measure the diameter across two opposite blades using a micrometer. With an odd number, a groove lies opposite each blade, so the micrometer will read too low. In this case, use a setting ring or a hole of known diameter. Insert the reamer and expand the blades until they contact the hole wall.
How to ream step by step – tap wrench and clockwise rotation
Guidelines for using an adjustable hand reamer
Insert the reamer into the hole and apply light pressure so the blades engage the wall immediately. The tap wrench must fit the square closely to ensure smooth rotation without jerking. Align the reamer axis with the hole axis. For a longer hole, check the alignment with a square.
Hand reaming in six steps
1
Drill a hole
Use a 18.75 mm drill bit for a 19.0 mm hole. Remove the 0.25 mm allowance in two passes.
2
Set the diameter
Loosen one nut, move the blades with the other, then lock the first nut.
3
Fit the tap wrench
Fit it to the square and align the reamer with the hole axis.
4
Turn clockwise
Turn smoothly with light, even pressure.
5
Withdraw the reamer
Keep turning clockwise, including as the blades leave the hole.
✓
Check the hole
Too tight? Set a larger diameter and make a second pass.
Guidelines based on adjustable reamer manufacturers' instructions.
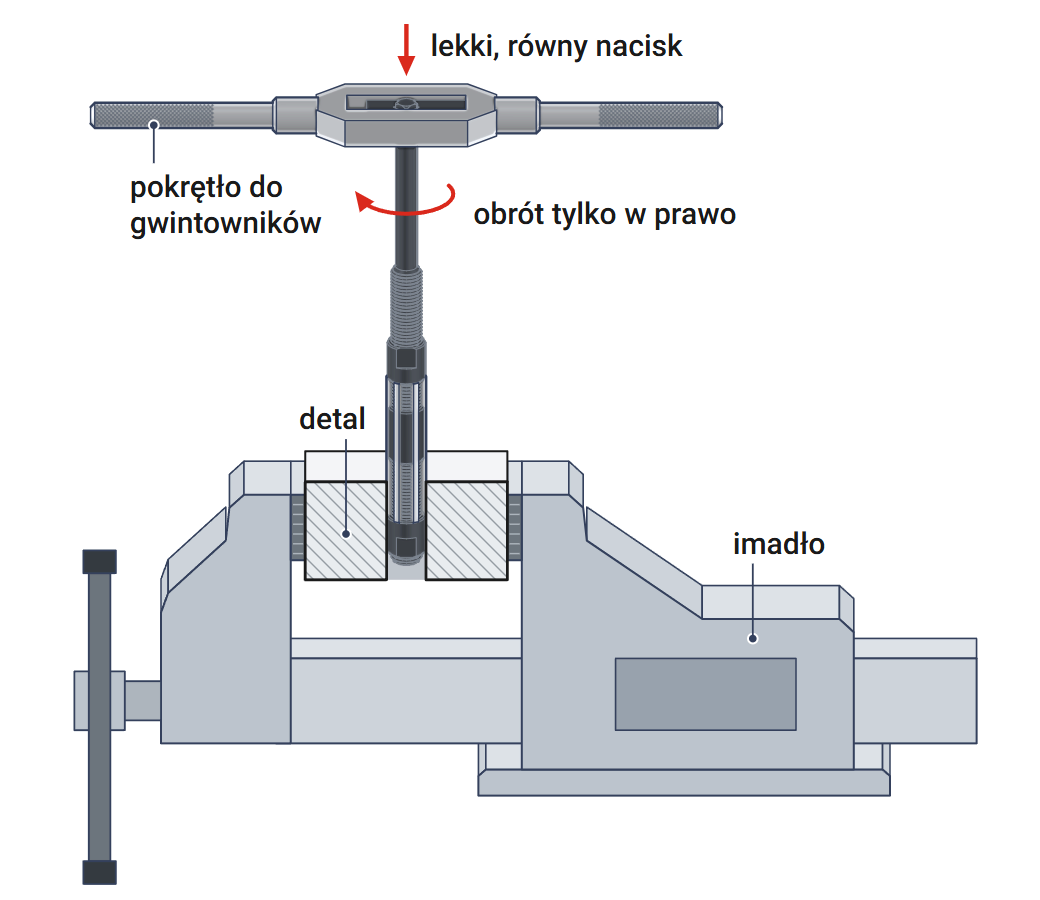
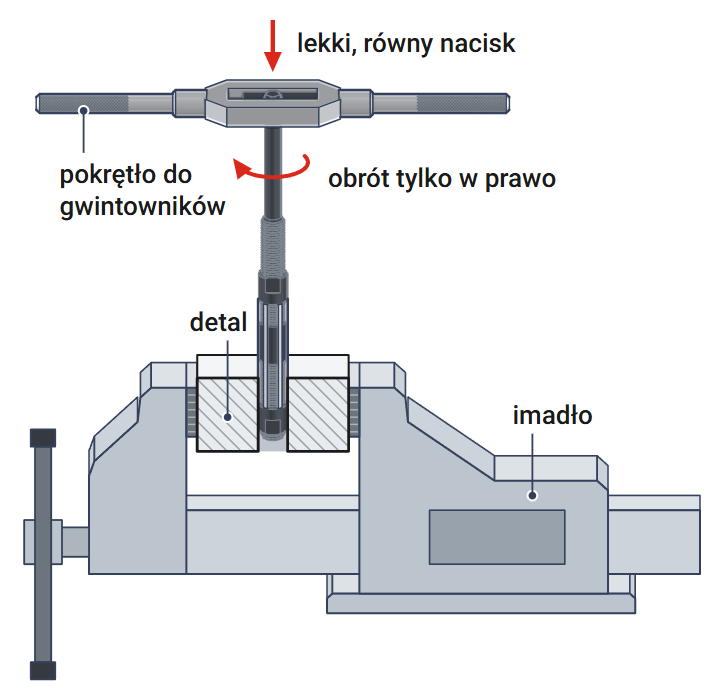
As the blades emerge from the far end of the hole, resistance drops suddenly. Reduce pressure at this point, but maintain the same turning speed. Otherwise, the reamer will jump through the end of the hole and leave it uneven.
▲
Never turn counterclockwise
Turning counterclockwise in the hole dulls the blades and may chip them. It can also loosen a nut and change the setting. Turn clockwise when withdrawing the tool as well; otherwise, you will scratch the hole wall.
How much material one pass removes
Reaming allowance and drill bit selection
This tool finishes a hole rather than drilling it. It removes a thin layer: from 0.05 to 0.15 mm on the diameter in one pass. A smaller allowance produces a smoother wall. Too little allowance is detrimental, as the blades rub against the wall instead of cutting and become dull faster.
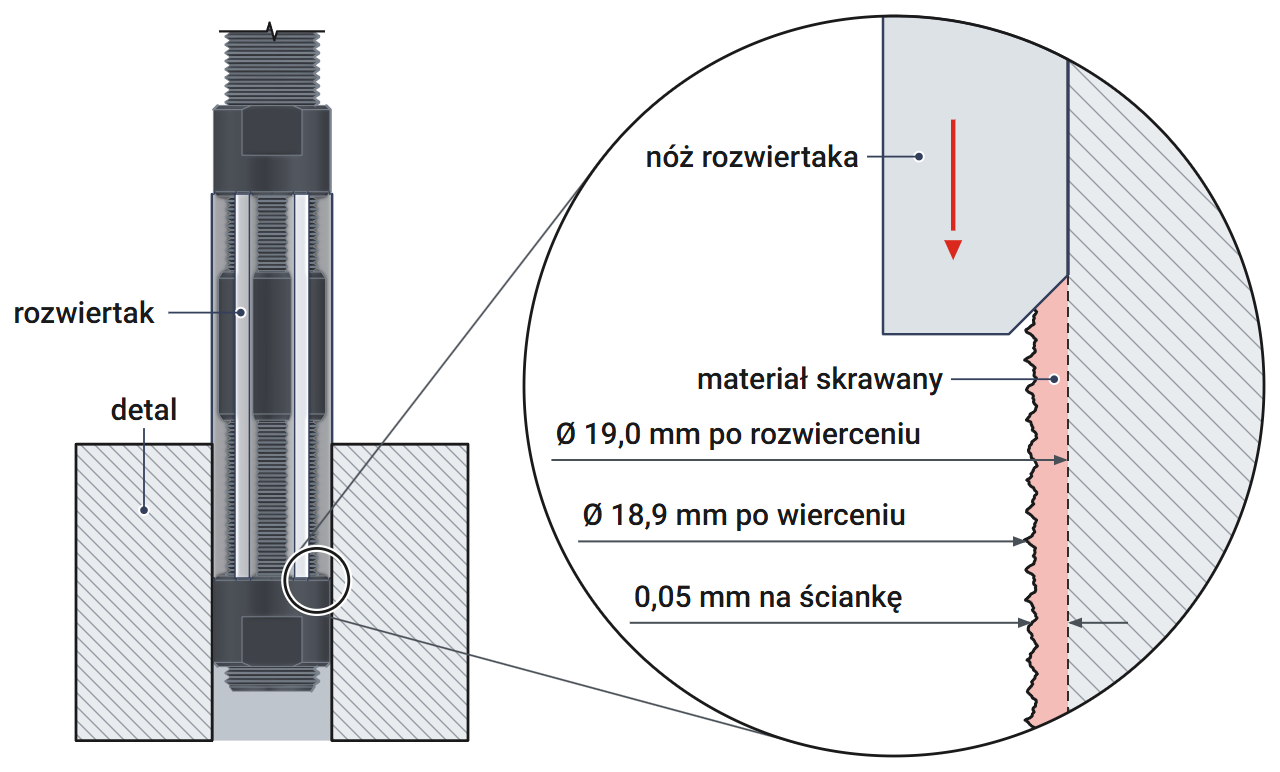
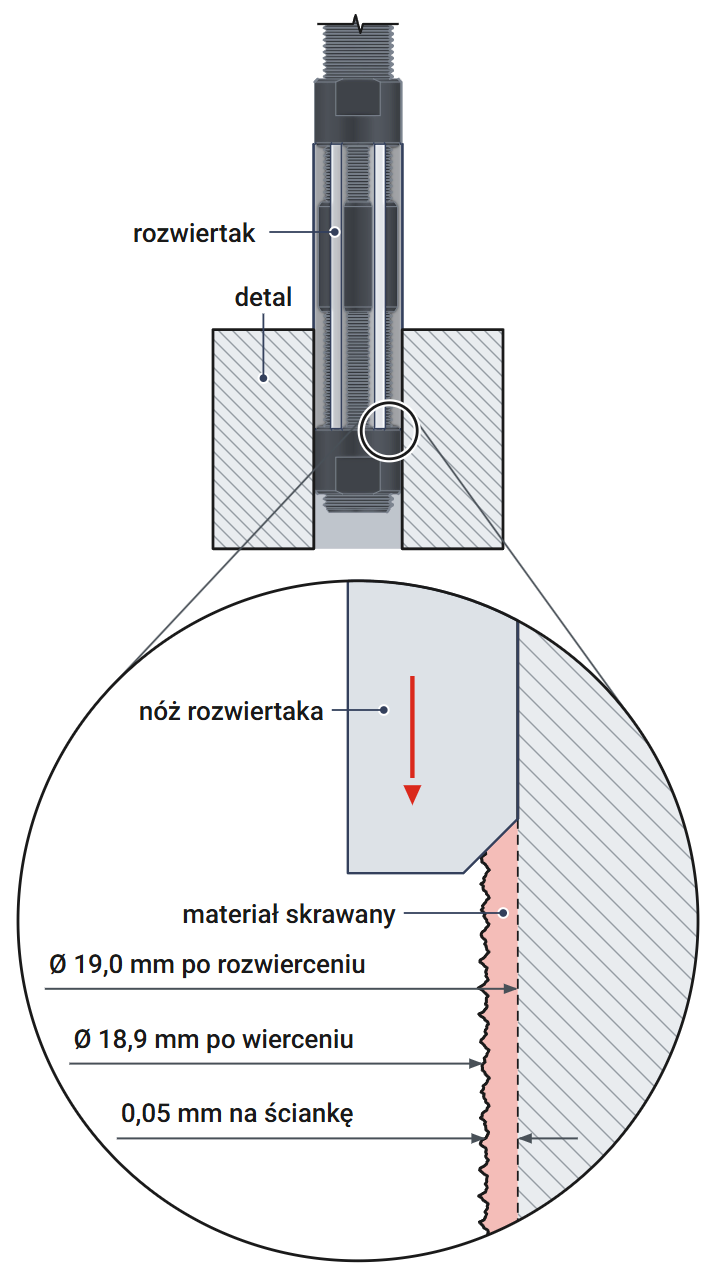
Calculation: 19 mm hole after drilling with a 18.75 mm drill bit
Diametral allowance = finished hole diameter 19.0 mm − drill bit diameter 18.75 mm = 0.25 mm. This exceeds the 0.15 mm that the blades remove in one pass. Set the first pass to 18.9 mm – it will remove 0.15 mm. Set the second to 19.0 mm – it will remove the remaining 0.1 mm.
| Finished hole [mm] | Drill bit [mm] | Diametral allowance [mm] | Layer thickness at the wall [mm] | Passes |
|---|---|---|---|---|
| 18.5 | 18.25 | 0.25 | 0.125 | 2: set to 18.4, then 18.5 |
| 19.0 | 18.75 | 0.25 | 0.125 | 2: set to 18.9, then 19.0 |
| 19.5 | 19.25 | 0.25 | 0.125 | 2: set to 19.4, then 19.5 |
| 19.75 | 19.5 | 0.25 | 0.125 | 2: set to 19.65, then 19.75 |
Drill bits in this range are available in 0.25 mm increments, with a straight shank or Morse taper MT2. Each leaves a 0.25 mm allowance. Remove it in two passes: 0.15 mm and 0.1 mm.
Tap wrench and lubrication – what to prepare
Tap wrench for a 9 mm square and oil suited to the material
Tap wrench No. 3
The shank square measures 9 mm, the same as M14 and M16 hand taps with a 9 mm square. The same tap wrench therefore fits. Choose an adjustable tap wrench to DIN 1814, size No. 3. It accepts squares from 4.9 to 12 mm and fits M5–M20 taps. The smaller No. 2 tap wrench has an upper limit of 9 mm, exactly at the size of the reamer square.
With oil or dry
| Workpiece material | Lubrication |
|---|---|
| Steel and cast steel | cutting oil or emulsion |
| Aluminum alloys | cutting oil or emulsion |
| Gray and malleable cast iron | dry |
| Bronze and brass | dry |
Remove chips from the reamer after use. Before adjusting the blades, also clean the body grooves so the blades move evenly.
Adjustable reamer 18.25-19.75 mm The NRZe has a 9 mm square, just like M14 and M16 hand taps. The reamer is 182 mm long, and its blades are 60 mm long. Use the same No. 3 tap wrench to drive them. Prepare a 19 mm hole with a 18.75 mm drill bit and ream twice: to 18.9 and 19.0 mm. Always turn clockwise.
Questions about drill bits, size selection, and operation
Frequently asked questions about hand reaming
With a 18.75 mm drill bit. Remove the 0.25 mm allowance in two passes: to 18.9 and 19.0 mm. The first removes 0.15 mm, and the second removes 0.1 mm.
Yes. M14 and M16 hand taps have a 9 mm square, just like this reamer. Both fit a No. 3 tap wrench, designed for squares from 4.9 to 12 mm.
Clockwise, just as when reaming. Clockwise rotation protects the blades and the hole wall. It also keeps the nuts in place, so the setting does not change.
Yes, at very low speed and with plenty of oil. At high speed, the hole may end up larger than the setting. Using a tap wrench provides the best control.
Product accessories


HSSE 18.5 cobalt metal drill bit DIN 338
Reference: 13299 In stock > 10 items
€18.42
€22.66 brutto
HSSE 19.5 cobalt metal drill bit DIN 338
Reference: 13301 In stock > 10 items
€19.74
€24.28 brutto

Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you




This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.