








Net price: €42.11
Description
Type DWCb · DIN 375 · high-speed steel (HSS) · Artykuly Techniczne brand
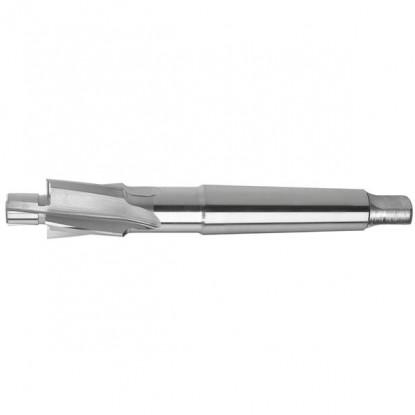
Manufactured to DIN 375 32×26 mm counterbore with pilot (type DWCb, Morse taper shank MT 3) is used to counterbore holes Ø26 mm. The rigid taper shank performs well at large cutting diameters, where a straight shank could slip in the chuck. The counterbore made of steel HSS machines steel, aluminum, copper, and brass. A Polish product from the brand Artykuly Techniczne.
| Technical data | |
|---|---|
| Counterbore diameter D | 32 mm |
| Pilot diameter d₁ | 26 mm |
| Morse taper shank | MT 3 |
| Flute length l | 35 mm |
| Pilot length l₁ | 16 mm |
| Overall length L | 310 mm |
| Material | HSS |
| Standard | DIN 375 DWCb |
| Brand | Artykuly Techniczne |
| Country of manufacture | Poland |
Applications and materials for the counterbore with Morse taper MT 3 shank
Typical applications:
| ✓ | Flat Ø32 mm seats in holes with a diameter of 26 mm |
| ✓ | Machining large steel parts, housings, and welded structures |
| ✓ | Spotfacing around the hole |
| ✓ | Use on pillar and radial drilling machines with Morse taper sockets and on milling machines |
Workpiece materials
Pilot Ø26 mm guides the tool coaxially in the hole, while the taper shank Morse taper MT 3 transmits high torque without slipping — at a cutting diameter of Ø32 mm, this is essential for stable operation without vibration. Steel HSS retains its cutting hardness up to an operating temperature of approx. 600°C.
Guideline values for HSS · Ø32 mm
| Material group (ISO 513) | Vc [m/min] | fz [mm/tooth] | n [rpm] · Ø32 | f [mm/min] · Z=3 |
|---|---|---|---|---|
| PStructural and alloy steel | 5–25 | 0.03–0.10 | 50–250 | 4–75 |
| MStainless steel | 6–15 | 0.03–0.06 | 60–150 | 5–27 |
| KCast iron | 10–20 | 0.08–0.12 | 100–200 | 24–70 |
| NNonferrous metals (Al, Cu, brass) | 15–80 | 0.06–0.14 | 150–800 | 27–330 |
| SDifficult-to-machine alloys and titanium | 8 | 0.04 | ≈80 | ≈10 |
Vc — cutting speed, fz — feed per tooth. Columns n and f calculated for D = 32 mm assuming Z = 3, the typical number of cutting edges on counterbores (rounded). For tools made of steel HSS-E the cutting parameters can be increased by 25%.
Spindle speed n = (Vc × 1000) ÷ (π × D), feed rate per minute f = fz × Z × n. Example for steel (Vc = 20, fz = 0.1): n = 20 000 ÷ 100.5 ≈ 200 rpm, f = 0.1 × 3 × 200 ≈ 60 mm/min. Start at the lower end of the range and adjust according to the material and clamping rigidity.
How to extend tool life
The tool is not intended for hardened steels above 45 HRC. For stainless and alloy steels, reduce the speed and use coolant — overheating accelerates cutting edge wear. Make sure the hole diameter matches the pilot Ø26 mm, and before use, check that the taper is compatible MT 3 with the spindle socket — use a Morse taper reduction sleeve if needed.
The shank seats directly in the MT 3 spindle socket of a pillar drill, radial drilling machine, or milling machine. If the spindle has a larger taper, use a Morse taper reduction sleeve; a drift wedge is used for removal. The taper must be clean and dry before insertion — only then can it transmit full torque without slipping.
The larger the cutting diameter, the lower the spindle speed: approx. 50–250 rpm for structural steel, approx. 100–200 rpm for cast iron, and a maximum of approx. 800 rpm for aluminum. Start at the lower end of the range, use a firm, steady feed, and apply coolant.
The Ø26 mm pilot guides the tool in a hole with a diameter of 26 mm (the hole must not be smaller than the pilot). The counterbore machines a flat Ø32 mm seat in it — for nonstandard screw heads, washers, sleeves, or bearing surfaces.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


