







Description
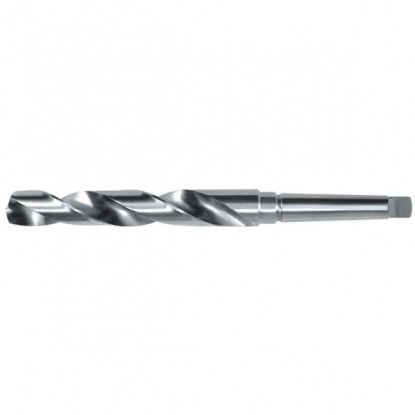
Twist drill with Morse taper shank
| TECHNICAL DATA | |
|---|---|
| Diameter | Ø21.5 NWKc HSSE |
| Standard | DIN 345 |
| Drill type | NWKc — twist drill with taper shank |
| Material | HSSE (cobalt high-speed steel) |
| Overall length l1 | 248 mm |
| Flute length l2 | 150 mm |
| Morse taper | MT2 |
| Point angle | 118° |
| Diameter tolerance | h8 |
| Cutting direction | Right-hand |
Product description and key benefits
The Ø21.5 mm twist drill with an MT2 Morse taper is designed for drilling mounting holes and through holes in structural steel up to 140 mm thick. The MT2 taper with a diameter of 17.780 mm ensures stable torque transmission at drilling diameters from 14 to 23 mm. The Ø21.5 Morse taper drill mounts directly in the spindles of shop-grade pillar drilling machines.
The Ø21.5 Morse taper drill is designed for drilling holes in steel components of various thicknesses — from thin sheet metal to thick-walled sections. The versatile diameter allows one tool to be used for multiple operations at a single workstation. H12 tolerance holes, Ø21.500–Ø21.710 mm; close fits require reaming.
Dimension table for all Morse tapers MT0–MT6
| Taper | Diameter D [mm] | Length [mm] |
|---|---|---|
| MT0 | 9.045 | 49.8 |
| MT1 | 12.065 | 53.5 |
| MT2 | 17.780 | 64.0 |
| MT3 | 23.825 | 80.5 |
| MT4 | 31.267 | 117.5 |
| MT5 | 44.399 | 149.5 |
| MT6 | 63.348 | 210.0 |
REDUCTION SLEEVES COMPATIBLE WITH THE Ø21.5 MM DRILL BIT:
| ✓ | MT2 → MT3 — for a spindle with an MT3 socket |
| ✓ | MT2 → MT4 — for a spindle with an MT4 socket |
| ✓ | MT2 drill drift — for removing the drill bit from the spindle |
Recommended machining conditions for a diameter of Ø21.5 mm
| ISO symbol | Workpiece material | Vc [m/min] | f [mm/rev] | n [rpm] | Vf [mm/min] |
|---|---|---|---|---|---|
| P Steel | Structural steel up to 900 N/mm² | 11÷20 | 0.20 | 163÷296 | 33÷59 |
| K Cast iron | Gray cast iron GG20–GG30 | 13÷16 | 0.20 | 192÷237 | 38÷47 |
| N Copper and Al alloys | Cu, CuZn, Al, and alloys | 25÷28 | 0.25÷0.32 | 370÷415 | 92÷133 |
When drilling holes deeper than 64 mm (3×Ø21.5), periodically retract the drill every 1–1.5×D to remove chips. Use ample emulsion cooling (minimum concentration of 6–8%). Reduce the feed by 30–50% from nominal values.
Range of workpiece materials and application limitations
In S235/S355 structural steels, spot drilling is not necessary — the 118° angle provides self-centering. Spotting with a 90° NC spotting drill is recommended when drilling on uneven or inclined surfaces, where the drill may slip away from the marked point.
The HSS drill can be used for stainless steel with Vc reduced by 40% and ample cooling with a 8–10% emulsion. An HSSE (cobalt) drill of the same diameter is a more efficient option, retaining its hardness up to 650°C.
A pillar or box-column drilling machine with an MT2 spindle and a minimum power rating of 0.75–1.5 kW. Bench drilling machines with a drill chuck are not recommended — they cannot transmit the torque generated at a diameter of 21.5 mm.

Reference: 0000006908 In stock > 10 items
€19.42 brutto
Reference: 1181 In stock > 10 items
€19.42 brutto
Reference: 4910 In stock > 10 items
€27.51 brutto
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


