







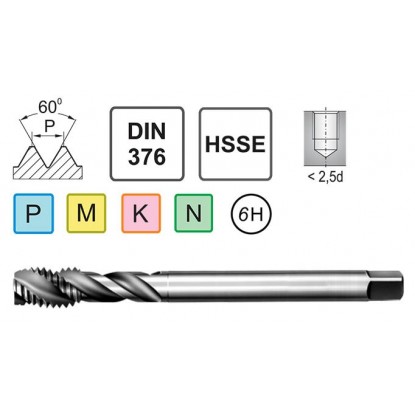

Description
| Technical Data | |
|---|---|
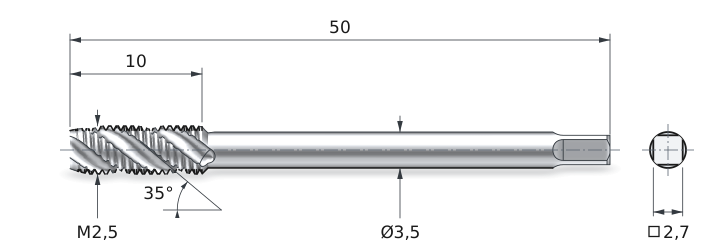
| Nominal Diameter d1 | M2.5 |
| Thread Pitch P | 0.45 mm |
| Helix Angle | 35° |
| Overall Length l1 | 50 mm |
| Flute Length l2 | 10 mm |
| Length l3 | 15 mm |
| Shank Diameter d2 | 3.5 mm |
| Square Drive Size a | 2.7 mm |
| Tap Drill Diameter | 2.05 mm |
| Chamfer | C (2÷3) P |
| Thread tolerance | 6H |
The 35° flute works like a screw conveyor
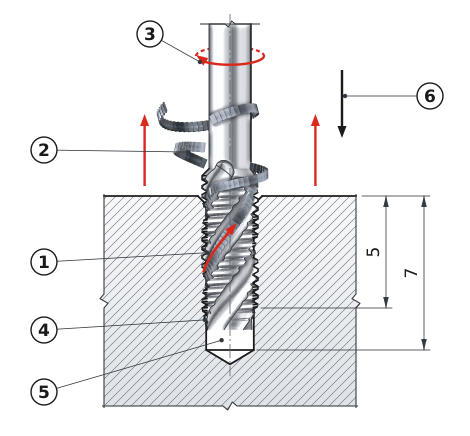
The flutes of this tap follow a right-hand helix at an angle of 35° to the axis. The tap rotates clockwise and advances into the hole. Chips cut by the chamfer enter the flute, and the helix carries them upward like the screw in a meat grinder. The bottom of the hole stays clean, and the cutting edges do not encounter packed chips. The M2.5 x0.45 tap has a reduced shank according to DIN 376: diameter 3.5 mm, square size 2.7 mm.
In this line, manufacturer Fra offers the M2.5 spiral flute machine tap with a long shank, designed for deep tapping in precision engineering. Made from HSSE steel with 5% cobalt, the tool meets DIN 376 requirements and provides a hardness of 65-67 HRC. The 35° spiral flute guarantees controlled chip evacuation when tapping blind holes. The long shank increases clamping rigidity and enables tapping in deep holes inaccessible to the short-shank version.
The M2.5 spiral flute tap is used in toolrooms and prototype shops to manufacture precision mechanical components. The standard pitch of the M2.5 thread is 0.45 mm, with a tap drill diameter of 2.05 mm. The tool works with standard mineral oil-based tapping lubricants and coolant emulsions.
| Material | Cutting speed Vc [m/min] | Spindle speed n [rpm] | Feed f [mm/min] |
|---|---|---|---|
| PSteel | 5-20 | 637-2546 | 287-1146 |
| MStainless steel | 5-10 | 637-1273 | 287-573 |
| KCast iron | 5-15 | 637-1910 | 287-860 |
| NAluminum | 10-25 | 1273-3183 | 573-1432 |
NC spotting drill 90°
Ø 2.05 mm
M2.5
Tolerance 6H
Standard: DIN 376 | Chamfer: C (spiral flute) | Application: blind holes
| Class | Accuracy | Application | Status |
|---|---|---|---|
| 4H / 4g | High | Precision connections, hydraulics | — |
| 6H / 6g | Standard | Machine building, general-purpose | SELECTED |
| 7H / 8g | Low | Large clearance, easy assembly | — |
6H = internal thread (nut, hole) | 6g = external thread (screw)
The M2.5 HSSE spiral flute machine tap to DIN 376 is suitable for structural steels up to 900 MPa, stainless steels, aluminum, and brass. The long shank enables tapping in deep pockets and holes with restricted access.
For an M2.5x0.45 thread in tolerance class 6H, the tap drill diameter should be 2.05 mm. The permissible hole diameter range is 2.05-2.15 mm. A smaller hole increases cutting torque and the risk of tool breakage.
Yes, cooling with tapping oil or minimum quantity lubrication (MQL) is recommended due to the small diameter and risk of breakage. The tool requires careful handling and low cutting speeds.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


