 Polski







- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot
Description
Material HSSE
Thread size M33
ChamferC (2–3) threads
Standard DIN 376
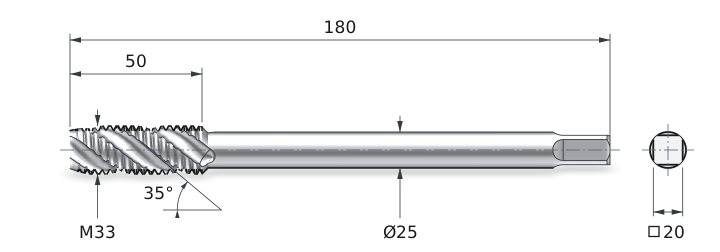
Technical data for the M33 blind-hole tap
| Technical Data | |
|---|---|
| Nominal Diameter d1 | M33 |
| Thread Pitch P | 3.5 mm |
| Helix Angle | 35° |
| Overall Length l1 | 180 mm |
| Flute Length l2 | 50 mm |
| Length l3 | 62 mm |
| Shank Diameter d2 | 25 mm |
| Square Drive Size a | 20 mm |
| Tap Drill Diameter | 29.5 mm |
| Chamfer | C (2÷3) P |
| Thread tolerance | 6H |
How a spiral flute tap evacuates chips from a blind hole
The 35° flute works like a screw conveyor
The flutes of this tap follow a right-hand helix at an angle of 35° to the axis. The tap rotates clockwise and advances into the hole. Chips cut by the chamfer enter the flute, and the helix carries them upward like the screw in a meat grinder. The bottom of the hole stays clean, and the cutting edges do not encounter packed chips. The M33 x3.5 tap has a reduced shank according to DIN 376: diameter 25 mm, square size 20 mm.
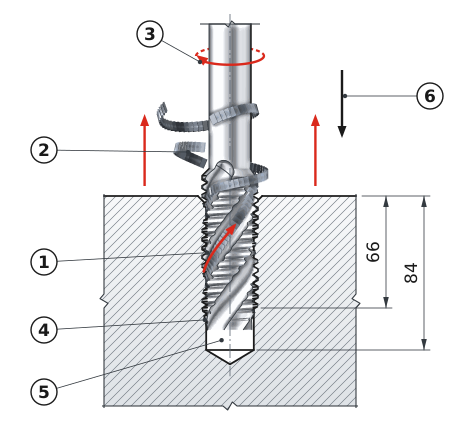
1
The 35° spiral flute carries chips upward from the chamfer.
2
The stepped chip exits the hole and breaks into short pieces.
3
The tap rotates clockwise to cut a right-hand thread.
4
Chamfer C: 2–3 incomplete threads on the tapered lead.
5
Clearance below the tap tip – min. 2 thread pitches above the bottom.
6
Feed 3.5 mm/rev, equal to the pitch of the M33 x3.5 thread.
M33 spiral-flute machine tap – for blind holes
The M33 spiral flute machine tap from the large-diameter series is designed for cutting threads in blind holes up to 2.5D deep. HSSE steel with 5% added cobalt provides a hardness of 65-67 HRC and high cutting-edge heat resistance up to 650°C. The 35° spiral flute ensures controlled chip evacuation when tapping deep blind holes. The form C chamfer makes the tool particularly suitable for blind-hole tapping close to the bottom of the hole. Tolerance 6H in accordance with DIN 376 meets industrial production requirements.
Key features of the M33 spiral flute machine tap
- Manufacturing precision to 6H tolerance guarantees dimensional repeatability and full thread interchangeability in series production of mechanical components
- Compliance with DIN 376 confirms quality and ensures standardized long-shank dimensions compatible with European machine tool holders
- Durability of HSSE steel with 5% cobalt allows operation at temperatures up to 650°C without loss of the cutting edge's mechanical properties
- Compatibility with ER40 holders and tapping heads for CNC machining centers with synchronous tapping capability
- Designed for heavy industry includes gearbox housings, engine blocks, structural components, and large machines
- 35° spiral flutes ensure consistent chip evacuation when tapping blind holes up to 2.5D deep without the risk of breakage
The M33 spiral flute tap is suitable for manufacturing machine housings and industrial gearboxes requiring large internal threads. The standard pitch of the M33 thread is 3.5 mm, with a tap drill diameter of 29.5 mm. The tool works with standard coolant emulsions and tapping oils.
Cutting data for the M33 blind-hole machine tap
| Material | Cutting speed Vc [m/min] | Spindle speed n [rpm] | Feed f [mm/min] |
|---|---|---|---|
| PSteel | 5-20 | 48-193 | 168-676 |
| MStainless steel | 5-10 | 48-96 | 168-336 |
| KCast iron | 5-15 | 48-145 | 168-508 |
| NAluminum | 10-25 | 96-241 | 336-844 |
Thread preparation M33 in a blind hole
1 Spot drilling
NC spotting drill 90°
2 Drilling
Ø 29.5 mm
3 Tapping
M33
✓ Done!
Tolerance 6H
Standard: DIN 376 | Chamfer: C (spiral flute) | Application: blind holes
Tolerance 6H — metric thread tolerance classes
| Class | Accuracy | Application | Status |
|---|---|---|---|
| 4H / 4g | High | Precision connections, hydraulics | — |
| 6H / 6g | Standard | Machine building, general-purpose | SELECTED |
| 7H / 8g | Low | Large clearance, easy assembly | — |
6H = internal thread (nut, hole) | 6g = external thread (screw)
Frequently asked questions
The M33 HSSE spiral flute machine tap is suitable for structural steels up to 900 MPa, stainless steels, aluminum, brass, and gray cast iron. The M33 size is used in heavy industry and special-purpose machine building.
For an M33x3.5 thread of tolerance class 6H, the recommended tap drill diameter is 29.5 mm. The hole tolerance range should be 29.5 to 29.8 mm. Exceeding the upper limit results in an incomplete thread profile.
Yes, cooling with an oil emulsion at a minimum concentration of 8% or with tapping oil is recommended and extends tool life by a factor of 2-3. Intensive cooling under pressure is required when machining stainless steels.
Product accessories


Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you


This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.