





Net price: €64.47
Description
| Technical Data | |
|---|---|
| Nominal Diameter d1 | M32x1 |
| Thread Pitch P | 1 mm |
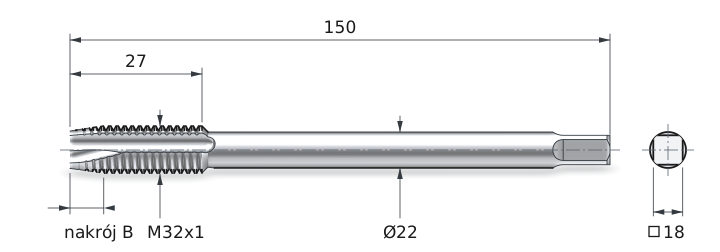
| Overall Length l1 | 150 mm |
| Flute Length l2 | 27 mm |
| Shank Diameter d2 | 22 mm |
| Square Drive Size a | 18 mm |
| Tap Drill Diameter | 31 mm |
| Chamfer | B (3.5÷5.5) P |
| Thread tolerance | 6H |
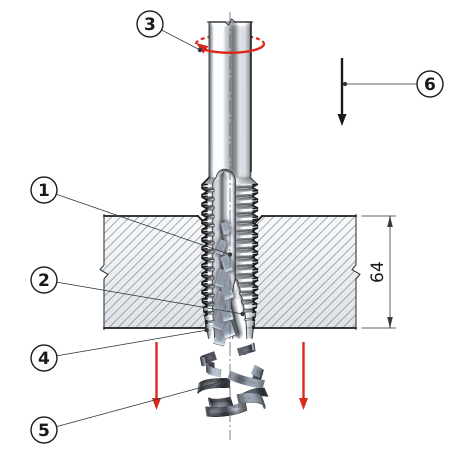
Chips exit at the bottom instead of returning through the thread
The form B chamfer for through holes has a chip breaker at the tip of the tap – an angled cut in the cutting edges. The chip breaker directs the chip down the hole, ahead of the tap tip. The chip curls into a coil, breaks into short pieces and exits the hole on the other side of the workpiece. The threads already cut remain clean because the chip does not pass through them on its way up. The M32x1 tap has a reduced shank according to DIN 374: diameter 22 mm, square size 18 mm.
The M32x1 fine thread machine tap is designed for precision tapping of holes in components requiring extremely accurate adjustment. HSSE high-speed steel construction with 5% added cobalt guarantees a hardness of 65-67 HRC and optimal tool life when machining materials with a tensile strength of up to 800 MPa. The M32x1 fine thread with a very small pitch is used in precision mechanisms and industrial optics where axial position microadjustment to fractions of a millimeter is required on a large diameter.
The M32x1 fine thread machine tap is used in industrial optics, large precision mechanisms, and measuring equipment where microadjustment on a large diameter is required. A thread with such a small pitch is preferred in industrial lenses and precision instruments. Cooling with an emulsion containing EP additives at a concentration of 8-10% is recommended.
| Material | Cutting speed Vc [m/min] | Spindle speed n [rpm] | Feed f [mm/min] |
|---|---|---|---|
| PSteel | 5-20 | 50-199 | 50-199 |
| MStainless steel | 5-10 | 50-99 | 50-99 |
| KCast iron | 5-15 | 50-149 | 50-149 |
| NAluminum | 10-25 | 99-249 | 99-249 |
NC spotting drill 90°
Ø 31 mm
M32x1
Tolerance 6H
Standard: DIN 374 | Chamfer: B (straight) | Application: through holes
| Class | Accuracy | Application | Status |
|---|---|---|---|
| 4H / 4g | High | Precision connections, hydraulics | — |
| 6H / 6g | Standard | Machine building, general-purpose | SELECTED |
| 7H / 8g | Low | Large clearance, easy assembly | — |
6H = internal thread (nut, hole) | 6g = external thread (screw)
The M32x1 fine thread provides 3.5 times the adjustment precision, higher tensile strength, excellent resistance to self-loosening, and the ability to microadjust position.
The recommended tap drill diameter for the M32x1 metric fine thread is 31 mm. Hole accuracy is particularly important for threads with such a small pitch.
The M32x1 thread is used in industrial optics, large precision mechanisms, and measuring equipment where position microadjustment on a large diameter is required.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


