








Description
| Technical data | |
|---|---|
| Thread size D1 | M20x1.5 |
| Thread Pitch P | 1.5 mm |
| Outside Diameter D2 | 45 mm |
| Thickness H1 | 14 mm |
| Number of Chip Holes | 6 |
| Required Shaft Diameter | 19.85 mm |

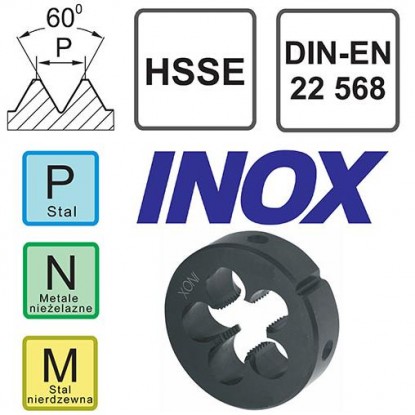
The M20x1.5 HSSE Inox die is a professional round tool made of high-performance high-speed steel (HSSE), specifically designed for cutting external metric fine threads with a diameter of 20 mm and a pitch of 1.5 mm in stainless steel. At this diameter, the fine thread provides increased vibration resistance and higher fatigue strength compared with the standard M20x2.5. The HSSE Inox designation indicates a version with alloying additions (cobalt) that increase resistance to high temperatures and abrasion when machining difficult-to-machine stainless steel. Compliance with DIN 22 568 and a tolerance class of 6g guarantee proper mating with 6H nuts in applications requiring corrosion resistance.
The M20x1.5 HSSE Inox die is a tool selected by shops serving the food, chemical, and pharmaceutical industries, and wherever corrosion resistance is required along with vibration resistance provided by the fine thread. It is particularly recommended for cutting threads on stainless steel rods, pins, and shafts. Use with lubricants specifically intended for stainless steel, such as Terebor, is recommended to achieve optimum quality and extend tool life.
Prepare a stainless steel rod (diameter 19.6-19.65 mm) with a 45° chamfer. Clamp it as securely as possible; stainless steel tends to work-harden during machining. Keep the die perpendicular, making two turns forward and half a turn backward. With stainless steel, reverse more frequently than with carbon steel: every 1.5 turns instead of every 2.
Special threading products such as Terebor or Castrol Ilocut, or cooling and lubricating emulsions for difficult-to-machine materials, are mandatory for stainless steel. Standard oils are insufficient; stainless steel generates high temperatures and adheres to the tool. Apply generously every 2 turns. Never work dry in stainless steel.
Stainless steel work-hardens during machining and adheres to the tool. Causes: excessive feed rate, insufficient lubrication, or failure to use a specialized product. Stop immediately, unscrew the die, and thoroughly clean the flutes (the steel adheres very strongly). Resume with generous lubrication using an Inox product, more frequent reversing (every 1-1.5 turns), and a slower pace than with carbon steel.

Reference: 0000007204 In stock > 10 items
€31.07 brutto
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


