









Net price: €12.11
Description
Type NWCa · DIN 373 · high-speed steel (HSS) · Artykuly Techniczne brand
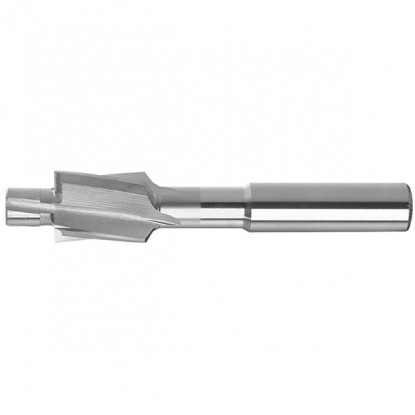
11×6.6 mm counterbore for M6 screws (type NWCa per standard DIN 373) produces flat, perpendicular seats for cylindrical screw heads M6 in a single tool pass. Guidance is provided by a fixed pilot Ø6.6 mm, which runs in the clearance hole and keeps the counterbore coaxial with the hole. High-speed steel HSS allows machining of steel, cast iron, aluminum, and nonferrous metals. A tool from the Polish brand Artykuly Techniczne — manufactured in Poland.
| Technical data | |
|---|---|
| Counterbore diameter D | 11 mm |
| Pilot diameter d₁ | 6.6 mm |
| Shank diameter d | 8 mm |
| Flute length l | 18 mm |
| Pilot length l₁ | 6 mm |
| Shank length l₂ | 35.5 mm |
| Overall length L | 80 mm |
| Number of cutting edges Z | 4 |
| For thread | M6 |
| Material | HSS |
| Standard | DIN 373 NWCa |
| Brand | Artykuly Techniczne |
| Country of manufacture | Poland |
Applications and materials for the M6 counterbore
Typical applications:
| ✓ | Counterboring holes for cylindrical heads of M6 screws (DIN 912 / ISO 4762) |
| ✓ | Flat, perpendicular seat for the head and washer |
| ✓ | Spotfacing around the hole |
| ✓ | Use on CNC machines, drilling machines, and conventional machine tools |
Workpiece materials
Pilot Ø6.6 mm enters the clearance hole and guides the tool coaxially, keeping the counterbore perpendicular to the hole axis and allowing full surface contact under the screw head. Steel HSS retains its cutting hardness up to an operating temperature of approx. 600°C.
Guideline values for HSS · Ø11 mm
| Material group (ISO 513) | Vc [m/min] | fz [mm/tooth] | n [rpm] · Ø11 | f [mm/min] · Z=4 |
|---|---|---|---|---|
| PStructural and alloy steel | 5–25 | 0.03–0.10 | 140–720 | 17–290 |
| MStainless steel | 6–15 | 0.03–0.06 | 170–430 | 21–100 |
| KCast iron | 10–20 | 0.08–0.12 | 290–580 | 95–280 |
| NNonferrous metals (Al, Cu, brass) | 15–80 | 0.06–0.14 | 430–2 300 | 100–1 300 |
| SDifficult-to-machine alloys and titanium | 8 | 0.04 | ≈230 | ≈35 |
Vc — cutting speed, fz — feed per tooth. Columns n and f calculated for D = 11 mm and Z = 4 (rounded). For tools made of steel HSS-E the cutting parameters can be increased by 25%.
Spindle speed n = (Vc × 1000) ÷ (π × D), feed rate per minute f = fz × Z × n. Example for steel (Vc = 20, fz = 0.1): n = 20 000 ÷ 34.6 ≈ 580 rpm, f = 0.1 × 4 × 580 ≈ 230 mm/min. Start at the lower end of the range and adjust according to the material and clamping rigidity.
How to extend tool life
The tool is not intended for hardened steels above 45 HRC. For stainless and alloy steels, reduce the speed and use coolant — overheating accelerates cutting edge wear. Make sure the clearance hole diameter matches the pilot Ø6.6 mm.
The M6 counterbore produces a flat seat for cylindrical heads of M6 screws, including DIN 912 / ISO 4762 socket head cap screws. The Ø6.6 mm pilot enters the clearance hole for M6 and centers the tool. The Ø11 mm counterbore diameter accommodates an M6 socket head cap screw head (Ø10 mm per DIN 912) with a small clearance.
A counterbore (DIN 373) produces a flat-bottomed cylindrical seat for a cylindrical head, such as a socket head cap screw. A countersink (DIN 335) produces a 90° chamfer for a conical/countersunk head. Choose a counterbore for cylindrical head screws and a countersink for countersunk screws.
Yes — for ISO M materials (stainless steel), operate at a reduced cutting speed (Vc approx. 6–15 m/min, or approx. 170–430 rpm for Ø11 mm) and use coolant to limit work hardening and overheating. Do not use the tool on hardened steels above 45 HRC.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


