







Description
dimensions, standard, and shank specifications
| Technical data | |
|---|---|
| Cutting diameter D | Ø3.5 H7 · hole 3.500–3.512 mm |
| Hole tolerance zone | H7 (+0.012 / 0 mm) |
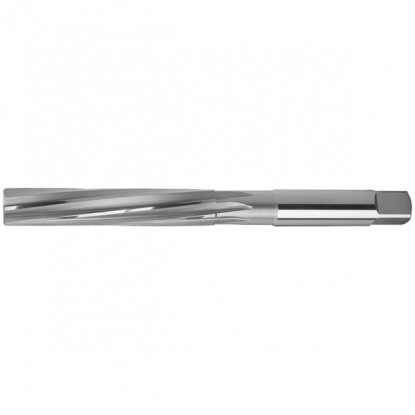
| Type | Fixed-size shank-type hand reamer |
| Dimensional standard | DIN 206 |
| Material | HSS (high-speed steel, manufactured by FRA) |
| Flute length l | 35 mm |
| Shank length l₁ | 26 mm |
| Overall length L | 71 mm |
| Number of cutting edges Z | 6 (straight flutes) |
| Shank / drive | Straight shank with square drive (for a tap wrench) |
construction, operation, and applications
The tool body is made from HSS high-speed steel supplied by the Serbian company FRA. The cutting section has straight flutes and 6 cutting edges: more edges distribute cutting resistance more evenly, improving hole roundness and reducing vibration compared with a two-edge drill. The extended tapered lead centers the reamer in the hole, while the square drive on the shank transfers torque from the tap wrench.
Reaming is a finishing operation, not a roughing operation. After drilling, the hole falls within the broad IT10–IT11 tolerance range; the reamer tightens its tolerance to H7, while improving the hole wall finish. Bear in mind that the tool follows the existing hole and will not straighten a crooked hole — so the initial hole must be drilled perpendicular to the surface. Unlike the machine version, the hand version has an extended tapered lead and more cutting edges, promoting even cutting. It is well suited to finishing holes for pins and shafts, when a running fit or a light interference fit is required.
final tolerance zone of the machined hole
| Designation | Hole Ø range [mm] | Deviations [mm] | IT tolerance grade |
|---|---|---|---|
| 3.5 H6 | 3.500 – 3.508 | +0.008 / 0 | 8 µm |
| 3.5 H7 | 3.500 – 3.512 | +0.012 / 0 | 12 µm this product |
| 3.5 H8 | 3.500 – 3.518 | +0.018 / 0 | 18 µm |
| 3.5 H9 | 3.500 – 3.530 | +0.030 / 0 | 30 µm |
| 3.5 H11 | 3.500 – 3.575 | +0.075 / 0 | 75 µm |
Your reamer produces tolerance grade H7 — finished hole Ø3.500–3.512 mm; the value is stated directly, without conversion from tables. A narrower tolerance zone means a more accurate hole. The reamed surface is smooth — typically Ra 0.4–1.6 µm, significantly better than after drilling alone (approx. 1.6–3.2 µm).
tap wrench operation, allowance and predrilled hole
The reamer engages with the tap wrench through the square drive on the shank — guide it by hand, steadily and in one direction, with moderate pressure. For Ø3.5 H7, leave a 0.1 mm allowance on diameter; predrill the hole with a drill of Ø3.4 mm, then finish with the reamer. With small diameters, guide the tool gently without lateral pressure — the slender shank is easily overloaded. Generous cutting oil lubrication is essential — it reduces cutting resistance and improves the surface finish to Ra 0.4–1.6 µm (approx. 1.6–3.2 µm after drilling).
groups P1.2–P1.3 according to the material classification
Yes — nonferrous metals and light alloys (brass, bronze, copper, aluminum) are among the recommended materials in group P1.2–P1.3, alongside unalloyed and free-machining steels. The limitations are hardened steels and hardened stainless steels, for which HSS is too soft.
The hole size falls within 3.500–3.512 mm (H7, +0.012 / 0 mm), and roughness drops to Ra 0.4–1.6 µm. By comparison, drilling alone leaves approx. 1.6–3.2 µm and a much looser IT10–IT11 tolerance grade.
The optimum allowance is 0.1 mm on diameter. Predrill with a Ø3.4 mm drill; excessive allowance worsens the surface finish and loads the cutting edges, while too little will not remove drilling marks.

Reference: 0000005480 In stock > 10 items
€74.45 brutto
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


