







Description
| Technical Data | |
|---|---|
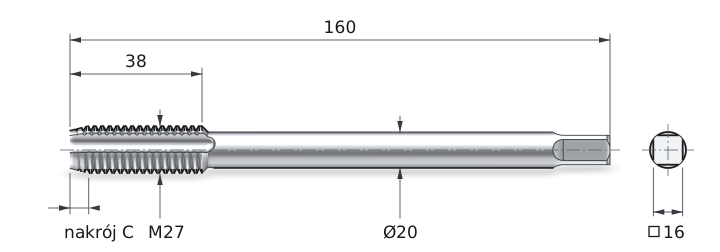
| Nominal Diameter d1 | M27 |
| Thread Pitch P | 3 mm |
| Overall Length l1 | 160 mm |
| Flute Length l2 | 38 mm |
| Shank Diameter d2 | 20 mm |
| Square Drive Size a | 16 mm |
| Tap Drill Diameter | 24 mm |
| Chamfer | C (2÷3) P |
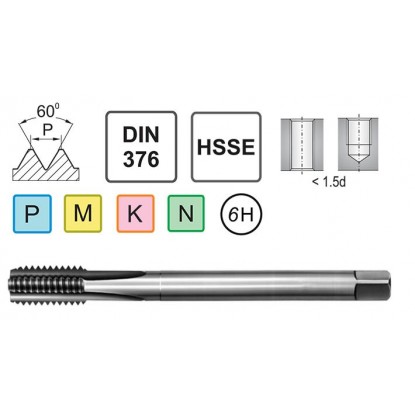
| Thread tolerance | 6H |
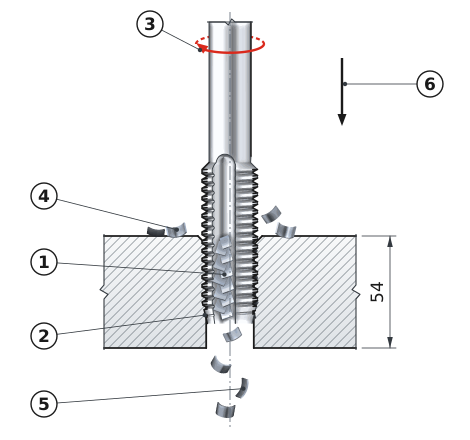
The flute holds the chips until the tap is reversed out
The straight flute runs parallel to the tap axis. There is no helix to carry chips upward. The chamfer cutting edges are not ground at an angle, so they do not push chips downward. Short chips break into fragments and remain in the flute, next to the cutting edges that produced them. They leave the hole only when the tap is backed out. The M27 x3 tap has a reduced shank to DIN 376: diameter 20 mm, square size 16 mm.
The M27 INOX machine tap is a professional tool for cutting M27 internal threads in stainless, structural, and alloy steels. Its HSSE high-speed steel construction with 5% cobalt provides a hardness of 66 HRC and high resistance to temperatures up to 650°C in the cutting zone. Form C with straight flutes allows tapping of both through and blind holes without changing tools. The 6H tolerance in accordance with DIN 376 ensures dimensional repeatability. The Fra M27 general-purpose machine tap is designed for toolrooms and CNC machining center operators.
The M27 machine tap for through and blind holes is used in the production of industrial fittings and pneumatic components requiring leak-tight threaded connections. Cooling with an EP emulsion at a minimum concentration of 8% extends tool life by a factor of 2-3. The tap drill diameter for an M27 thread is 24 mm for a coarse thread with a pitch of 3 mm.
| Material | Cutting speed Vc [m/min] | Spindle speed n [rpm] | Feed f [mm/min] |
|---|---|---|---|
| PSteel | 5-20 | 59-236 | 177-708 |
| MStainless steel / INOX | 5-10 | 59-118 | 177-354 |
| KCast iron | 5-15 | 59-177 | 177-531 |
| NAluminum | 10-25 | 118-295 | 354-885 |
NC spotting drill 90°
Ø 24 mm
M27
Tolerance 6H
Standard: DIN 376 | Chamfer: C (straight) | Application: general-purpose (through and blind holes)
| Class | Accuracy | Application | Status |
|---|---|---|---|
| 4H / 4g | High | Precision connections, hydraulics | — |
| 6H / 6g | Standard | Machine building, general-purpose | SELECTED |
| 7H / 8g | Low | Large clearance, easy assembly | — |
6H = internal thread (nut, hole) | 6g = external thread (screw)
The M27 HSSE tap with form C and straight flutes is universal – suitable for both through holes and blind holes. Its design ensures proper chip evacuation in both hole types.
The M27 HSSE tap produces an internal thread to tolerance class 6H. The designation 6H specifies the permissible deviations of the thread pitch and minor diameters – the digit 6 indicates the tolerance zone width (medium), and the letter H indicates the position of the zone at the zero line. Tolerance 6H ensures proper fit with screws to tolerance 6g.
When tapping stainless steels, an EP emulsion at a minimum concentration of 8% or tapping oil is recommended for cooling. Cooling extends tool life by a factor of 2-3 and improves the thread surface finish.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


