






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot
Description
Material HSSE
Thread size M10
ChamferC (2–3) threads
Standard DIN 376
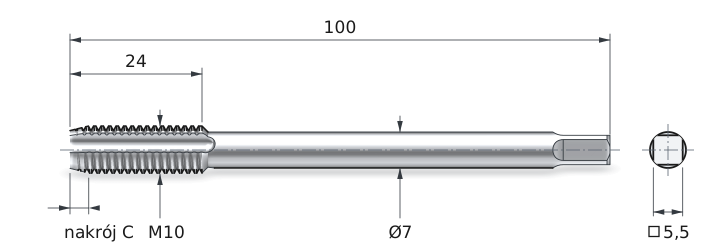
Technical data for the M10 HSSE INOX general-purpose machine tap
| Technical Data | |
|---|---|
| Nominal Diameter d1 | M10 |
| Thread Pitch P | 1.5 mm |
| Overall Length l1 | 100 mm |
| Flute Length l2 | 24 mm |
| Shank Diameter d2 | 7 mm |
| Square Drive Size a | 5.5 mm |
| Tap Drill Diameter | 8.5 mm |
| Chamfer | C (2÷3) P |
| Thread tolerance | 6H |
Where chips remain in a straight-flute tap
The flute holds the chips until the tap is reversed out
The straight flute runs parallel to the tap axis. There is no helix to carry chips upward. The chamfer cutting edges are not ground at an angle, so they do not push chips downward. Short chips break into fragments and remain in the flute, next to the cutting edges that produced them. They leave the hole only when the tap is backed out. The M10 x1.5 tap has a reduced shank to DIN 376: diameter 7 mm, square size 5.5 mm.
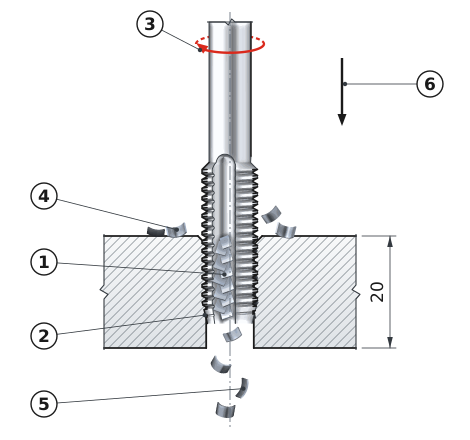
1
Straight flute – chips remain in the flute, next to the cutting edges that produced them.
2
Chamfer C: 2–3 incomplete threads on the tapered lead.
3
The tap rotates clockwise to cut a right-hand thread.
4
Individual fragments exit at the top, onto the workpiece surface.
5
A few fragments fall below the tip and exit through the bottom of the hole.
6
Feed 1.5 mm/rev, equal to the pitch of the M10 x1.5 thread.
M10 INOX machine tap – compliant with DIN 376
This HSSE series model, designed for CNC machining and precision tapping in industrial toolrooms, features a long shank in accordance with DIN 376. The M10 INOX machine tap has a reinforced straight shank that increases rigidity at high spindle speeds. With 5% added cobalt, the tool maintains a hardness of 66 HRC even at cutting zone temperatures up to 650°C. Form C with straight flutes provides versatility across different hole types. The 6H tolerance guarantees the dimensional repeatability required in precision manufacturing.
Key advantages of the M10 DIN 376 tap
- Material versatility covering structural steels up to 800 MPa, austenitic stainless steels, GGG40 ductile cast iron, and 6000 series aluminum alloys
- Durability increased by the addition of cobalt in HSSE steel allows 400-600 threads to be cut in structural steel with proper emulsion cooling
- Compatibility with ER20 holders and collets for precise clamping on machining centers with axial compensation and automatic tool changing
- Precision to tolerance class 6H for demanding fit tolerances in series production of mechanical, hydraulic and pneumatic components
- Long shank to DIN 376 provides increased clamping rigidity and eliminates vibration at high spindle speeds on CNC machines
- Universal M10 machine tap with form C allows tapping of through holes and blind holes without changing the tool or parameters
The M10 HSSE DIN 376 machine tap is used in toolrooms and prototype shops for one-off and small-batch production of precision components. The M10 machine tap for through holes and blind holes also performs well in maintenance work. The tap drill diameter for the M10 thread is 8.5 mm.
Cutting data for the universal M10 HSSE INOX machine tap
| Material | Cutting speed Vc [m/min] | Spindle speed n [rpm] | Feed f [mm/min] |
|---|---|---|---|
| PSteel | 5-20 | 159-637 | 238-956 |
| MStainless steel / INOX | 5-10 | 159-318 | 238-477 |
| KCast iron | 5-15 | 159-477 | 238-716 |
| NAluminum | 10-25 | 318-796 | 477-1194 |
Thread preparation M10
1 Spot drilling
NC spotting drill 90°
2 Drilling
Ø 8.5 mm
3 Tapping
M10
✓ Done!
Tolerance 6H
Standard: DIN 376 | Chamfer: C (straight) | Application: general-purpose (through and blind holes)
Tolerance 6H — metric thread tolerance classes
| Class | Accuracy | Application | Status |
|---|---|---|---|
| 4H / 4g | High | Precision connections, hydraulics | — |
| 6H / 6g | Standard | Machine building, general-purpose | SELECTED |
| 7H / 8g | Low | Large clearance, easy assembly | — |
6H = internal thread (nut, hole) | 6g = external thread (screw)
Frequently asked questions
With proper cooling and lubrication, the M10 HSSE tap produces 400-600 threads in structural steel or 250-350 threads in stainless steel. Dry machining reduces tool life by 40-50%.
Yes, the M10 HSSE tap with 5% cobalt is designed for austenitic stainless steels 304 and 316. The cobalt addition increases heat resistance up to 650°C in the cutting zone.
An HSSE tap contains 5% cobalt, which increases hardness from 64 to 66 HRC and heat resistance to 650°C. HSSE is suitable for stainless steels, while HSS is suitable only for structural steels up to 800 MPa.
Product accessories


Hand tap M10 DIN 352/3 6H HSS Bucovice
Reference: 0000006583 In stock > 10 items
€11.84
€14.57 brutto


Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you


This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.