








Description
| Technical Data | |
|---|---|
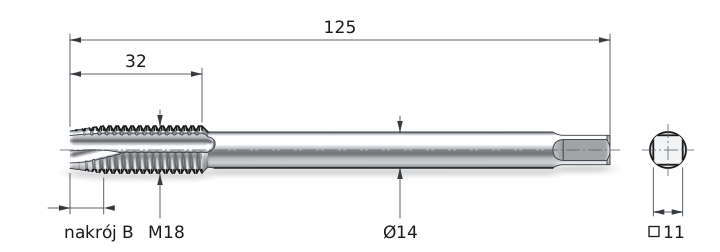
| Nominal Diameter d1 | M18 |
| Thread Pitch P | 2.5 mm |
| Overall Length l1 | 125 mm |
| Flute Length l2 | 32 mm |
| Shank Diameter d2 | 14 mm |
| Square Drive Size a | 11 mm |
| Tap Drill Diameter | 15.5 mm |
| Chamfer | B (3.5÷5.5) P |
| Thread tolerance | 6H |
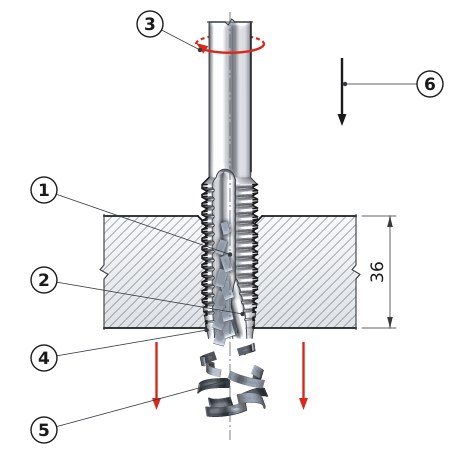
Chips exit at the bottom instead of returning through the thread
The type B through-hole chamfer has a chip breaker at the tip of the tap – an angled notch in the cutting edges. The chip breaker directs chips down the hole, ahead of the tap tip. The chips curl into a spring shape, break into short pieces and exit the hole on the other side of the workpiece. The threads already cut remain clean because the chips do not pass through them on their way up. The M18 x2.5 tap has a reduced shank to DIN 376: diameter 14 mm, square size 11 mm.
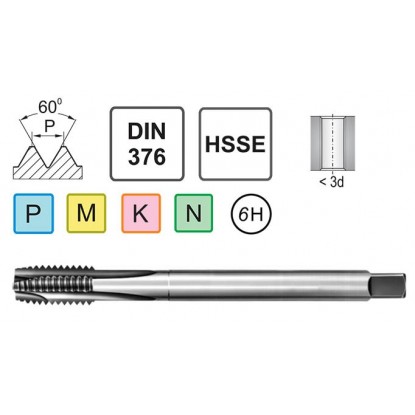
The M18 through-hole machine tap from the HSSE series is designed for cutting M18 internal threads in through holes on CNC and conventional machine tools. The long shank according to DIN 376 provides increased clamping rigidity and improved tool guidance when tapping large diameters in deep holes requiring high precision. High-speed steel with 5% cobalt provides a hardness of 65-67 HRC and high heat resistance in the cutting zone up to 650°C. The tool is intended for professional toolrooms, maintenance departments, and CNC operators.
The M18 machine tap for through holes is used in series production, heavy machine building, and maintenance departments for repairs and thread restoration in mechanical components. Form B with straight flutes ensures efficient forward chip evacuation. The tool requires cooling with an oil emulsion at a minimum concentration of 8-10% to maintain optimum tool life.
| Material | Cutting speed Vc [m/min] | Spindle speed n [rpm] | Feed f [mm/min] |
|---|---|---|---|
| PSteel | 5-20 | 88-354 | 220-885 |
| MStainless steel | 5-10 | 88-177 | 220-442 |
| KCast iron | 5-15 | 88-265 | 220-662 |
| NAluminum | 10-25 | 177-442 | 442-1105 |
NC spotting drill 90°
Ø 15.5 mm
M18
Tolerance 6H
Standard: DIN 376 | Chamfer: B (straight) | Application: through holes
| Class | Accuracy | Application | Status |
|---|---|---|---|
| 4H / 4g | High | Precision connections, hydraulics | — |
| 6H / 6g | Standard | Machine building, general-purpose | SELECTED |
| 7H / 8g | Low | Large clearance, easy assembly | — |
6H = internal thread (nut, hole) | 6g = external thread (screw)
The M18 HSSE tap performs well in structural steels up to 800 MPa, alloy steels, austenitic stainless steels 304/316, gray and ductile cast iron, aluminum, and brass.
The recommended tap drill diameter for the M18 coarse thread is 15.5 mm. Accurate hole preparation ensures a full thread profile and minimizes the load on the tap.
With proper cooling, the M18 HSSE tap cuts 300-500 threads in structural steel and 150-250 threads in stainless steel. Dry operation reduces tool life by 30-40%.

Reference: 0000008242 In stock < 10 items
€26.54 brutto

Reference: 13293 In stock > 10 items
€18.77 brutto
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


