 Polski






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot
Description
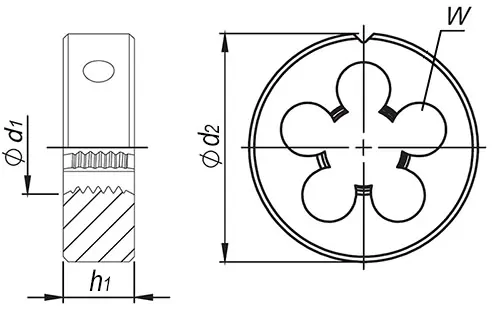
Technical data die M16
| Technical Data | |
|---|---|
| Thread size D1 | M16 |
| Thread Pitch P | 2 mm |
| Outside Diameter D2 | 45 mm |
| Thickness H1 | 18 mm |
| Number of Chip Holes | 5 |
| Required Shaft Diameter | 15.82 mm |
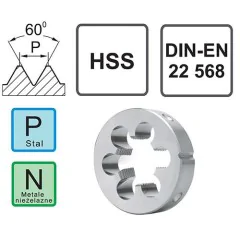
M16 HSS DIN 22568 die – professional threading of load-bearing components
The M16 die is a robust tool designed to cut external threads on heavy rods and structural shafts. Made from high-speed steel (HSS) in accordance with DIN 22568, the M16 metric die is used to cut threads in structural steels, aluminum alloys, and gray cast iron in applications requiring high load-bearing capacity of joints, with a tolerance of 6g and a pitch of 2.0 mm.
Key applications of the M16 HSS die
- Threading for heavy structures is ideal for the machinery industry, structural steel construction, and industrial equipment assembly
- HSS with increased hardness allows repeated use in production environments
- Popular in fabrication shops producing machine frames, supports, and large connecting components
- The DIN 22568 standard ensures dimensional accuracy and compatibility with standard nuts
- Proven in industrial plant maintenance departments when reconditioning machine joints
Structural steel erectors and industrial machinery mechanics use the M16 threading die when building and repairing high-power equipment. Essential in plants manufacturing mining equipment, construction machinery, and power installations requiring strong bolted joints. Choose a tool that withstands intensive use in the most demanding industrial conditions.
Frequently asked questions
Remove scale and rust from the rod with a diameter of 15.75-15.80 mm using a wire brush or belt grinder. Check cylindricity with a caliper at a minimum of three points - the deviation must not exceed 0.08 mm. Make a lead-in chamfer over a length of 4-5 mm using a lathe or grinder. Secure the workpiece in a vise or lathe chuck to ensure stability during threading.
Typical problems include excessive cutting edge wear due to insufficient lubrication, sharp burrs on aluminum threads, and difficulty maintaining perpendicular alignment during hand threading. Working too quickly causes the tool to heat up and lose hardness. In steels harder than 25 HRC, the die may jam unless it is reversed every half turn to break the chips.
For hand threading, generous lubrication with threading compounds is sufficient without active cooling. For machine threading on a lathe or milling machine, emulsion coolant supplied under pressure to the cutting zone is recommended. In batch production, cooling extends die life by 50-70 percent and improves thread surface finish. Aluminum can be threaded dry with minimal kerosene lubrication.
Product accessories


Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you




This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.