







- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot
Description
SIZEØ9 mm
TAPER1:50
STANDARDDIN 9
MATERIALHSS M2
| Technical data | |
|---|---|
| Designation | 9 NRSk (DIN 9) |
| Cutting diameter D | 9 mm |
| Shank diameter d | 10 mm |
| Flute length l | 145 mm |
| Overall length L | 180 mm |
| Number of cutting edges Z | 7 (straight) |
| Design | Form A (straight flutes) |
| Taper ratio | 1:50 (angle 1.146°) |
| Material | HSS (M2), high-speed steel |
| Shank | straight shank with square drive (hand operation) |
| Intended use | holes for taper pins, ISO 2339 / 8736 |
| Pilot hole (drill) | ≈ Ø9 mm |
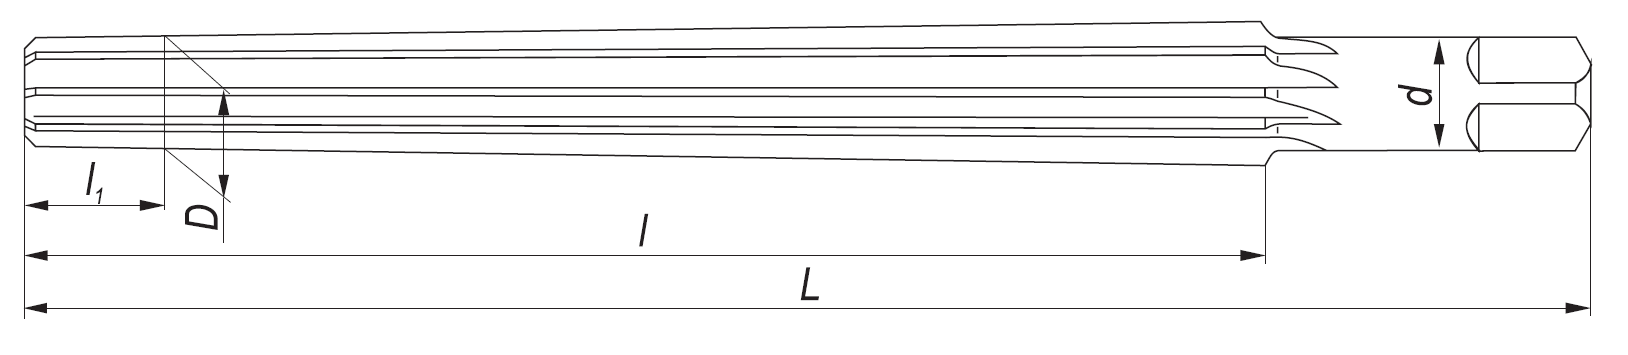
Tapered hand reamer 9 NRSk – features and applications
DIN 9 standard, HSS, 1:50 taper for taper pins
Tapered hand reamer 9 NRSk is a finishing tool for precision reaming of holes with a taper of 1:50 — the standard for fitting taper pins. Made of high-speed steel HSS, compliant with the dimensional standard DIN 9, with a square drive for a tap wrench.
A taper pin with a taper of 1:50 combines precision with removability. One taper geometry fits an entire family of pins: ISO 2339 (= DIN 1, unhardened), ISO 8736 (with internal thread), ISO 8737 (with external thread) and DIN 258 (with a flat).
The pin precisely locates two components relative to each other and transmits transverse loads. Its shallow taper makes it self-locking in the hole while remaining removable — it can be driven out and reinstalled without losing the fit. This is the key advantage of a tapered joint over a cylindrical one.
The reamer gives the drilled hole an accurate, smooth tapered profile in which the pin seats with the correct contact pressure over the full contact length. Straight cutting edges (Z = 7, Form A design) distribute the cut in a thin layer, providing steady guidance and low hole wall roughness.
Grade M2 HSS combines hardness with impact toughness, withstanding interrupted manual cutting of materials in group P. Hand operation with a tap wrench provides full feed control — in short production runs and repair work, this can be more valuable than machine productivity.
Guide the tool slowly, applying even pressure and removing chips regularly; this keeps the hole wall smooth and ensures pin contact along the entire taper. In precision engineering and maintenance, the reamer is suitable for locating clevises, bearing blocks, and table supports, as well as securing levers, gears, and sleeves on shafts.
Taper pin installation process
From drilling to the finished joint
Machining a hole for a 1:50 taper pin step by step
1Pilot drilling
Cylindrical hole Ø ≈ 9 mm
2Step drilling
Deep holes: 2–3 diameters
3Hand reaming
Tap wrench + oil, rotation in one direction
✓Pin installation
Taper pin Ø9 · 1:50
The pilot hole diameter is taken as equal to the small diameter of the pin (reamer tip). The stock allowance increases toward the large end, so deep holes are step-drilled.
1:50 taper — calculation and tips
Why selecting the correct taper is critical
With a taper of 1:50 the diameter increases by 1 mm for every 50 mm of length. Over a 145 mm cutting section, this gives an increase of 145 ÷ 50 = 2.9 mm — from Ø9 mm at the tip to ≈ Ø11.9 mm at the shank. The included taper angle is 2 · arctan(1/100) = 1.146°.
▲
Do not confuse taper ratios
A taper ratio of 1:50 is specifically for taper pins. This is not a Morse taper (≈ 1:20) or a taper pipe thread (1:16) — a tool with the wrong taper prevents a proper fit. Work by hand, using oil and a steady rotation in one direction; do not reverse rotation, as this may chip the cutting edges. HSS loses hardness above 600 °C — avoid overheating. Also remember that a pinned joint relies on friction and transmits less torque than a key or thread — it is intended for locating, not for transmitting drive.
Workpiece material selection
Suitability by machining group
| Material | Suitability | Note |
|---|---|---|
| Structural carbon steels | Recommended | primary workpiece material (HSS M2) |
| Alloy steels (up to ~1000 MPa) | Recommended | oil cooling |
| Nonferrous metals (brass, bronze, aluminum) | Recommended | easy machining |
| Stainless steel, titanium | Conditionally suitable | HSS-Co M35 version recommended |
| Hardened steels (> 45 HRC) | Not recommended | cemented carbide required |
Other sizes in the series and accessories
| ▸ | Tapered hand reamers NRSk DIN 9 — range Ø3 to Ø50 mm (including 5, 7, 8, 10, 12) |
| ▸ | Tap wrench (holder) for hand reamers with square drives |
| ▸ | 1:50 taper pins to ISO 2339, ISO 8736, ISO 8737, and DIN 258 |
| ▸ | Cutting oil to facilitate hand reaming |
Frequently asked questions
Tapered reamer 9 NRSk DIN 9
It is used for finish reaming holes with a 1:50 taper for taper pins to ISO 2339 / 8736 / 8737. It gives the hole an accurate, smooth tapered profile in which the pin seats with even contact pressure. The nominal diameter 9 corresponds to the small diameter of the pin.
Drill a cylindrical pilot hole with a diameter close to the small diameter of the pin, approximately Ø9 mm. For deep seating, step drilling (2–3 stepped diameters) is recommended to reduce the stock allowance at the large end and ease the load on the hand reamer.
The diameter is fixed — the 1:50 taper increases from Ø9 mm at the small end, so the fit is determined by the taper profile, not just the pin size. Select the pin length to suit the combined thickness of the joined components so that it protrudes slightly on both sides. After reaming, seat the pin with light taps until fully seated; full, even contact along the entire taper indicates a correct fit.
No — threading requires a different tool. For taper pipe threads (NPT, NPTF, RC/BSPT, 1:16 taper), a separate 1:16 tapered reamer to ASME B94.2 is used, followed by an NPT or RC tap to cut the thread. The 9 NRSk DIN 9 reamer has a 1:50 taper and prepares holes exclusively for taper pins.
Product accessories


Set of metal drill bits 1-13 HSSE Inox DIN 338
Reference: 0000005480 In stock > 10 items
€50.00
€61.50 brutto


HSSE 9.8 cobalt metal drill bit DIN 338
Reference: 0000008587 In stock > 10 items
€3.68
€4.53 brutto
Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you


This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.