







Description
| Technical data | |
|---|---|
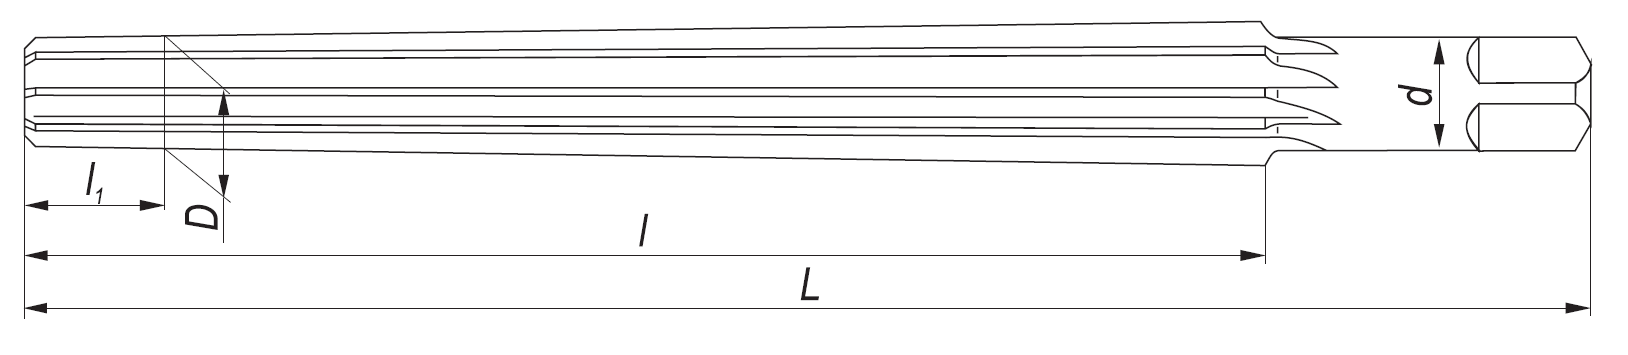
| Designation | 50 NRSk (DIN 9) |
| Cutting diameter D | 50 mm |
| Shank diameter d | 50 mm |
| Flute length l | 360 mm |
| Overall length L | 460 mm |
| Number of cutting edges Z | 11 (straight) |
| Design | Form A (straight flutes) |
| Taper ratio | 1:50 (angle 1.146°) |
| Material | HSS (M2), high-speed steel |
| Shank | straight shank with square drive (hand operation) |
| Intended use | holes for taper pins, ISO 2339 / 8736 |
| Pilot hole (drill) | ≈ Ø50 mm |
DIN 9 standard, HSS, 1:50 taper for taper pins
A taper pin with a taper of 1:50 combines precision with removability. One taper geometry fits an entire family of pins: ISO 2339 (= DIN 1, unhardened), ISO 8736 (with internal thread), ISO 8737 (with external thread) and DIN 258 (with a flat).
The pin precisely locates two components relative to each other and transmits transverse loads. Its shallow taper makes it self-locking in the hole while remaining removable — it can be driven out and reinstalled without losing the fit. This is the key advantage of a tapered joint over a cylindrical one.
The reamer gives the drilled hole an accurate, smooth tapered profile in which the pin seats with the correct contact pressure over the full contact length. Straight cutting edges (Z = 11, Form A design) distribute the cut in a thin layer, providing steady guidance and low hole wall roughness.
Grade M2 HSS combines hardness with impact toughness, withstanding interrupted manual cutting of materials in group P. Hand operation with a tap wrench provides full feed control — in short production runs and repair work, this can be more valuable than machine productivity.
Guide the tool slowly, applying even pressure and removing chips regularly; this keeps the hole wall smooth and ensures pin contact along the entire taper. In precision engineering and maintenance, the reamer is suitable for locating clevises, bearing blocks, and table supports, as well as securing levers, gears, and sleeves on shafts.
From drilling to the finished joint
Cylindrical hole Ø ≈ 50 mm
Deep holes: 2–3 diameters
Tap wrench + oil, rotation in one direction
Taper pin Ø50 · 1:50
The pilot hole diameter is taken as equal to the small diameter of the pin (reamer tip). The stock allowance increases toward the large end, so deep holes are step-drilled.
Why selecting the correct taper is critical
With a taper of 1:50 the diameter increases by 1 mm for every 50 mm of length. Over a 360 mm cutting section, this gives an increase of 360 ÷ 50 = 7.2 mm — from Ø50 mm at the tip to ≈ Ø57.2 mm at the shank. The included taper angle is 2 · arctan(1/100) = 1.146°.
A taper ratio of 1:50 is specifically for taper pins. This is not a Morse taper (≈ 1:20) or a taper pipe thread (1:16) — a tool with the wrong taper prevents a proper fit. Work by hand, using oil and a steady rotation in one direction; do not reverse rotation, as this may chip the cutting edges. HSS loses hardness above 600 °C — avoid overheating. Also remember that a pinned joint relies on friction and transmits less torque than a key or thread — it is intended for locating, not for transmitting drive.
Suitability by machining group
| Material | Suitability | Note |
|---|---|---|
| Structural carbon steels | Recommended | primary workpiece material (HSS M2) |
| Alloy steels (up to ~1000 MPa) | Recommended | oil cooling |
| Nonferrous metals (brass, bronze, aluminum) | Recommended | easy machining |
| Stainless steel, titanium | Conditionally suitable | HSS-Co M35 version recommended |
| Hardened steels (> 45 HRC) | Not recommended | cemented carbide required |
Other sizes in the series and accessories
| ▸ | Tapered hand reamers NRSk DIN 9 — range Ø3 to Ø50 mm (including 5, 7, 8, 10, 12) |
| ▸ | Tap wrench (holder) for hand reamers with square drives |
| ▸ | 1:50 taper pins to ISO 2339, ISO 8736, ISO 8737, and DIN 258 |
| ▸ | Cutting oil to facilitate hand reaming |
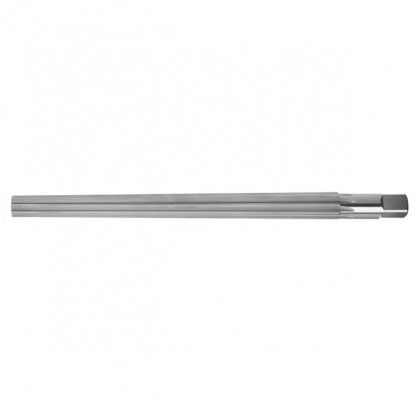
Tapered reamer 50 NRSk DIN 9
It is used for finish reaming holes with a 1:50 taper for taper pins to ISO 2339 / 8736 / 8737. It gives the hole an accurate, smooth tapered profile in which the pin seats with even contact pressure. The nominal diameter 50 corresponds to the small diameter of the pin.
Drill a cylindrical pilot hole with a diameter close to the small diameter of the pin, approximately Ø50 mm. For deep seating, step drilling (2–3 stepped diameters) is recommended to reduce the stock allowance at the large end and ease the load on the hand reamer.
The diameter is fixed — the 1:50 taper increases from Ø50 mm at the small end, so the fit is determined by the taper profile, not just the pin size. Select the pin length to suit the combined thickness of the joined components so that it protrudes slightly on both sides. After reaming, seat the pin with light taps until fully seated; full, even contact along the entire taper indicates a correct fit.
No — threading requires a different tool. For taper pipe threads (NPT, NPTF, RC/BSPT, 1:16 taper), a separate 1:16 tapered reamer to ASME B94.2 is used, followed by an NPT or RC tap to cut the thread. The 50 NRSk DIN 9 reamer has a 1:50 taper and prepares holes exclusively for taper pins.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


