 Polski






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot

Description
M8 DIN 371 B machine tap – for through holes
Technical data and dimensions to DIN 371
| Technical data | |
|---|---|
| Thread | M8 x1.25 (metric coarse) |
| Standard | DIN 371, reinforced shank |
| Flute | straight |
| Chamfer | B (for through holes, with chip breaker), 3.5–5.5 threads |
| Thread tolerance | 6H |
| Material | HSSE (HSS-Co5) |
| Overall length | 90 mm |
| Threaded section length | 20 mm |
| Length to shank | 35 mm |
| Shank diameter | 8 mm |
| Square drive | 6.2 mm |
| Tap drill | 6.8 mm |
| Manufacturer | Varel |
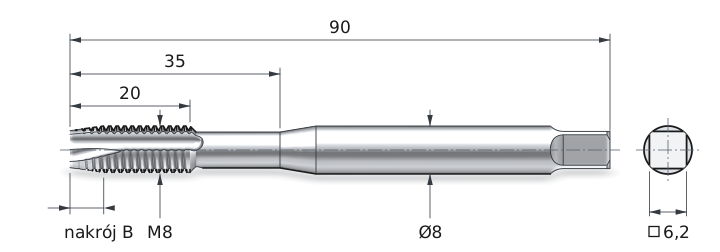
M8 machine tap Varel cuts threads in through holes, meaning holes drilled all the way through. It has straight flutes and cutting edges ground at an angle on the chamfer. These cutting edges push chips ahead of the tip, down the hole, and the chips exit through the other side of the workpiece.
The form B chamfer distributes the cutting action over 3.5–5.5 threads, so each cutting edge removes a thin layer. Cobalt-alloyed HSSE steel and 6H tolerance produce threads for M8 screws in steel, stainless steel, cast iron, and aluminum.
MaterialHSSE, 5% cobalt
Flutestraight
ChamferB, 3.5–5.5 threads
Tolerance6H
How the type B through-hole chamfer pushes chips down the hole
Chips exit at the bottom instead of returning through the thread
The form B chamfer for through holes has a chip breaker at the front of the tap – an angled notch in the cutting edges. The chip breaker directs chips down the hole, ahead of the tap tip. The chips curl into a spring shape, break into short pieces, and exit the hole on the other side of the workpiece. The threads already cut remain clean because the chips do not pass back through them on their way upward.
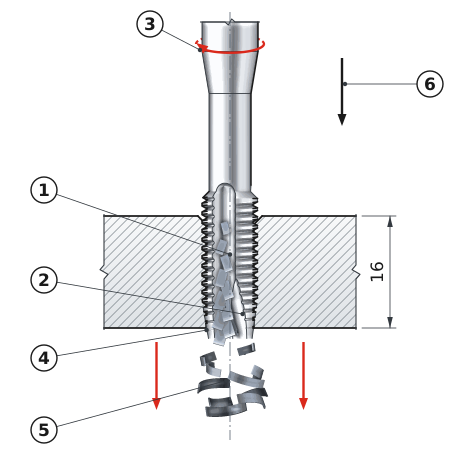
1
Straight flute – chips do not enter it; the flute carries lubricant to the cutting edges.
2
The chip breaker at the tip of the tap directs chips down the hole.
3
The tap rotates clockwise to cut a right-hand thread.
4
B chamfer: 3.5–5.5 incomplete threads on the entry taper.
5
The chips break into segments: individual pieces at the top of the hole, with progressively more farther down. They fall out below the workpiece.
6
Feed 1.25 mm/rev, equal to the pitch of the M8 thread.
Straight flute – rigid tap core
A straight flute runs parallel to the axis. It does not carry chips upward because chip evacuation is handled by the chamfer. This allows shallower flutes and a thicker core than in a spiral flute tap. The thicker core withstands torque better, making the tap less likely to break during machine operation.
Form B chamfer – smooth entry and full threads at the exit
The chamfer is the tapered lead of the tap that removes material gradually. Form B has 3.5–5.5 tapered threads, equivalent to 4.4–6.9 mm, since each thread represents a pitch of 1.25 mm. The load is distributed over more cutting edges than with the short form C chamfer. For full threads to reach the end of the hole, the entire chamfer must pass below the workpiece.
DIN 371 shank and machine mounting
Reinforced 8 mm shank with 6.2 mm square
DIN 371 specifies machine taps with a reinforced shank. For M8, the shank diameter is 8 mm, the same as the thread diameter. There is a reduced neck between the thread and the shank, and the length from the tip to the shank is 35 mm. The 6.2 mm square at the end of the shank transmits torque from the holder to the tap.
Mount the tap in a tapping chuck with a 6.2 mm square socket or in a tap collet. On a drill press or machine tool without rigid tapping, use a chuck with axial compensation. It compensates for the difference between the machine feed and the thread pitch, preventing the threads from being stretched or compressed.
▲
Clearance is required below the hole
The chamfer extends approximately 7 mm below the workpiece, and chips fall behind it. A table, vise, or spacer below the hole will trap chips in the thread and may break the tap.
Cutting data and tap drill hole for M8
Cutting speed, spindle speed, and feed for HSSE steel
These values apply to an uncoated HSSE tap with abundant lubrication. Spindle speed and feed were calculated for a diameter of 8 mm. The feed per revolution always equals the thread pitch, which is 1.25 mm.
| Workpiece material | Cutting speed [m/min] | Spindle speed [rpm] | Feed [mm/min] |
|---|---|---|---|
| PLow-carbon steel up to 500 MPa | 10–15 | 400–600 | 500–750 |
| PMedium-carbon steel 500–700 MPa, e.g., C45 | 8–12 | 320–480 | 400–600 |
| PAlloy steel 700–1000 MPa | 6–10 | 240–400 | 300–500 |
| MAustenitic stainless steel 304, 316 | 4–8 | 160–320 | 200–400 |
| KGray cast iron, e.g., EN-GJL-250 | 10–18 | 400–720 | 500–900 |
| NWrought aluminum | 20–40 | 800–1590 | 1000–1990 |
Spindle speed = 1000 × 12 m/min ÷ (3.14 × 8 mm) ≈ 477 rpm; feed = 477 rpm × 1.25 mm ≈ 597 mm/min
12 m/min is the cutting speed at the midpoint of the range for C45 steel. 8 mm is the tap diameter, and 1000 converts meters to millimeters. 1.25 mm is the pitch of the M8 thread — the distance the tap advances into the hole per revolution. Set approximately 480 rpm and a feed of approximately 600 mm/min.
M8 thread in a through hole step by step
1Spot drilling
90° center drill
2Drilling
6.8 mm drill bit, drill all the way through
3Tapping
feed 1.25 mm/rev, chamfer passes below the workpiece
✓Inspection
M8 6H gauge
For a 16 mm workpiece, the tap travels approximately 23 mm = thickness 16 mm + chamfer up to 5.5 threads × 1.25 mm.
Suitable materials and hole types
Steel, stainless steel, cast iron, and aluminum
HSSE is high-speed steel with approximately 5% cobalt. Cobalt helps the cutting edge retain its hardness at high cutting temperatures. The tap is suitable for structural steels and C45 steel, and at lower spindle speeds also for 304 and 316 stainless steel. Straight flutes handle the short chips from gray cast iron well. In aluminum and mild steel, the chip breaker on the form B chamfer pushes long chips down the hole.
Lubricate generously with an emulsion at a concentration of 5–10% or tapping oil. For stainless steel, use oil or an emulsion at a concentration of 8–12%.
▲
Through holes only
In a blind hole, chips accumulate at the bottom ahead of the tip, jam the tap, and break the cutting edges. For blind holes, choose a spiral flute tap with a form C chamfer.
M8 machine tap DIN 371 B Varel combines two features needed in a through hole. The form B chamfer chip breaker pushes chips down the hole, while the straight flute leaves a thick, rigid core. The 6H tolerance produces a thread that fits M8 screws with a 6g tolerance. The 6.8 mm drill bit and 1.25 mm/rev feed remain the same for every material.
Questions about tapping M8 through holes
Drill bit, chamfer, and hole type
A 6.8 mm drill bit. This is the thread diameter of 8 mm minus the pitch of 1.25 mm. A hole with a 6H tolerance can range from 6.647 to 6.912 mm, so a 6.8 mm drill bit falls in the middle of this tolerance zone.
B denotes the chamfer form, or tapered lead. The form B chamfer is 3.5–5.5 threads long and is used for through holes. The shorter form C chamfer, 2–3 threads long, is used in blind holes.
A tap with a form B chamfer for through holes has straight flutes and a chip breaker that pushes chips down the hole. A spiral flute tap has helical flutes, like a drill bit, and carries chips upward out of a blind hole.
By the full chamfer length, up to approximately 7 mm, since 5.5 threads × 1.25 mm = 6.9 mm. Only then do full threads reach the bottom edge of the hole.
DIN 371 features a reinforced shank – for M8, the shank diameter equals the thread diameter, 8 mm. DIN 376 features a shank smaller than the thread diameter. A practical rule: coarse threads up to M10 – DIN 371, from M12 – DIN 376.
Product accessories


Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you




Viewed products


This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.