








Description
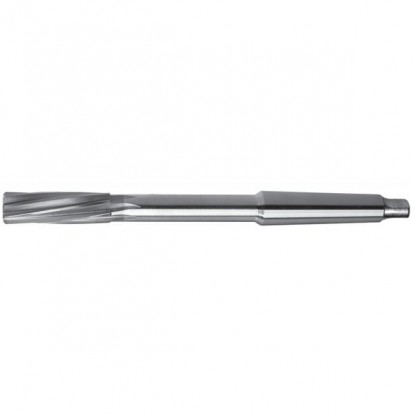
NRTc — shank-type finishing reamer, Morse taper shank, HSS DIN 208
| Technical Data | |
|---|---|
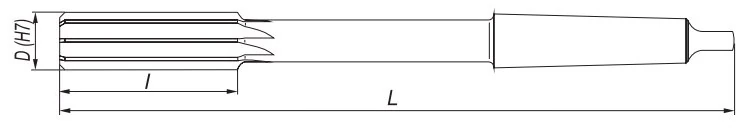
| Cutting diameter D | Ø17 H7 (17.000–17.018 mm) |
| Morse taper | MT2 |
| Flute length l | 54 mm |
| Overall length L | 214 mm |
| Number of teeth Z | 8 |
| Type | NRTc — shank-type finishing reamer, Morse taper shank |
| Dimensional standard | DIN 208 |
| Material | HSS (high-speed steel) |
| Class | Deviations [mm] | Dimension [mm] | |
|---|---|---|---|
| H6 | +0.011 / 0 | 17.000 – 17.011 | |
| H7 | +0.018 / 0 | 17.000 – 17.018 | SELECTED |
| H8 | +0.027 / 0 | 17.000 – 17.027 | |
| H9 | +0.043 / 0 | 17.000 – 17.043 |
The reamed hole falls within the tolerance zone 17.000–17.018 mm (ISO 286-2) — an accuracy level typical of dowel pin holes and sliding fits, among other applications.
Indicative values Ø17 mm Z = 8
| Material group (ISO 513) | Vc [m/min] | fz [mm/tooth] | n [rpm] Ø17 | f [mm/min] Z=8 |
|---|---|---|---|---|
| PStructural and carbon steel | 8–10 | 0.16–0.20 | 150 | 192 |
| MStainless steel | 2–3 | 0.16–0.20 | 37 | 47 |
| KCast iron | 3–5 | 0.16–0.20 | 56 | 72 |
| NAluminum and light alloys | 12–16 | 0.20–0.24 | 225 | 360 |
Vc — cutting speed, fz — feed per tooth (catalog values for HSS, selected for a diameter of Ø17 mm). Spindle speeds were calculated for the lower end of the range: n = (Vc × 1000) ÷ (π × D), feed rate per minute f = fz × Z × n for Z = 8. Start with the lower values and adjust according to the material and clamping rigidity. For an HSS reamer, the cutting parameters can be increased by approx. 25% compared with HSS.
You may also need: Cutting parameters calculator
Hole finishing to H7 tolerance
Machine reamer Ø17 H7 for metal with a taper shank Morse MT2 — NRTc shank-type finishing reamer according to DIN 208 made of high-speed steel (HSS) HSS (approx. 5% Co). The taper shank provides secure, concentric mounting directly in the spindle socket or in a reduction sleeve — from lathes and milling machines to CNC machining centers. The tool has a ~45° lead-in chamfer at the tip for centered entry, while the guiding margins on the cutting edges keep the tool aligned with the hole axis.
The Morse taper shank reamer Ø17 H7 for metal removes the allowance left after drilling and brings the hole to its final size within the tolerance zone H7 (17.000–17.018 mm). Reaming straightens the hole axis, improves roundness and cylindricity, and reduces surface roughness to approx. Ra 0.4–1.6 µm. 8 unequally spaced cutting edges reduce vibration and machining marks. This diameter range is commonly used for sliding fits: pins, shafts, plain bushings, and dowel pin holes in housings. Suitable for reaming steel, cast iron, and nonferrous metals — HSS retains its hot hardness longer than standard HSS and performs more reliably in stainless steel.
Workpiece materials
Drill a hole Ø16.75 mm — stock allowance of approx. 0.25 mm on the diameter. Too little allowance causes the material to be compressed rather than cut; too much overloads the cutting edges and reduces hole accuracy.
Use a Morse taper reduction sleeve — it allows the reamer to be mounted in a socket with a larger taper number without losing mounting concentricity.
The hole falls within the tolerance zone 17.000–17.018 mm, and surface roughness is approx. Ra 0.4–1.6 µm — this accuracy is sufficient for sliding fits and dowel pin holes.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


