








Net price: €434.21
Description
| Technical data | |
|---|---|
| Nominal diameter d1 mm | M70x1.5 LH |
| Thread pitch P mm | 1.5 mm |
| Overall length l1 | 160 mm |
| Flute length l2 | 41 mm |
| Shank diameter d2 | 50 mm |
| Square drive size a | 39 mm |
| Tap drill diameter | 68.5 mm |
| Thread angle G | 60° |
| Tap tolerance | ISO2 6H |

Division of work in the 1–2 set
The M70x1.5 LH thread is cut into the wall of a hole with a diameter of 68.5 mm. The thread groove extends 0.75 mm into the wall. A single tap would have to cut the entire groove at once — by hand, this means high resistance and a risk of breakage. The set divides this work into two passes.
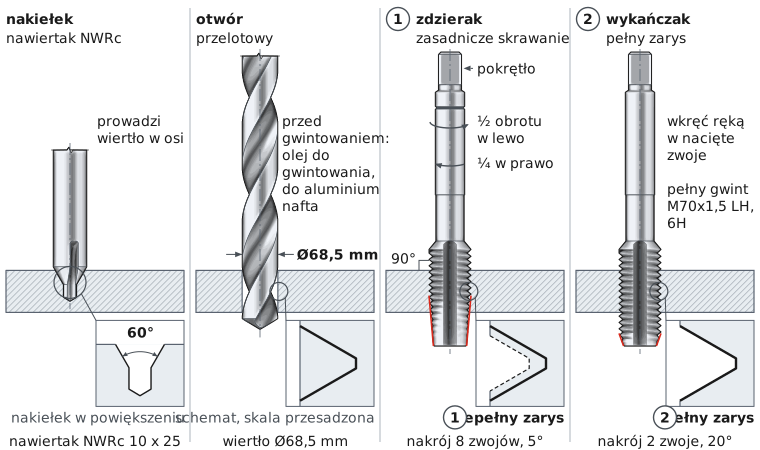
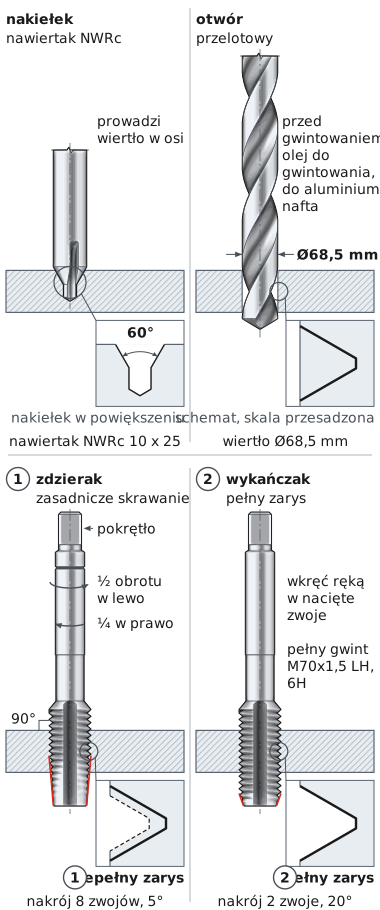
The drawing shows the entire set in operation. Both taps have the same shank and the same length. They differ in their chamfer, the tapered tip: No. 1 has a chamfer spanning 8 threads, while No. 2 spans only 2 threads. The detail windows at the hole wall show how the thread groove deepens after each tap.
| Tap | Chamfer | Chamfer angle | Material removed | How it works in the hole |
|---|---|---|---|---|
| No. 1 – roughing tap | long, 8 threads | 5° | the main portion of the groove | enters smoothly and establishes thread alignment |
| No. 2 – finishing tap | short, 2 threads | 20° | the remainder, to the full profile | follows the cut threads and produces the full 6H profile |
The chamfer on No. 1 is 4 times as long as the chamfer on No. 2 — the difference is immediately visible when you place them side by side. No. 1 has an incomplete thread profile; only No. 2 has the full profile. The number is also indicated on the shank: No. 1 has one ring, No. 2 has none. Keep the set together and always start with the roughing tap.
Hand tapping step by step
Drill bit 68.5 mm
Chamfer 8 threads
Chamfer 2 threads
Tolerance 6H
Turning sequence: half a turn counterclockwise, a quarter turn clockwise | Between taps: remove chips from the hole
Start with the hole. The drill diameter is easy to calculate: thread diameter 70 mm minus pitch 1.5 mm gives 68.5 mm. An undersized hole is a common cause of a tap twisting off in the workpiece.
The set taps both types of holes. In a through hole, the thread extends through the full material thickness. In a blind hole, cut the thread to 175 mm, or 2.5 times the thread diameter (2.5 x 70 mm, shown as 2.5D in the drawing). Drill the hole deeper than the thread. The finishing tap has a chamfer spanning 2 threads, so approx. 2 incomplete threads remain near the bottom. The extra depth below the thread accommodates them along with the chips.
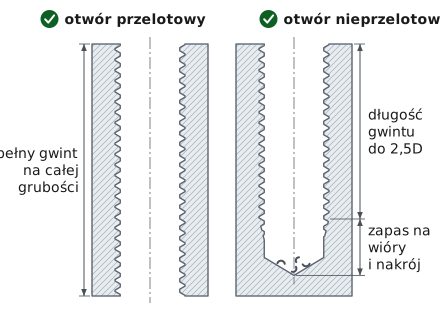
Fit the roughing tap into a tap wrench and position it perpendicular to the surface. Check the angle from two sides, for example with a square. This is a left-hand thread, so turn in the opposite direction to usual: half a turn counterclockwise, then a quarter turn clockwise. Reversing breaks the chip into short pieces — a slight crunch is normal. The first threads determine whether the thread will be straight.
Unscrew the roughing tap and remove chips from the hole. Screw the finishing tap by hand into the cut threads — it should engage them naturally. Continue with the same turning sequence as for the roughing tap. The finishing tap removes the remaining material and cuts the groove to its full profile within 6H tolerance. Once it screws smoothly all the way in, the thread is complete — check it with an M70x1.5 LH screw.
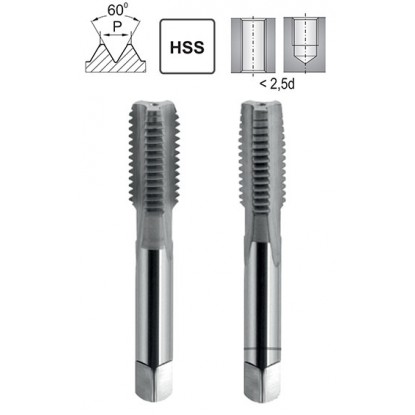
Hand Tap M70x1.5 DIN 2181/2 6H HSS is designed to cut metric fine threads with a diameter of seventy millimeters and a pitch of one and a half millimeters in structural steels and metal alloys with strengths up to eight hundred megapascals. It provides a clean thread profile and high dimensional repeatability in one-off and short-run machining.
Technical data: nominal diameter seventy millimeters; pitch one and a half millimeters; sixty-degree metric profile according to ISO 68-1; hole tolerance zone 6H according to ISO 965; right-hand direction. Straight flutes promote controlled chip evacuation and stable guidance. Precision-manufactured high-speed steel (HSS) maintains edge sharpness and resistance to microchipping. The two-part arrangement according to DIN 2181/2 — starting section (I) and finishing section (II) — balances torsional loads and supports axial alignment. Recommended drill bit: sixty-eight and a half millimeters; lubrication with emulsion or active cutting oil improves surface texture and extends cutting edge life.
Compliance with DIN 2181/2 (construction), ISO 68-1 (profile geometry), and ISO 965 (6H tolerance) ensures compatibility with measuring equipment and stable dimensions. In workshop practice, consistent quality and predictable thread geometry are facilitated by using an M70x1.5 Left-Hand Hand Tap Set, providing a consistent transition between the starting and finishing stages.

The set consists of two taps — a roughing tap and a finishing tap, which guarantee a fully formed thread when used in sequence.
The HSS tool works well in low-carbon steel, aluminum, brass, and other materials with good machinability.
High-speed steel (HSS) provides high durability, abrasion resistance, and stable operation even under demanding conditions.

Reference: 0000008644 In stock < 10 items
€277.01 brutto
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


