






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot

Hand Tap M40X1.5 LH DIN 2181/2 6H HSS
12569
Thread size: M40x1,542 sizes of this tap
€135.95 tax inc.
Net price: €110.53
Description
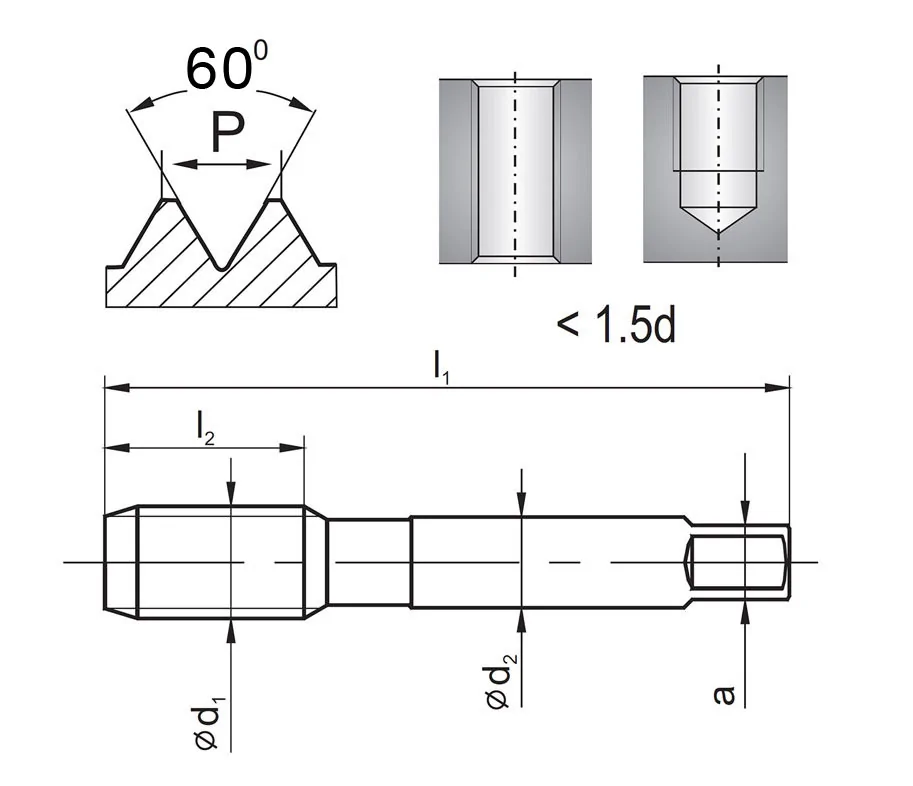
Technical data for the M40x1.5 left-hand hand tap
| Technical data | |
|---|---|
| Nominal diameter d1 mm | M40 |
| Thread pitch P mm | 1.5 mm |
| Overall length l1 | 110 mm |
| Flute length l2 | 25 mm |
| Shank diameter d2 | 32 mm |
| Square drive size a | 24 mm |
| Tap drill diameter | 38.5 mm |
| Thread angle G | 60° |
| Tap tolerance | ISO2 6H |
Roughing tap and finishing tap – how much material each removes
Division of work in the 1–2 set
The M40x1.5 LH thread is cut into the wall of a hole with a diameter of 38.5 mm. The thread groove extends 0.75 mm into the wall. A single tap would have to cut the entire groove at once — by hand, this means high resistance and a risk of breakage. The set divides this work into two passes.
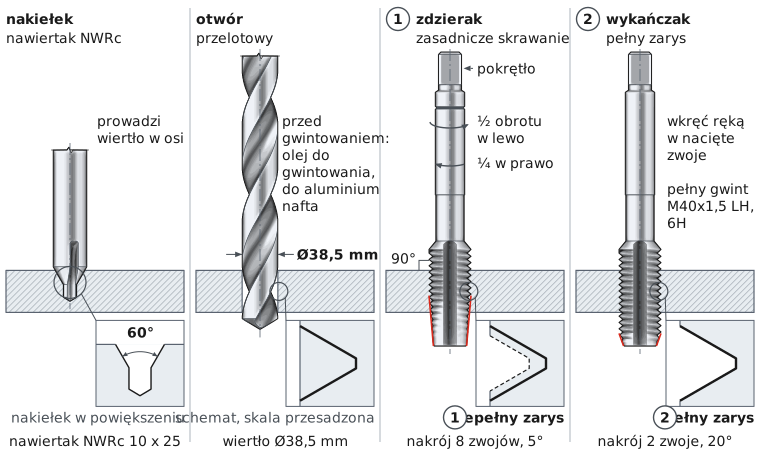
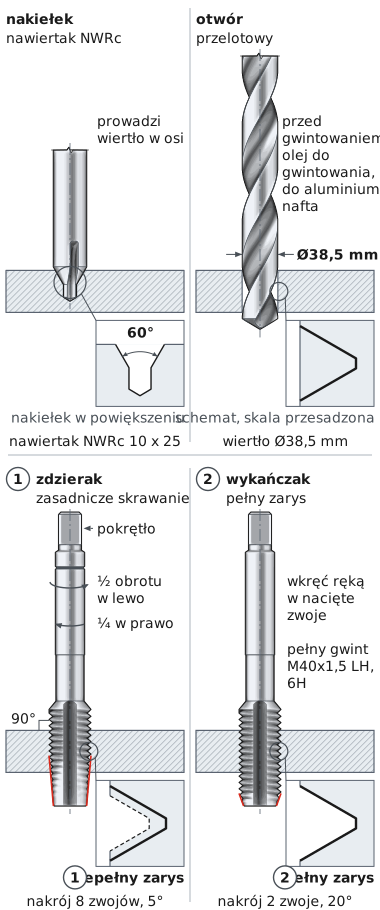
The drawing shows the entire set in operation. Both taps have the same shank and the same length. They differ in their chamfer, the tapered tip: No. 1 has a chamfer spanning 8 threads, while No. 2 spans only 2 threads. The detail windows at the hole wall show how the thread groove deepens after each tap.
| Tap | Chamfer | Chamfer angle | Material removed | How it works in the hole |
|---|---|---|---|---|
| No. 1 – roughing tap | long, 8 threads | 5° | the main portion of the groove | enters smoothly and establishes thread alignment |
| No. 2 – finishing tap | short, 2 threads | 20° | the remainder, to the full profile | follows the cut threads and produces the full 6H profile |
How to distinguish the taps in the set
The chamfer on No. 1 is 4 times as long as the chamfer on No. 2 — the difference is immediately visible when you place them side by side. No. 1 has an incomplete thread profile; only No. 2 has the full profile. The number is also indicated on the shank: No. 1 has one ring, No. 2 has none. Keep the set together and always start with the roughing tap.
How to tap an M40x1.5 LH hole – sequence 1, 2
Hand tapping step by step
Thread M40x1.5 LH in four steps
ØDrilling
Drill bit 38.5 mm
1Roughing tap
Chamfer 8 threads
2Finishing tap
Chamfer 2 threads
✓Finished thread
Tolerance 6H
Turning sequence: half a turn counterclockwise, a quarter turn clockwise | Between taps: remove chips from the hole
Start with the hole. The drill diameter is easy to calculate: thread diameter 40 mm minus pitch 1.5 mm gives 38.5 mm. An undersized hole is a common cause of a tap twisting off in the workpiece.
Through hole or blind hole – how deep to drill
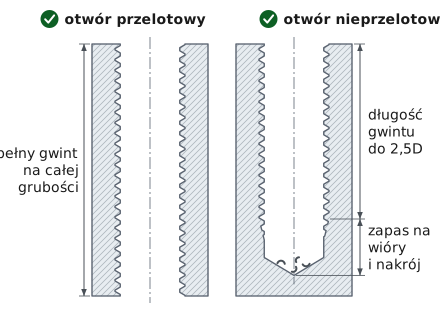
The set taps both types of holes. In a through hole, the thread extends through the full material thickness. In a blind hole, cut the thread to 100 mm, or 2.5 times the thread diameter (2.5 x 40 mm, shown as 2.5D in the drawing). Drill the hole deeper than the thread. The finishing tap has a chamfer spanning 2 threads, so approx. 2 incomplete threads remain near the bottom. The extra depth below the thread accommodates them along with the chips.
No. 1 – the roughing tap establishes thread alignment
Fit the roughing tap into a tap wrench and position it perpendicular to the surface. Check the angle from two sides, for example with a square. This is a left-hand thread, so turn in the opposite direction to usual: half a turn counterclockwise, then a quarter turn clockwise. Reversing breaks the chip into short pieces — a slight crunch is normal. The first threads determine whether the thread will be straight.
No. 2 – the finishing tap produces the full profile
Unscrew the roughing tap and remove chips from the hole. Screw the finishing tap by hand into the cut threads — it should engage them naturally. Continue with the same turning sequence as for the roughing tap. The finishing tap removes the remaining material and cuts the groove to its full profile within 6H tolerance. Once it screws smoothly all the way in, the thread is complete — check it with an M40x1.5 LH screw.
M40x1.5 left-hand metric fine hand taps
Set of two high-quality general-purpose hand taps for cutting metric fine threads, type M40x1.5 LH with a 60° angle, compliant with ISO DIN-13. The taps are suitable for tapping through and blind holes. Designed for machining components made of materials designated P1.2 – P1.3 (unalloyed steels, metals, nonferrous metals, metal alloys, and plastics).
Our fine-thread hand taps are manufactured according to ISO 529 from modern high-speed steel (HSS). This special tool steel increases tapping efficiency and precision. The tolerance class of the threads produced is ISO2 (6H). The taps also offer durability under demanding operating conditions and cutting edges resistant to mechanical damage. The taps are intended for both hobbyists and professional companies and metalworking shops.
Product accessories


Metal drill bit 38.5 NWKc HSS DIN 345 Werko
Reference: 0423 In stock > 10 items
€65.79
€80.92 brutto


Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you






This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.