







Description
| Technical data | |
|---|---|
| Side length l | 12.9 mm |
| Insert thickness s | 4.76 mm |
| Hole diameter d1 | 5.16 mm |
| Corner radius rε | 0.8 mm |
| ANSI code | CNMG 432 |
finishing, semi-finishing, and roughing — ISO groups K and H
| Material | Finishing | Semi-finishing | Roughing | ||||||
|---|---|---|---|---|---|---|---|---|---|
| Vc [m/min] | Feed f [mm/rev] | ap [mm] | Vc [m/min] | Feed f [mm/rev] | ap [mm] | Vc [m/min] | Feed f [mm/rev] | ap [mm] | |
| KCast iron | 240-400 | 0.1 | 0.5 | 155-280 | 0.25 | 2.5 | 120-200 | 0.4 | 5 |
| HHardened materials | 80-150 | 0.08 | 0.2 | 40-90 | 0.15 | 0.8 | 30-60 | 0.25 | 1.5 |
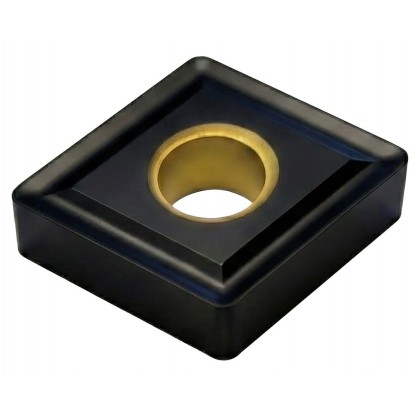
double-sided 80° diamond with a hole and chip breaker
The CNMG 120408 turning insert is a double-sided, rhombic indexable insert made of grade H5115 cemented carbide, designed for turning cast iron. The C shape, a rhombus with a 80° corner angle, combines a rigid, strong corner with the ability to perform longitudinal turning and facing using one tool. The negative geometry with a 0° clearance angle allows both sides of the insert to be used — a total of four cutting edges. The nose radius rε of 0.8 mm provides a balance between surface finish and edge strength at feed rates of 0.25–0.4 mm/rev.
The CNMG 120408 insert (also written without a space as cnmg120408) is suitable for precision external turning and boring of iron castings — gray, ductile, and malleable cast iron. The wear-resistant CVD coating allows high cutting speeds, reaching approximately 400 m/min when finishing cast iron. Calculate spindle speed using n = 1000·Vc/(π·D): for a shaft with a diameter of 50 mm at Vc = 300 m/min, the result is approximately 1910 rpm. Grade H5115 indexable inserts are supplied by the Korean brand Horn.
The 80° rhombic shape provides a compromise between corner strength and versatility — stronger than a triangle, while allowing longitudinal turning and facing without changing the turning tool. The hole with a chip breaker on both sides (type G according to ISO 1832) controls chip flow and breaking on both sides of the insert. Short, brittle cast iron chips work well with the type G chip breaker, making it easier to evacuate chips from the cutting zone. Tolerance class M ensures repeatable edge positioning after indexing the insert in the holder pocket. When machining more ductile nodular cast iron, maintain a stable feed rate and rigid clamping to reduce corner chipping. Grade H5115 carbide also handles hardened materials at appropriately reduced cutting speeds.
Grade H5115 with a CVD coating is optimized for cast iron and continuous turning. When machining austenitic stainless steel or making heavily interrupted cuts, select a grade dedicated to ISO group M or P — CVD withstands edge impacts less effectively than coatings PVD.
how to read the CNMG 120408 code — positions 1–7 of the designation
Designation CNMG 120408 according to the standard ISO 1832: 4 letters describe geometry and construction, 3 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
holders with a 12 diamond-shaped pocket — external and internal turning
use, turning tool selection, and turning parameters
Four — the diamond has 2 corners per side, and the negative geometry (0° clearance angle) allows both sides of the insert to be used. Once an edge becomes dull, simply rotate the insert in its pocket without changing the holder.
Holders with a 12 diamond-shaped pocket (IC 12.7 mm): for external turning TCLNR/L and PCLNR/L (entering angle 95°), PCBNR/L and TCKNR/L (75°) and PCMNN, TCMNN and TCZNN with cross sections of 16×16–32×32 mm; for internal turning, boring bars S20R–S50V with a TCLNR/L or PCLNR/L head.
Only in corner radius: 0.4 mm is used for finishing at low feed rates, 0.8 mm is the general-purpose version, and 1.2 mm is selected for roughing at feed rates up to 0.4–0.5 mm/rev. The other dimensions (IC 12.7 mm, thickness 4.76 mm) are identical.
Yes — grade H5115 covers group ISO K: gray, ductile, and malleable cast iron. The CVD coating allows cutting speeds of up to approximately 400 m/min when finishing; maintain a stable feed rate and rigid clamping to reduce corner chipping.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


