






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot

Description
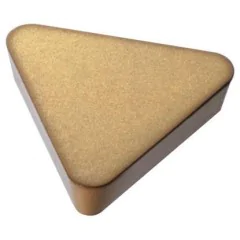
SPKN 1504 milling insert – 75° square for face milling
| Technical data | |
|---|---|
| Side length l | 15.88 mm |
| Insert thickness s | 4.76 mm |
| Shape | square (S) |
| Entering angle κ | 75° |
| Version | R — right-hand |
| Hole / chip breaker | none (clamp mounting) |
| Grade | SM25T (P15-P40 / M25-M35) |
| ANSI code | SPKN 53 |

SM25T indexable insert – milling data for steel and stainless steel
face milling with a 75° milling head — conservative ranges according to ISO 513 (face milling table); for uncoated SM25T, select the lower part of the range
| Material | Vc [m/min] | Feed per tooth fz [mm/tooth] | ap [mm] | ae [% D] |
|---|---|---|---|---|
| PSteel, cast steel | 150-220 | 0.10-0.22 | 0.5-3.0 | 60-80 |
| MStainless steel | 80-140 | 0.08-0.18 | 0.3-2.0 | 50-70 |
SM25T cemented carbide insert – design and applications
square insert without a hole, with a wiper edge, secured by a clamp
The SPKN 1504 milling insert is a square, single-sided cemented carbide indexable insert designed for face milling steel, cast steel, and stainless steel. The square shape provides four cutting edges per insert, and the seventy-five° entering angle thins the chip and softens entry into the material. The design is positive, with an eleven° clearance angle, without a hole or chip breaker — the insert is secured in the milling head pocket by a top clamp or wedge. A ground wiper edge runs along the corner, smoothing the bottom surface after face milling. SM25T grade is an uncoated carbide with increased resistance to dynamic fatigue loads, producing discontinuous chips with large, variable cross sections. The body dimensions — side length 15.88 mm and thickness 4.76 mm — correspond to the inch-based ANSI SPKN 53 code.
Key benefits of the SPKN 1504 milling insert
- Four cutting edges — the square shape provides 4 usable corners; once dull, simply index the insert in the milling head pocket.
- 75° entering angle — thins the chip and softens entry into the material, increasing corner life during face milling.
- SM25T grade for ISO P and M groups — uncoated carbide for P15-P40 steel and M25-M35 stainless steel.
- The ground wiper edge at the corner improves the finish of the bottom surface after face milling.
- The 11° positive geometry reduces forces and power consumption at large uncut chip cross sections.
- The design without a hole, secured by a clamp or wedge, simplifies insert replacement in the milling head.
Square insert applications and cutting data selection
The SPKN 1504 EDR SM25T insert is suitable for face milling castings, welds, and datum surfaces in difficult-to-machine materials. It performs best where high and medium cutting speeds and large uncut chip cross sections are required. Calculate milling head speed using n = 1000·Vc/(π·D): a milling head diameter of 80 mm at a cutting speed of 120 m/min gives approximately 477 rpm. Calculate the table feed rate using vf = fz·z·n — with six inserts and a feed per tooth (fz) of 0.15 mm, this gives approximately 429 mm/min.
However, the ground wiper edge imposes a condition: feed per revolution should not exceed sixty percent of its width; otherwise, the wiper stops smoothing the surface. As an uncoated carbide, SM25T grade performs best in stable, continuous cutting without vibration. Interrupted entries and hard casting skin reduce its tool life faster than that of coated grades. The square profile with four corners allows the insert to be indexed to the next edge once dull, without removing the holder from the spindle.
▲
Application limitation
Grade SM25T is a carbide uncoated — it is not designed for interrupted cutting on hard casting skin or for hardened materials. For cast iron and nonferrous metals (ISO K/N groups), select a dedicated grade, e.g. H10.
Square insert designation decoder according to ISO 1832
how to read the SPKN 1504 EDR code — positions 1–9 of the designation
Designation SPKN 1504 EDR according to the standard ISO 1832: 4 letters describe the geometry and construction, 2 numeric codes describe the dimensions, and the suffix EDR — the wiper edge geometry. Each field has a number, an icon and a brief description.
ISO 1832 designation decoder — how to read the code
1Sshape 2Pangle α 3Ktolerance 4Ntype – 515size 604thickness – 7Eangle κ 8Dland α′ 9Rhand
Positions 1–3 · ISO code
1SShape
Square 90°
4 corners of 90° per side
2PClearance angle
α = 11°
positive, single-sided
3KTolerance
Class K (precision)
ground thickness ±0.025 mm
Positions 4–6
4NType
Without hole or chip breaker
clamp or wedge mounting
515Size
l = 15.88 mm
IC = 15.88 mm (square: IC = l)
604Thickness
s = 4.76 mm
between rake faces
EDR suffix · wiper edge
7EEntering angle
κ = 75°
75° face milling heads
8DWiper land
α′ = 15°
wiper land clearance angle
9RHand
Right-hand
standard clockwise spindle rotation
✓ 4 corners × 1 side = 4 cutting edges
Full designation: SPKN 1504 EDR = 90° square · 11° positive · class K · without a hole or chip breaker · IC 15.88 mm (l 15.88 mm) · s 4.76 mm · κ 75° · 15° wiper land · right-hand (R)
75° milling heads for the SPKN 1504 insert
pockets for inserts without a hole, secured by a top clamp
| Holder / milling head | Compatible |
|---|---|
| 75° face milling heads (e.g. FWT 75°, Darmet FB75SP15) | ✓ yes — SPKN pocket, top clamp |
| 90° angle milling cutters and heads (TPKN pockets) | ✗ no — different entering angle and pocket shape |
| Pockets for inserts with a hole (APKT / SEKT) | ✗ no — SPKN has no hole, clamp mounting only |
Frequently asked questions about the SPKN 1504 insert
mounting, milling head selection, and milling parameters
Four — a square has 4 corners, and the positive, single-sided geometry with a 11° clearance angle means the insert cuts only with its top face. Once a corner is dull, index the insert in the milling head pocket to the next edge without replacing the holder.
Face milling heads with an entering angle of 75°, e.g. FWT 75° or Darmet FB75SP15. The insert has no hole, so it is secured with a top clamp or wedge. The 90° milling heads use TPKN inserts and are not compatible with SPKN inserts.
SM25T is uncoated cemented carbide from Baildonit, corresponding to groups ISO P15-P40 (steel, cast steel) and M25-M35 (stainless steel). It withstands varying chip cross sections and dynamic loads at high and medium cutting speeds.
Keep the feed per revolution below 60% the width of the wiper edge at the corner. Above this value, the wiper no longer smooths the machined floor. Calculate rotational speed and feed rate using n = 1000·Vc/(π·D) and vf = fz·z·n.
Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you


Viewed products


This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.