







Net price: €3.16
Description
| Technical data | |
|---|---|
| Side length l | 15.00 mm |
| Insert thickness s | 5.5 mm |
| Corner radius rε | 2.0 mm |
| Shape | Rectangular 85° (parallelogram) |
| Clearance angle | 15° (positive) |
| Grade | IC328 (coated) |
| Application | steel, stainless steel (ISO P/M) |
right-angle shoulder and profile milling — ISO groups P and M
| Material | vc [m/min] | fz [mm/tooth] | ap [mm] | ae [% D] |
|---|---|---|---|---|
| PSteel | 130-200 | 0.10-0.20 | 1.0-4.0 | 30-70 |
| MStainless steel | 70-130 | 0.06-0.15 | 0.5-2.0 | 25-60 |
rectangular 85° with a large corner radius for profile milling
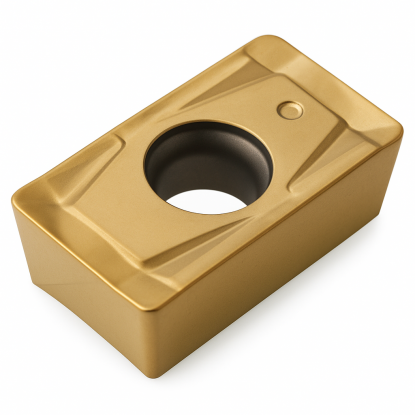
The ADKT 150520 milling insert is an indexable cemented carbide insert in coated grade IC328, designed for indexable milling cutters and milling heads operating at a right angle. Shape A, a parallelogram with a 85° corner angle, combined with a large 2.0 mm corner radius, makes the insert suitable for high-performance profile and contour milling. The positive 15° clearance angle reduces cutting resistance and enables smoother milling head operation, even on machines with moderate power. The countersunk hole and single-sided chip breaker (type T according to ISO 1832) control chip evacuation when machining with one side of the insert. Coated grade IC328 covers ISO P and M groups, so one insert handles both steel and stainless steel.
The ADKT 150520 indexable insert performs well in shoulder, pocket, and profile milling in structural steel, alloy steel, and stainless steel. Calculate spindle speed using n = 1000·vc/(π·D): for a milling head with a diameter of 63 mm at a cutting speed of vc = 160 m/min, the result is approximately 808 rpm. With five inserts in the milling head and a feed per tooth of fz = 0.15 mm, this gives a table feed rate of approximately 606 mm/min. The abbreviation fz denotes the feed per cutting edge during one revolution of the milling head.
The large corner radius distributes the load over a longer section of the edge and improves the finish of the profile floor, but increases radial forces. For this reason, mount the milling head rigidly and select a depth of cut that does not exceed the active cutting edge length. For stainless steel, maintain a constant feed and continuous cooling, as some stainless steels dissipate heat poorly and work-harden when cutting is too slow. Climb milling on a CNC machine with table backlash eliminated extends edge life and reduces vibration.
Coated grade IC328 is intended for groups ISO P and ISO M. For other material groups, select a grade approved by the tool manufacturer. The large corner radius 2.0 mm increases radial forces and requires rigid mounting of the milling head.
how to read the ADKT 150520 code — positions 1–7 of the designation
Designation ADKT 150520 according to the standard ISO 1832: 4 letters describe geometry and construction, 3 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
ISO 1832 designation decoder — how to read the code
Positions 1–4 · ISO code
1AShape
Parallelogram 85°
2 corners of 85° per side
2DClearance angle
α = 15°
positive, single-sided
3KTolerance
Class K (precision)
ground thickness ±0.025 mm
4TType
Countersunk hole + chip breaker
countersink 40–60°, single-sided chip breaker
Positions 5–7 · dimensions [mm]
515Edge length
l = 15 mm
code 15 → edge length
605Thickness
s = 5.56 mm
between rake faces
720Corner radius
rε = 2 mm
code ÷ 10 → radius in mm
✓ 2 corners × 1 side = 2 cutting edges
pocket for ADKT 150520 — 90° shoulder, pocket, and profile milling
Applications and compatibility:
| Rating | Tool, material or application |
|---|---|
| ✔ | Milling heads and indexable milling cutters with a pocket designed for the insert ADKT 150520 |
| ✔ | Milling heads and indexable milling cutters operating at a right angle (90°) with a pocket for shape A (85° rectangle) |
| ✔ | Right-angle shoulder and straight-wall milling, as well as profile and contour milling |
| ✔ | Structural and alloy steel (ISO P) and stainless steel (ISO M) |
| ✗ | Other material groups — require a grade confirmed by the manufacturer |
| ✗ | APKT inserts and inserts of other shapes (e.g., SEKT) — require different pocket geometry |
number of edges, materials, differences, and dimensions
Two — the 85° rectangle provides 2 corners for cutting, and the positive geometry with a clearance angle of 15° makes the insert single-sided, cutting only with its top face. Once a corner is worn, rotate the insert in its pocket to the next edge without replacing the milling head.
Coated grade IC328 covers steel in group ISO P and stainless steel in group ISO M. For steel, maintain a cutting speed of 130–200 m/min, for stainless steel 70–130 m/min with a constant feed and continuous cooling.
Both shapes are rectangular 85° for milling heads operating at a right angle, and they differ in clearance angle: ADKT has an angle of 15° (letter D), while APKT an angle of 11° (letter P). The inserts must not be interchanged in the same milling head pocket.
The corner radius rε is 2.0 mm (code 20 in the ISO 1832 designation), the insert thickness s is 5.5 mm, and the side length l is — 15.00 mm. The large radius and thick body make the insert suitable for productive profile milling.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


