









Net price: €8.42
Description
| Technical data | |
|---|---|
| Shape | Square (S) |
| Side length l | 12.70 mm |
| Insert thickness s | 3.18 mm |
| Dimension m | 0.90 mm |
| Entering angle κ | 75° |
| Cutting direction | right-hand (R) |
| ANSI code | SPKN 42 |
| Grade | YG612 (YG-1) |
face milling — indicative family ranges according to ISO 513, by analogy with face mills
| Material | Vc [m/min] | Feed fz [mm/tooth] | Depth ap [mm] | Width ae [% D] |
|---|---|---|---|---|
| PSteel, cast steel | 150-220 | 0.10-0.22 | 0.5-3.0 | 60-80 |
single-sided, positive, without a hole, with a wiper edge at the corner
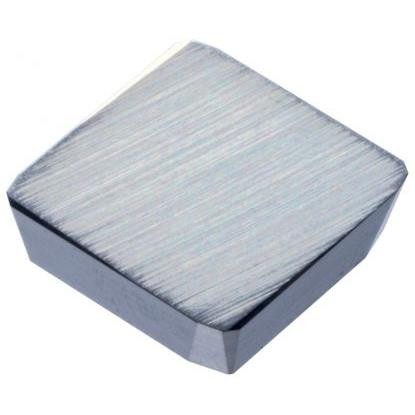
The SPKN 1203 EDTR milling insert is a single-sided, square indexable insert made of grade YG612 cemented carbide from the Korean company YG-1. Its four corners operate at an entering angle of seventy-five°, making the insert suitable for face mills. The design is positive, with an eleven° clearance angle, and has no hole or chip breaker. It is secured in the milling head pocket with a wedge or top clamp. A ground wiper land at each corner smooths the bottom of the path left by the milling cutter. This design originates from ISO 3365 and GOST standards, widely used in Polish machine shops. Grade YG612 from YG-1 is intended for machining steel and cast steel at increased cutting parameters.
The square profile and wiper land make the SPKN 1203 insert suitable for face milling flat surfaces on conventional milling machines and CNC machine tools. For the land to smooth the surface effectively, the feed per revolution of the milling head should not exceed sixty percent of the wiper edge width. Manufacturer YG-1 does not specify this width in the available description, so it must be confirmed in the insert data sheet. Then calculate the limit using f_rev,max = 0.6·b_s and divide it by the number of active cutting edges to determine the feed per tooth.
The indexable insert performs well when machining structural steel and cast steel. Calculate spindle speed using n = 1000·Vc/(π·D): for a milling head with a diameter of 63 mm at a cutting speed of 180 m/min, the result is approximately 910 rpm. Use climb milling when table backlash has been eliminated, as the cutting edge then enters at the thicker part of the chip and stays sharp longer. For cast steel, reduce the cutting speed to the lower end of the range to limit abrasive wear on the edge. Emulsion cooling maintains consistent chip evacuation when face milling larger surfaces.
Insert SPKN 1203 works only in face mills with an entering angle of 75° — it does not fit 90° shoulder milling heads, which require inserts TPKN, or 45° face mills for inserts SEKN/SEAN/SEKR.
how to read the SPKN 1203 EDTR code — positions 1–10 of the designation
Designation SPKN 1203 EDTR according to the standard ISO 1832: 4 letters describe the geometry and construction, 2 numeric codes describe the dimensions, and the suffix EDTR — the wiper edge geometry. Each field has a number, an icon and a brief description.
ISO 1832 designation decoder — how to read the code
Positions 1–3 · ISO code
1SShape
Square 90°
4 corners of 90° per side
2PClearance angle
α = 11°
positive, single-sided
3KTolerance
Class K (precision)
ground thickness ±0.025 mm
Positions 4–6
4NType
Without hole or chip breaker
clamp or wedge mounting
512Size
l = 12.7 mm
IC = 12.7 mm (square: IC = l)
603Thickness
s = 3.18 mm
between rake faces
EDTR suffix · wiper edge
7EEntering angle
κ = 75°
75° face milling heads
8DWiper land
α′ = 15°
wiper land clearance angle
9TEdge condition
Chamfered (T-land)
the chamfer strengthens the edge during roughing
10RHand
Right-hand
standard clockwise spindle rotation
✓ 4 corners × 1 side = 4 cutting edges
SPKN 1203 pocket — face mills with an entering angle of 75°
| Milling head / holder type | Angle κ | SPKN 1203 insert |
|---|---|---|
| FWT 75° face mill | 75° | ✔ compatible |
| Darmet FB75SP15 milling head | 75° | ✔ compatible |
| 90° shoulder milling head | 90° | ✗ requires TPKN |
| 45° face mill | 45° | ✗ requires SEKN/SEAN/SEKR |
geometry, milling head selection, and face milling parameters
Four — a square has 4 corners, and the positive, single-sided geometry means the insert cuts only with its top face. Once a corner wears out, rotate the insert in its pocket to the next edge without replacing the entire milling head.
For face mills with an entering angle of 75°, for example FWT 75° or Darmet FB75SP15. It does not fit shoulder milling heads 90° (which require TPKN inserts) or face mills 45° (SEKN/SEAN/SEKR).
E = corner entering angle 75°, D = wiper land clearance angle 15°, T = chamfered edge (T-land), R = right-hand version.
The feed per revolution of the milling head should not exceed 60% the width of the wiper edge. The land width must be confirmed in the YG-1 data sheet, as it is not specified in the available description. Calculate the limit as f_rev,max = 0.6·b_s, then divide the result by the number of active cutting edges.

Reference: 0000003728 In stock < 10 items
€106.82 brutto
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


