





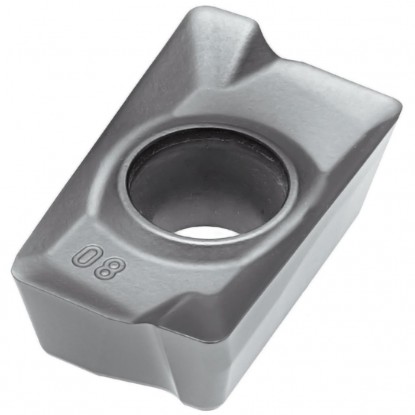


Net price: €3.16
Description
| Technical data | |
|---|---|
| Shape | Rectangular 85° (A) |
| Clearance angle | 11° (P) — positive |
| Tolerance | Class K (±0.025 mm) |
| Side length l | 11 mm |
| Insert thickness s | 3.5 mm |
| Corner radius rε | 0.5 mm |
| PDER code | proprietary code; meaning per the product data sheet |
| H2 suffix | proprietary code — not interpreted |
| Cutting edges | 2 (single-sided) |
| The | PVD |
| Grade | H6310 (P20-P40 / M20-M40) |
shoulder and pocket milling with a 90° milling head — ISO P and M groups
| Workpiece material | ISO group | vc [m/min] | fz [mm/tooth] | ap [mm] |
|---|---|---|---|---|
| PStructural steel | P20-P40 | 130-200 | 0.10-0.20 | 1-4 |
| MStainless steel | M20-M40 | 70-130 | 0.06-0.15 | 0.5-2 |
single-sided 85° rectangle with PVD coating for 90° shoulder milling heads
The APKT 113505 milling insert is a single-sided, rectangular indexable insert made of cemented carbide in grade H6310, designed for milling steel and stainless steel. Shape A, a rectangle with a corner angle of 85°, and the positive clearance angle of 11° reduce cutting forces and facilitate smooth cutting edge entry in interrupted cuts. PDER and H2 are proprietary codes whose meaning should not be interpreted without the manufacturer's data sheet. The insert is suitable for milling pockets, shoulders and vertical walls. The PVD (physical vapor deposition) coating increases edge hardness and abrasion resistance. The two cutting edges can be used in sequence by rotating the insert in the milling head pocket.
The APKT indexable insert is used for finish milling low-carbon steels, structural steels and stainless steels, as well as surface-hardened materials that tend to adhere. Calculate the spindle speed using n = 1000·vc/(π·D). For a milling head with a diameter of 50 mm at a cutting speed of 160 m/min, the result is approximately 1019 rpm. Select a feed per tooth (fz) of 0.10–0.20 mm for steel and 0.06–0.15 mm for stainless steel to limit work hardening of the layer being cut. The PVD coating withstands the thermal shocks of interrupted cutting typical of stainless steel milling.
Class K tolerance ensures uniform thickness of all inserts in the milling head, resulting in a smooth surface in face and shoulder milling. The positive, single-sided design limits the number of edges to two but reduces cutting resistance. This is an advantage on lower-power machine tools and with slender tools with long overhangs. Keep the depth of cut (ap) within 1–4 mm for steel and 0.5–2 mm for stainless steel. Use climb milling on CNC machines with table backlash eliminated to extend cutting edge life. Milling inserts in grade H6310 are supplied by the Korean brand Horn.
Grade H6310 is not intended for steels hardened above 45 HRC — for hard machining, select a milling insert with a cubic boron nitride (CBN) cutting edge.
how to read the APKT 113505 PDER code — positions 1–10 of the designation
Designation APKT 113505 PDER according to the standard ISO 1832: 4 letters describe the geometry and construction, 2 numeric codes describe the dimensions, and the suffix PDER — the wiper edge geometry. Each field has a number, an icon and a brief description.
ISO 1832 designation decoder — how to read the code
Positions 1–4 · ISO code
1AShape
Parallelogram 85°
2 corners of 85° per side
2PClearance angle
α = 11°
positive, single-sided
3KTolerance
Class K (precision)
ground thickness ±0.025 mm
4TType
Countersunk hole + chip breaker
countersink 40–60°, single-sided chip breaker
Positions 5–7 · dimensions [mm]
511Edge length
l = 11 mm
code 11 → edge length
635Thickness
s = 3.5 mm
between rake faces
705Corner radius
rε = 0.5 mm
code ÷ 10 → radius in mm
PDER suffix · wiper edge
7PEntering angle
κ = 90°
90° angle milling cutters and milling heads
8DWiper land
α′ = 15°
wiper land clearance angle
9EEdge condition
Rounded (honed)
greater resistance to chipping
10RHand
Right-hand
standard clockwise spindle rotation
✓ 2 corners × 1 side = 2 cutting edges
90° milling heads (shoulder milling) — machining steel and stainless steel
Suitable applications:
| Rating | Application |
|---|---|
| ✓ | Shoulder and step milling (shoulder milling) with a milling head with a 90° entering angle |
| ✓ | Milling pockets with a straight, vertical side wall |
| ✓ | Finish machining of low-carbon and structural steels — ISO P group |
| ✓ | Machining stainless steels and surface-hardened materials — ISO M group |
| ✓ | Use on conventional machine tools and CNC machining centers |
| ✗ | NOT for aluminum — -AL geometry with a polished flute is required |
| ✗ | NOT for hardened steels above 45 HRC — select an insert with a CBN cutting edge |
edges, grade H6310, designation and milling parameters
Two — the positive 85° rectangle with a clearance angle of 11° is a single-sided insert that cuts with one face. You use 2 corners; after the first one wears out, rotate the insert in the milling head pocket to the second edge without replacing the tool.
Grade H6310 is PVD-coated cemented carbide, a versatile grade for steel P20-P40 and stainless steel M20-M40. Do not use it for hardened steels above 45 HRC — cubic boron nitride (CBN) inserts are intended for hard machining.
PDER and H2 are proprietary codes; no specific meaning should be assigned to them without the manufacturer's data sheet. H6310 indicates the carbide grade.
For structural steel (ISO P) with a 90° milling head, use a cutting speed of 130-200 m/min, a feed per tooth of 0.10-0.20 mm and a depth of 1-4 mm. Use climb milling on CNC machining centers. For stainless steel, reduce the speed to 70-130 m/min and maintain a continuous coolant supply.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


