





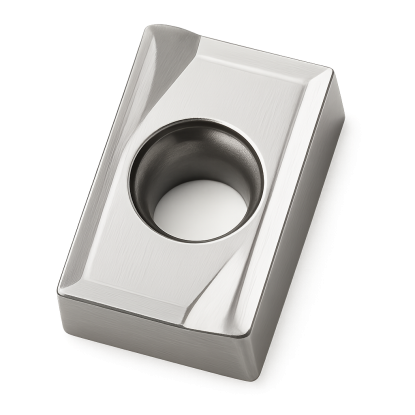

Description
| Technical data | |
|---|---|
| Edge length l | 10 mm |
| Insert thickness s | 3.5 mm |
| Corner radius rε | 0.5 mm |
| Shape | Rectangular 85° (A) |
| Clearance angle | 11° positive (P) |
| Tolerance | class K (precision) |
| Number of edges | 2 |
| Grade | K10 (uncoated carbide) |
nonferrous metals and gray cast iron — ISO N and K groups, 90° angle milling heads
| Material | Finishing | Semi-finishing | Roughing | ||||||
|---|---|---|---|---|---|---|---|---|---|
| Vc [m/min] | fz [mm/tooth] | ap [mm] | Vc [m/min] | fz [mm/tooth] | ap [mm] | Vc [m/min] | fz [mm/tooth] | ap [mm] | |
| NAluminum, nonferrous metals | 400-600 | 0.10-0.15 | 1-2 | 350-500 | 0.10-0.15 | 2-4 | 300-450 | 0.15-0.25 | 4-6 |
| KGray cast iron | 220-280 | 0.10 | 1-2 | 180-240 | 0.15 | 2-3 | 150-220 | 0.20-0.25 | 3-5 |
single-sided 85° rectangle with positive geometry and a sharp edge
Milling insert APKT is a single-sided, positive indexable insert with a rectangular shape and a 85° corner angle, designed primarily for milling aluminum and other nonferrous metals. It is made of uncoated cemented carbide in grade K10, which combines high hardness with a smooth, sharp cutting edge. The positive geometry with a 11° clearance angle reduces cutting forces and limits built-up edge formation, which is typical when machining soft aluminum. The insert is mounted in 90° angle milling heads and cutters for milling shoulders, pockets, and straight vertical walls. Precision class K tolerance ensures uniform height of all cutting edges in a multi-insert milling head and an even load on each corner.
Insert APKT performs well in milling narrow slots, cutouts, and projections, as well as face milling steps. The 90° entering angle directs forces primarily radially, allowing the full shoulder depth to be engaged in one pass. Calculate milling head speed using n = 1000·vc/(π·D): for a milling head with a diameter of 63 mm and a cutting speed of 400 m/min, the result is approximately 2020 rpm. For aluminum, maintain a high cutting speed and generous cooling to prevent chips from clogging the flute and welding to the cutting edge.
The sharp, uncoated edge of grade K10 produces low roughness and clean slot walls, making the carbide insert well suited to finishing aluminum housings, plates, and profiles. The 0.5 mm corner radius strengthens the tip at moderate feeds, but select feed per tooth (fz) carefully when milling cast iron. Match depth of cut ap to mounting rigidity: with slender arbors and thin-walled workpieces, limit it to avoid vibration caused by the radial direction of forces at a 90° angle. Two cutting edges allow the insert to be rotated once the first corner becomes dull, reducing the cost per edge in series production.
Uncoated grade K10 is intended primarily for aluminum, other nonferrous metals, and cast iron. For steel and stainless steel, select an insert APKT in a grade approved for ISO P or M groups.
how to read the APKT 100305 PDFR code — positions 1–10 of the designation
Designation APKT 100305 PDFR according to the standard ISO 1832: 4 letters describe the geometry and construction, 2 numeric codes describe the dimensions, and the suffix PDFR — the wiper edge geometry. Each field has a number, an icon and a brief description.
ISO 1832 designation decoder — how to read the code
Positions 1–4 · ISO code
1AShape
Parallelogram 85°
2 corners of 85° per side
2PClearance angle
α = 11°
positive, single-sided
3KTolerance
Class K (precision)
ground thickness ±0.025 mm
4TType
Countersunk hole + chip breaker
countersink 40–60°, single-sided chip breaker
Positions 5–7 · dimensions [mm]
510Edge length
code 10
dimension according to the manufacturer's catalog data sheet
603Thickness
s = 3.18 mm
between rake faces
705Corner radius
rε = 0.5 mm
code ÷ 10 → radius in mm
PDFR suffix · wiper edge
7PEntering angle
κ = 90°
90° angle milling cutters and milling heads
8DWiper land
α′ = 15°
wiper land clearance angle
9FEdge condition
Sharp
as ground, without edge preparation
10RHand
Right-hand
standard clockwise spindle rotation
✓ 2 corners × 1 side = 2 cutting edges
materials and operations suitable for grade K10
Recommended and non-recommended applications:
| Rating | Material or operation |
|---|---|
| ✔ | Aluminum and aluminum alloys (ISO N) — the primary application of grade K10 |
| ✔ | Other nonferrous metals: brass, bronze, copper |
| ✔ | Gray cast iron (ISO K) — uncoated, hard cemented carbide |
| ✔ | Milling 90° shoulders, slots, and projections, and face milling steps |
| ✔ | 90° angle milling heads and cutters with a pocket for the APKT 1003 insert |
| ✗ | Steel and stainless steel without a grade approved for ISO P or M groups |
| ✗ | 45° face milling — geometry dedicated to 90° milling heads |
| ✗ | ISO S heat-resistant superalloys — outside the application range of uncoated K10 |
grade, materials, geometry, and number of edges
Primarily for aluminum and nonferrous metals (group ISO N) and gray cast iron (ISO K). Grade K10 is an uncoated cemented carbide with high hardness and a sharp edge.
Two — the rectangle with a corner angle of 85° has two sharp corners, and the positive, single-sided design allows cutting only with the top face. Once the first corner becomes dull, rotate the insert in its pocket to the second edge without changing the tool holder.
Conservative settings for aluminum: cutting speed 400–600 m/min, a feed per tooth of 0.10–0.15 mm and a depth of 1–2 mm for finishing, and for roughing vc 300–450 m/min, fz up to 0.25 mm and ap up to 6 mm. Always verify these values against the data sheet for the milling head being used.
The letters APKT describe the basic geometry and design according to ISO 1832, while the numbers correspond to dimensions: length 10 mm, a thickness of 3.5 mm and radius 0.5 mm. PDFR is the manufacturer's geometry code; its meaning must be checked in the product data sheet.

Reference: 012161 In stock < 10 items
€61.50 brutto

Reference: 565302 In stock < 10 items
€84.16 brutto
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


