






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot

Description
SPKN 1504 EDL milling insert – 75° square H10
| Technical data | |
|---|---|
| Side length l = IC | 15.87 mm |
| Insert thickness s | 4.76 mm |
| Shape | S — square, κ 75° |
| Clearance angle | 11° (positive) |
| Hole / chip breaker | none — clamp mounting |
| Wiper edge | ground land (wiper) |
| Version | L — left-hand |
| Carbide grade | H10 (uncoated) |
| ANSI code | SPKN 53 |

Cutting data for the SPKN 1504 insert for cast iron and nonferrous metals
facing and face milling with a 75° milling head — ISO K and N groups
| Material | vc [m/min] | fz [mm/tooth] | ap [mm] | ae [% D] |
|---|---|---|---|---|
| KGray and ductile cast iron | 150-250 | 0.10-0.25 | 1.0-4.0 | 60-80 |
| NNonferrous metals and Al alloys | 300-600 | 0.12-0.30 | 1.0-5.0 | 60-80 |
H10 cemented carbide insert – design and applications
75° square, wiper edge, clamp mounting
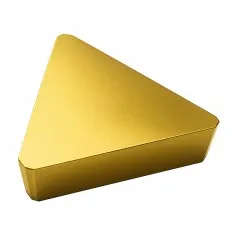
The SPKN 1504 EDL milling insert is a square, single-sided indexable insert made of H10 grade cemented carbide, manufactured by the Polish company Baildonit. The square S shape provides four cutting edges, and the positive geometry with an eleven° clearance angle reduces cutting forces during face milling. The suffix EDL describes a seventy-five° entering angle (letter E), a fifteen° wiper land clearance angle (D), and a left-hand version (L). The insert has no hole or chip breaker — it is secured by a top clamp or wedge in the face milling head pocket. The ground wiper edge at the corner smooths the bottom surface and improves its finish after the cutter passes.
Key benefits of the SPKN 1504 EDL milling insert
- Four cutting edges — the square shape provides 4 usable corners; once an edge is worn, simply index the insert in the pocket without replacing the holder.
- H10 grade for ISO K and N groups — uncoated K10-K20 carbide for cast iron and short-chipping nonferrous metals.
- Wiper edge at the corner — the ground land smooths the bottom of the cut and improves the surface finish after face milling.
- The 11° positive geometry reduces forces and power consumption during face milling with a seventy-five° milling head.
- Design without a hole — secured from above by a clamp or wedge, without weakening the center of the insert.
- Dimensions according to the ISO 3365 family: side l = IC 15.87 mm, thickness 4.76 mm, ANSI code SPKN 53.
Square insert applications and cutting data selection
The SPKN 1504 indexable insert is suitable for facing and face milling gray cast iron, ductile cast iron, and nonferrous metal alloys. H10 grade covers ISO K10-K20 groups and group N materials, making it well suited to short-chipping materials. Calculate milling head speed using n = 1000 × vc / (π × D). A milling head diameter of 80 mm at a cutting speed of 180 m/min gives approximately 716 rpm. With five inserts and a feed per tooth (fz) of 0.15 mm, this gives a table feed rate of approximately 537 mm/min.
The wiper edge limits the feed — keep feed per revolution below sixty percent of the wiper land width to obtain a smooth surface without undercuts. The left-hand EDL version requires a milling head with a matching direction of rotation, so check the R or L pocket designation before installation. The H10 insert is uncoated, so it performs best dry or with compressed-air cooling in cast iron, and with emulsion in nonferrous metals. Select a depth of cut from one to four millimeters, without exceeding the active cutting edge length.
▲
Application limitation
Grade H10 is uncoated and designed for short-chipping materials. We do not recommend it for long-chipping structural steels or hardened steels — for those, select a PVD-coated insert, for example Baildonit N250.
Square insert designation decoder according to ISO 1832
how to read the SPKN 1504 EDL code — positions 1–9 of the designation
Designation SPKN 1504 EDL according to the standard ISO 1832: 4 letters describe the geometry and construction, 2 numeric codes describe the dimensions, and the suffix EDL — the wiper edge geometry. Each field has a number, an icon and a brief description.
ISO 1832 designation decoder — how to read the code
1Sshape 2Pangle α 3Ktolerance 4Ntype – 515size 604thickness – 7Eangle κ 8Dland α′ 9Lhand
Positions 1–3 · ISO code
1SShape
Square 90°
4 corners of 90° per side
2PClearance angle
α = 11°
positive, single-sided
3KTolerance
Class K (precision)
ground thickness ±0.025 mm
Positions 4–6
4NType
Without hole or chip breaker
clamp or wedge mounting
515Size
l = 15.87 mm
IC = 15.87 mm (square: IC = l)
604Thickness
s = 4.76 mm
between rake faces
EDL suffix · wiper edge
7EEntering angle
κ = 75°
75° face milling heads
8DWiper land
α′ = 15°
wiper land clearance angle
9LHand
Left-hand
mirror-image machining and special configurations
✓ 4 corners × 1 side = 4 cutting edges
Full designation: SPKN 1504 EDL = 90° square · 11° positive · class K · without a hole or chip breaker · IC 15.87 mm (l 15.87 mm) · s 4.76 mm · κ 75° · 15° wiper land · left-hand (L)
Compatible milling heads and cutters for the SPKN 1504 insert
75° face milling heads — clamp or wedge mounting
Milling head and material selection
| ✔ | 75° face milling heads with an SPKN pocket (clamp/wedge mounting): FWT 75°, Darmet FB75SP15 |
| ✔ | Gray and ductile cast iron (ISO K), nonferrous metals, and aluminum alloys (ISO N) |
| ✔ | Finishing and semi-finishing — facing and face milling |
| ✔ | Left-hand version (L) — match the milling head's direction of rotation to the pocket designation |
| ✗ | 90° angle milling heads — use TPKN inserts (κ 90°), not SPKN |
| ✗ | 45° milling heads — require SEKT/SEHT inserts with a different shape |
| ✗ | Hardened steels and long-chipping structural steels — H10 is uncoated; a PVD coating is recommended |
| ✗ | Holders for inserts with a hole (APKT/SEKT) — different mounting system |
Frequently asked questions about the SPKN 1504 insert
H10 grade, milling head selection, left-hand direction
Four — a square has 4 corners, and the positive geometry with a 11° clearance angle makes the insert single-sided, cutting only with its top face. Once a corner is worn, index the insert in the pocket to the next edge without changing the milling head.
H10 grade is an uncoated carbide in the group ISO K10-K20 (plus N). It is suitable for gray and ductile cast iron, nonferrous metals, and short-chipping materials. It is not intended for long-chipping structural steels or hardened steels — for those, select a PVD-coated insert.
Three sub-positions: E = entering angle κ 75°, D = wiper land clearance angle 15°, L = left-hand version. The right-hand counterpart is designated EDR. These codes are standardized according to ISO 1832 / GOST 19042-80.
Face milling heads 75° with an SPKN pocket, securing the insert with a clamp or wedge (without a hole), for example FWT 75° or Darmet FB75SP15. Neither 90° angle milling heads (for TPKN) nor 45° heads (for SEKT/SEHT) are compatible.
Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you



Viewed products




This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.