







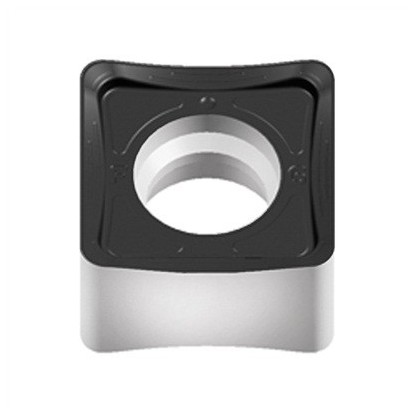


Net price: €5.26
Description
| Technical data | |
|---|---|
| Shape | Square (S) — 4 corners |
| Clearance angle | 0° (N — negative) |
| Side length l | 13.5 mm |
| Insert thickness s | 6.8 mm |
| Tolerance class | M |
| Type | X (proprietary) |
| Grade | TT6080 (TaeguTec) |
| Application | cast iron (ISO K) |
conservative ranges for ISO K group according to ISO 513
| Material | Vc [m/min] | Feed fz [mm/tooth] | ap [mm] | ae [% D] |
|---|---|---|---|---|
| KGray cast iron | 180-300 | 0.10-0.28 | 1.0-4.0 | 60-80 |
square, double-sided negative geometry for milling castings
Milling insert SNMX 1306 is a square, double-sided indexable insert made of cemented carbide in grade TT6080 from TaeguTec, designed for milling cast iron. The square shape, designated by the letter S, provides four corners on each side, and the negative geometry with zero clearance angle allows the insert to be flipped to use a total of eight edges. The letter X confirms only the manufacturer's special type. Geometry details and suitability for cast iron are determined by the designation XTN-TT6080, rather than by the letter X in the ISO code alone. The insert dimensions are a side length of 13.5 millimeters and a thickness of 6.8 millimeters — a substantial body that withstands roughing loads and interrupted milling well.
The carbide insert SNMX is used in milling heads for face milling and roughing iron castings: housings, flanges, plates, and machine components. The strong negative edge performs well at large depths of cut and on hard casting skin. Calculate spindle speed using n = vc·1000/(π·D). A milling head diameter of 63 millimeters at a cutting speed (vc) of 200 meters per minute gives approximately 1011 rpm. With five inserts and a feed of 0.2 millimeters per tooth, this gives a table feed rate of over 1000 millimeters per minute. This feed rate ensures a high material removal rate when face milling large casting surfaces.
Conservative ranges for gray cast iron are a cutting speed of 180–300 meters per minute and a feed of 0.10–0.28 millimeters per tooth; select values according to clamping rigidity and machine power. Cast iron is usually milled dry or with minimum quantity lubrication, because intensive emulsion cooling during interrupted cutting promotes thermal cracking of the coating. Keep the depth of cut below the active cutting edge length, and start at lower speeds on casting skin to limit corner wear. Once all eight edges are dull, replace the insert with a new one of the same grade and geometry type. ISO K group includes both gray cast iron and higher-strength ductile cast iron.
Grade TT6080 and geometry type X are designed for milling cast iron (ISO K). For stainless steel, heat-resistant alloys, and hardened steels, select an insert with a grade and geometry intended for those materials.
how to read the SNMX 1306 code — positions 1–6 of the designation
Designation SNMX 1306 according to the standard ISO 1832: 4 letters describe geometry and construction, 2 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
ISO 1832 designation decoder — how to read the code
Positions 1–3 · ISO code
1SShape
Square 90°
4 corners of 90° per side
2NClearance angle
α = 0°
negative, double-sided
3MTolerance
Class M (intermediate)
IC ±0.10 · thickness ±0.13 mm
Positions 4–6
4XType
Manufacturer-specific special type
features outside the ISO 1832 code
513Size
l = 13.5 mm
IC = 13.5 mm (square: IC = l)
606Thickness
s = 6.35 mm
between rake faces
✓ 4 corners × 2 sides = 8 cutting edges
milling heads for negative square inserts — applications and limitations
Compatible milling heads / applications:
| ✓ | Milling heads with a pocket for a size 1306 negative square SNMX insert |
| ✓ | Milling gray cast iron (ISO K) — face milling and roughing castings |
| ✓ | Double-sided use — 8 cutting edges (4 corners × 2 sides) |
| ✓ | Interrupted milling and castings with hard casting skin |
| ✗ | Turning tool holders — the insert is designed for milling, not for turning tools |
| ✗ | Milling heads for positive inserts — different clearance angle geometry |
| ✗ | Hardened steels and hard machining — carbide grade intended for cast iron |
designation, materials, and milling parameters
Eight. The square has 4 corners, and the negative geometry with a 0° clearance angle makes the insert double-sided. Once one side is dull, flip the insert in the pocket and use the next 4 edges — a total of 8 cutting edges.
For milling gray cast iron, group ISO K. Conservative parameters are a cutting speed of 180–300 m/min and a feed of 0.10–0.28 mm/tooth; select them according to clamping rigidity, machine power, and milling head diameter.
S = square (4 corners), N = 0° clearance angle (negative insert), M = tolerance class, X = manufacturer's special type; geometry and application details are defined by the designation XTN-TT6080. The number 1306 encodes the size: side length l = 13.5 mm and thickness s = 6.8 mm.
Gray cast iron is usually milled dry or with minimum quantity lubrication (MQL). Intensive emulsion cooling during interrupted milling causes thermal shock at the edge and promotes cracking of the insert coating.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


