






Description
| Technical data | |
|---|---|
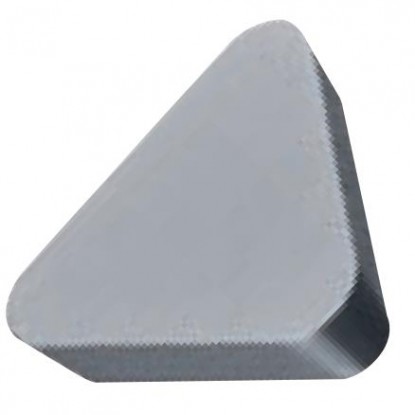
| Side length l | 16.5 mm |
| Insert thickness s | 3.18 mm |
| Inscribed circle dimension IC | 9.525 mm |
| Corner radius rε | 0.4 mm |
| Wiper chamfer width | approx. 1.3 mm |
| Entering angle κ | 90° |
| Tolerance class | M (intermediate) |
| Grade | MTC (Horn) |
| ANSI code | TPM 32 |
shoulder milling with a 90° milling head — ISO P and M groups, conservative values
| Material | vc [m/min] | Feed per tooth fz [mm] | ap [mm] | ae [% D] |
|---|---|---|---|---|
| PSteel | 130-200 | 0.10-0.20 | 1.0-4.0 | 30-70 |
| MStainless steel | 70-130 | 0.06-0.15 | 0.5-2.0 | 25-60 |
single-sided triangle without a hole; PDSR is a manufacturer suffix without interpretation
Milling insert TPMN 1603 PDSR is a single-sided, triangular cemented carbide indexable insert in grade MTC, designed for shoulder milling steel and stainless steel. The triangular insert without a hole or chip breaker is secured with a top clamp, making it suitable for clamp-on milling heads and angle milling cutters. PDSR is the manufacturer's geometry suffix; the TPKN/SPKN family designation decoder must not be applied to it without a separate source for TPMN. The entering angle and corner characteristics require confirmation in the product and milling head data sheets. Positive eleven° clearance reduces cutting forces, making operation easier with less rigid milling heads. Tolerance class M provides intermediate dimensional accuracy and repeatable edge seating after indexing the insert in its pocket.
The triangular insert is suitable for milling shoulders, slots and contours in structural steels and stainless steel components. Calculate the milling head speed using n = 1000·vc/(π·D). For a milling head with a diameter of 63 mm at a cutting speed of 150 m/min, the result is approximately 758 rpm. With five inserts and a feed per tooth (fz) of 0.15 mm, this gives a table feed rate of approximately 568 mm/min. Select a depth of cut ap between one and four millimeters and keep the radial engagement ae below seventy percent of the milling head diameter.
The wiper edge improves the floor finish but requires careful feed selection: keep the feed per revolution below sixty percent of the width of this chamfer to avoid overloading the corner. In stainless steels, reduce the cutting speed to 70–130 m/min and maintain a constant feed to limit work hardening of the layer being cut. Apply a generous stream of coolant emulsion, as heat buildup in the cutting zone accelerates edge wear. Climb milling on a CNC machine extends cutting edge life and improves surface quality.
Grade MTC covers steel (ISO P) and stainless steel (ISO M) but is not intended for machining materials in the ISO H group. The insert has no hole — it is secured only with a top clamp, so it does not fit milling heads with screw-clamping pockets (APKT, SEKT inserts).
how to read the TPUN 1603 PDSR code — designation positions 1–10
Designation TPUN 1603 PDSR according to the standard ISO 1832: 4 letters describe the geometry and construction, 2 numeric codes describe the dimensions, and the suffix PDSR — the wiper edge geometry. Each field has a number, an icon and a brief description.
ISO 1832 designation decoder — how to read the code
Positions 1–3 · ISO code
1TShape
60° triangle
3 corners of 60° per side
2PClearance angle
α = 11°
positive, single-sided
3UTolerance
Class U (wide)
IC ±0.08–0.25 · thickness ±0.13 mm
Positions 4–6
4NType
Without hole or chip breaker
clamp or wedge mounting
516Size
l = 16.5 mm
IC = 9.525 mm · 3/8″
603Thickness
s = 3.18 mm
between rake faces
PDSR suffix · wiper edge
7PEntering angle
κ = 90°
90° angle milling cutters and milling heads
8DWiper land
α′ = 15°
wiper land clearance angle
9SEdge condition
Chamfered and rounded
S-land — strongest edge
10RHand
Right-hand
standard clockwise spindle rotation
✓ 3 corners × 1 side = 3 cutting edges
triangular pocket 16 for TPKN/TPMN inserts, entering angle 90°
| Holder / milling head type | Compatibility |
|---|---|
| 90° shoulder milling head with triangular pocket 16: Dolfamex 220.17 or Darmet FA90TP22 | ✔ yes |
| Top clamping (clamp-on) — insert without a hole | ✔ yes |
| 75° face mill for SPKN inserts | ✗ no |
| 45° face mill for SEKN/SEKT inserts | ✗ no |
| Pockets for inserts with a hole and screw (APKT, SEKT) | ✗ no |
milling head selection, tolerance and milling parameters
Shoulder milling heads and cutters with an entering angle of 90° and a triangular pocket that secures the insert with a top clamp, such as Dolfamex 220.17 or Darmet FA90TP22. The insert has no hole, so it does not fit screw-clamping pockets.
Only the tolerance class in the third position of the designation: M is an intermediate tolerance, while U — wide (looser). The shape and dimensions remain identical: side 16.5 mm, thickness 3.18 mm, IC 9.525 mm. Both versions fit the same 90° milling heads.
PDSR is the manufacturer's geometry suffix. The designation decoder confirmed for TPKN/SPKN must not be applied to TPMN; the meaning requires a separate product data sheet.
Yes — MTC grade covers group ISO M. In this case, reduce the cutting speed to 70–130 m/min, maintain a constant feed per tooth 0.06–0.15 mm and continuous coolant flow: austenitic steel conducts heat poorly and work-hardens when cutting too slowly.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


