







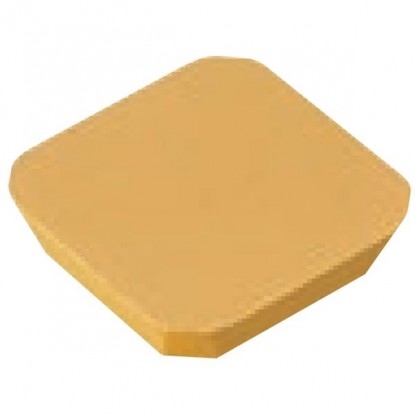


Net price: €6.84
Description
| Technical data | |
|---|---|
| Shape | square (S) |
| Side length l | 15.88 mm |
| Insert thickness s | 4.76 mm |
| Number of edges | 4 |
| Mounting | without a hole, wedge clamping |
| Entering angle κ | 45° |
| AFTN code | manufacturer geometry; meaning according to the Palbit data sheet |
| Grade | Palbit 6920 (CVD) |
| ISO groups | P10-P35 · M15-M25 |
| ANSI code | SEKN 53 |
face milling with a 45° face mill — conservative ranges for ISO groups P and M
| Workpiece material | ISO group | vc [m/min] | fz [mm/tooth] | ap [mm] | ae [% D] |
|---|---|---|---|---|---|
| PStructural steels (up to ~250 HB) | P10-P35 | 150-220 | 0.10-0.22 | 0.5-3.0 | 60-80 |
| MStainless steels (austenitic) | M15-M25 | 80-140 | 0.08-0.18 | 0.3-2.0 | 50-70 |
AFTN code without interpretation, face mills and parameter selection
The SEKN 1504 AFTN milling insert is a square indexable insert made of cemented carbide, designed for face mills operating at an entering angle of 45°. The square shape without a hole provides four cutting edges, secured in the face mill pocket by a wedge. AFTN is the manufacturer's geometry code; its meaning should not be expanded without the Palbit data sheet. The edges are indexed in sequence by rotating the insert in the pocket until all four corners have been used. Operation at an angle of 45° directs most cutting forces axially toward the spindle. This allows the face mill to run more smoothly with less vibration, while chip thickness decreases to approximately 0.71 of the feed per tooth. This allows a higher feed and productive face milling of large surfaces. Indexable inserts in this grade are supplied by Palbit under the designation 6920.
This square cemented carbide insert is suitable for facing and face milling plates, housings and castings made of structural steels and stainless steels. Calculate the face mill speed using n = 1000 · vc / (π · D). For a face mill with a diameter of 80 mm at a cutting speed of 180 m/min, the result is approximately 716 rpm. With six inserts and a feed per tooth (fz) of 0.15 mm, the table feed rate is approximately 644 mm/min. This is the distance the machine table travels in one minute of operation.
Grade 6920, with a CVD coating applied by chemical vapor deposition, withstands demanding conditions in medium machining and roughing. When machining stainless steel, keep the cutting speed in the lower range of 80–140 m/min and maintain a constant feed to limit work hardening of the layer being cut and built-up edge formation. Select a depth of cut ap that does not exceed the active cutting edge length of the insert. Apply a generous, continuous coolant flow for consistent chip and heat removal from the cutting zone. Use the insert on both conventional machine tools and CNC milling centers.
The edge enters the material at 45°, so a face mill with SEKN inserts cannot produce a vertical 90° wall. For milling shoulders and square steps, select an insert for a 90° milling head (e.g. APKT). Grade 6920 is intended for steel and stainless steel, not hardened materials.
how to read the SEKN 1504 AFTN code — positions 1–10 of the designation
Designation SEKN 1504 AFTN according to the standard ISO 1832: 4 letters describe the geometry and construction, 2 numeric codes describe the dimensions, and the suffix AFTN — the wiper edge geometry. Each field has a number, an icon and a brief description.
ISO 1832 designation decoder — how to read the code
Positions 1–3 · ISO code
1SShape
Square 90°
4 corners of 90° per side
2EClearance angle
α = 20°
positive, single-sided
3KTolerance
Class K (precision)
ground thickness ±0.025 mm
Positions 4–6
4NType
Without hole or chip breaker
clamp or wedge mounting
515Size
l = 15.88 mm
IC = 15.88 mm (square: IC = l)
604Thickness
s = 4.76 mm
between rake faces
AFTN suffix · wiper edge
7AEntering angle
κ = 45°
45° angle milling cutters and milling heads
8FWiper land
α′ = 25°
wiper land clearance angle
9TEdge condition
Chamfered (T-land)
the chamfer strengthens the edge during roughing
10NHand
Right-hand and left-hand
symmetrical design
✓ 4 corners × 1 side = 4 cutting edges
face milling at 45° — applications and limitations
Application range of this indexable insert:
| Rating | Application |
|---|---|
| ✔ | Facing and face milling large surfaces with 45° face mills |
| ✔ | Machining structural steels (ISO P10-P35) — medium machining and roughing |
| ✔ | Machining austenitic stainless steels (ISO M15-M25) |
| ✔ | Operation on conventional machine tools and CNC milling centers |
| ✗ | NOT for milling shoulders and vertical 90° walls (the edge operates at 45°) |
| ✗ | NOT for hardened materials or superalloys (outside the application range of grade 6920) |
edges, grade, face mill angle and stainless steel machining
Four — the square shape without a hole provides 4 corners that work as separate edges. When one edge is worn, rotate the insert in the face mill pocket by 90°, until all four have been used, without replacing the entire insert.
Grade 6920 is a CVD-coated cemented carbide for ISO groups P10-P35 (structural steels) and M15-M25 (stainless steels). It is suitable for medium machining and roughing, including demanding cutting conditions.
45° — it is a face milling head. The 45° angle directs forces axially, reduces vibration and thins the chip to approximately 0.71 fz, allowing a higher feed. However, it cannot produce a vertical 90° wall.
Yes — grade 6920 covers ISO group M15-M25. Maintain a cutting speed of 80–140 m/min, a constant feed and a generous coolant flow: austenitic steel dissipates heat poorly and work-hardens if cutting is too slow.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


