





- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot

Description
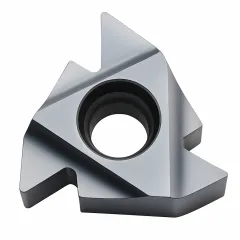
Metric threading insert 16 ER 0.8 ISO BMA – full profile
Technical data for the full-profile insert for 0.8 mm pitch
| Technical data | |
|---|---|
| Designation | 16 ER 0.8 ISO BMA |
| Brand / part number | Fanar / 0000011830 |
| Type | external threading insert, right-hand |
| Profile | full, ISO metric, 60° angle |
| Pitch | 0.8 mm |
| Thread depth | 0.49 mm |
| Thread tolerance class | 6g |
| Insert size | 16: edge 16 mm, IC 9.525 mm |
| Cutting edges | 3 |
| Tool holders | right-hand external SER, size 16 |
| Grade | BMA: submicron carbide, PVD TiAlN |


Pitch0.8 mm

Profilefull ISO

Depth0.49 mm

Tool holdersSER 16
Metric threading insert 16 ER 0.8 ISO BMA turns the full external thread profile at a pitch of 0.8 mm: flanks, root, and crests. It can cut an M5 coarse thread. It operates in size 16 right-hand SER holders. It has three corners for sequential use.
Full ISO profile – flanks, root and major thread diameter
The insert finishes the thread crests in the same cycle
This insert
16 ER 0.8 ISO – full profile
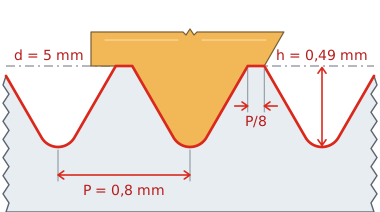
Crests trimmed to diameter d.
Comparison
Partial profile, e.g. 16 ER AG60
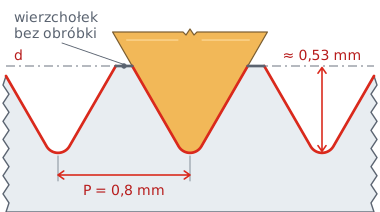
The crests retain the surface from turning the shaft.
Axial cross section of an M5 thread after the final pass. Gold highlights the insert; the red line marks the surfaces machined by the insert.
A full-profile threading insert has short edges on both sides of the tooth. During the final passes, these trim the adjacent thread crests to the major thread diameter. The insert therefore turns both the groove and the thread diameter itself, with a crest flat equal to 1/8 of the pitch, or approximately 0.10 mm.
For an M5 thread in tolerance class 6g, the major diameter is 4.826–4.976 mm and the pitch diameter is 4.361–4.456 mm. Pre-turn the shaft with a small machining allowance. If the diameter is too small, the crests will remain unmachined and the profile will be too shallow. Check the finished thread with a thread ring gauge or a nut.
This insert
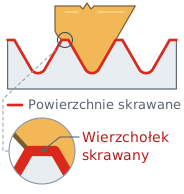
Full profile 16 ER 0.8 ISO
The insert turns the flanks, root and crests of a thread with a 0.8 mm pitch. The crest is formed in the same cycle as the flanks, ensuring a repeatable profile in production runs.
Choose for: production runs of threads with a single pitch.
Comparison
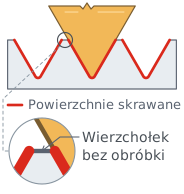
Partial profile, e.g. 16 ER AG60
The insert machines the flanks and root of the groove over a pitch range of 0.5–3.0 mm. It does not touch the crests: they retain the previously turned diameter.
Choose for: short runs and various pitches.
How the 16 ER 0.8 ISO insert cuts threads – passes, feed and cutting data
Feed of 0.8 mm per revolution and 4–7 progressively shallower passes
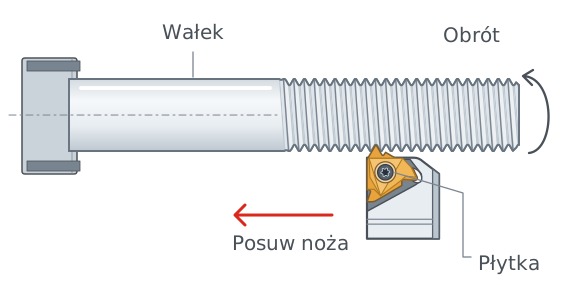
Schematic illustration: insert in a right-hand SER holder in front of the lathe axis. Gold highlights the insert.
One spindle revolution – 0.8 mm of feed
The shaft rotates while the insert advances along the axis by 0.8 mm per spindle revolution. In a typical setup, the right-hand insert feeds toward the chuck and cuts a right-hand thread. During the final passes, its side edges trim the crests to the thread diameter.
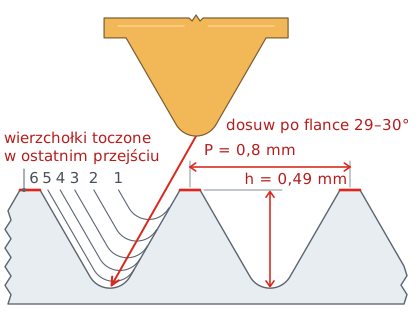
Schematic illustration of the passes for an M5 thread. The lines show successive cutting edge positions.
Successive passes to a depth of 0.49 mm
The insert reaches a depth of 0.49 mm in 4–7 passes; start with 6. The first pass removes the most material, while the final pass removes 0.05–0.08 mm. Use flank infeed at 29–30° to the radial direction: the insert then cuts mainly on one flank.
At the end of the thread next to the shoulder, machine a runout groove at least 0.9 mm wide and at least 0.49 mm deep.
Cutting speed for BMA grade
BMA is a submicron carbide grade with a PVD TiAlN coating for steels, stainless steels and cast iron. The speeds in the table apply to thread turning.
| Workpiece material | Cutting speed vc [m/min] |
|---|---|
| P Unalloyed steel, cast steel, free-cutting steel | 120–180 |
| P Low-alloy steel and cast steel (up to 5% alloying elements) | 80–130 |
| P High-alloy and tool steel | 60–80 |
| M Stainless steel and stainless cast steel | 90–130 |
| K Gray cast iron | 120–130 |
| K Ductile and malleable cast iron | 100–130 |
Spindle speed and feed for M5
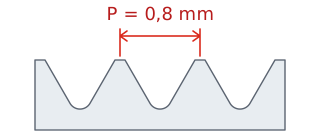
Pitch P is measured along the axis between corresponding points on adjacent thread turns.
For each spindle revolution, the insert advances by one pitch: fn = P = 0.8 mm/rev.
Example: M5 in low-alloy steel, vc = 100 m/min
n = 1000 × vc / (π × d) = 1000 × 100 / (π × 5) ≈ 6370 rpm
vf = n × P = 6370 × 0.8
5096 mm/min
feed rate
d – thread diameter (5 mm), n – spindle speed, vc – cutting speed from the middle of the range in the table, vf – feed rate.
Calculate the helix angle β using the formula tan β = P / (π × d), where P is the pitch and d is the thread diameter. For M5: 0.8 / (π × 5) = 0.051, giving β ≈ 2.92°. Standard threading holder shims tilt the insert by 1–1.5°. This thread has a larger angle, so select a shim with a tilt closer to 2.9° using the holder manufacturer's table.
Thread with a 0.8 mm pitch – M5
One pitch, one size from the standard table
The tooth profile matches a single pitch. The depth of a thread with a 0.8 mm pitch is 0.49 mm.
The 16 ER 0.8 ISO insert can cut an M5 coarse thread.
| Group according to PN-ISO 261 | Thread sizes with a 0.8 mm pitch |
|---|---|
| Coarse threadstandard pitch 0.8 mm | M5 |
M5 is highlighted in gold – the thread used in the drawings and calculation example in this description.
Decoding the 16 ER 0.8 ISO designation – element by element
Size, operating hand, pitch, profile and grade in the insert designation, holder selection
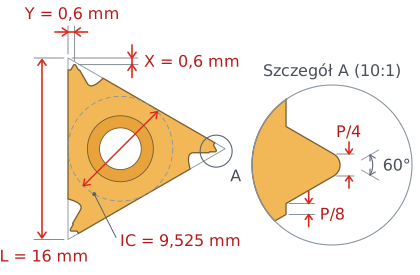
Dimensions according to catalogs for inserts of this standard. Enlarged corner detail.
Dimensions of the 16 ER 0.8 ISO insert
Size 16 denotes an edge length of 16 mm and an inscribed circle IC of 9.525 mm, or 3/8 inch; it is not the thread diameter. Dimensions X = 0.6 mm and Y = 0.6 mm specify the position of the cutting tip relative to the insert sides. The corner reproduces the ISO profile: an angle of 60°, a thread crest of 1/8 of the pitch and a root of 1/4 of the pitch in the nominal profile.
16

Insert size
Edge 16 mm, IC 9.525 mm.
E

External thread
Turning on shafts and journals.
R

Right-hand version
SER holder, feed toward the chuck.
0.8

Thread pitch
0.8 mm; one insert for one pitch.
ISO

Metric profile
Angle 60°, full profile, class 6g.
BMA

Carbide grade
Submicron, PVD TiAlN, P20–P40 and K20–K30.
Only for 0.8 mm pitch and external threads
The insert profile matches a single pitch. At a different feed, the insert flanks will not align with the thread flanks, resulting in a distorted thread. An internal thread has a different depth and radii, so it requires an internal threading insert in an internal holder.
Mount the threading insert in right-hand external SER holders for size 16 inserts, e.g. SER 1616 H16, SER 2020 K16 or SER 2525 M16. A right-hand external insert works only in a right-hand external holder.
The 16 ER 0.8 ISO BMA metric threading insert finishes a thread with a 0.8 mm pitch, including the crests, without a separate finish-turning operation on the diameter. A single insert can cut an M5 thread, always at the same depth of 0.49 mm. It is suitable for production runs requiring a consistent profile.
16 ER 0.8 ISO – questions about selection and applications
Key information before selecting an insert
You can cut all external metric threads with a 0.8 mm pitch: the M5 coarse thread.
Yes. The full profile trims the thread crests at the major diameter, for example to 4.826–4.976 mm for M5 in tolerance class 6g. Simply pre-turn the shaft with a small machining allowance.
The external thread depth is 0.49 mm, or 0.6134 times the pitch.
Right-hand external SER holders for size 16 inserts, e.g. SER 1616 H16, SER 2020 K16, SER 2525 M16 or SER 3232 P16.
Usually 4 to 7 passes; start with 6. For harder materials, add passes instead of increasing the cutting speed.
Product accessories

Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you


This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.