






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot
Description
Trapezoidal threading insert 16 ER 1.5 TR – full 30° profile
Technical data for a full-profile insert for trapezoidal threads with a 1.5 mm pitch
| Technical data | |
|---|---|
| Designation | 16 ER 1.5 TR MTA |
| Brand / part number | Horn / 15165 |
| Type | external threading insert, right-hand |
| Profile | full, trapezoidal Tr, 30° angle |
| Pitch | 1.5 mm |
| Profile height | 0.90 mm |
| Thread tolerance class | 7e |
| Insert size | 16: edge 16 mm, IC 9.525 mm |
| Cutting edges | 3 |
| Tool holders | right-hand external SER, size 16 |
| Grade | MTA: submicron carbide, PVD TiAlN |


Pitch1.5 mm

Profilefull Tr 30°

Depth0.90 mm

Tool holdersSER 16
Trapezoidal threading insert 16 ER 1.5 TR turns the full external thread profile with a 1.5 mm pitch: flanks, roots, and crests. It can cut Tr 8 × 1.5, Tr 9 × 1.5, and Tr 10 × 1.5 threads. It works in size 16 right-hand SER holders. It has three corners for use in succession.
Full Tr 30° profile – flanks, roots, and thread diameter
The insert finishes the thread crests in the same cycle
This insert
16 ER 1.5 TR – full profile
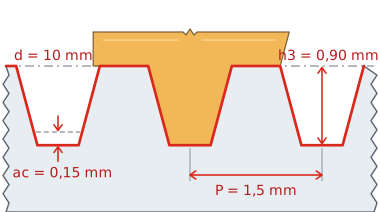
Crests trimmed to diameter d.
Axial cross-section of a Tr 10 × 1.5 thread after the final pass. Gold highlights the insert; the red line indicates the surfaces machined by the insert.
The trapezoidal profile has a 30° flank angle and flat roots and crests. The external thread profile height h3 is 0.5 of the pitch plus the crest clearance ac = 0.15 mm, giving 0.90 mm. The insert turns the flanks, roots, and crests at the thread diameter in the same cycle.
The Tr 10 × 1.5 thread has a major diameter of 10 mm, a pitch diameter d2 = d − 0.5 × P = 9.25 mm, and a minor diameter d3 = d − 2 × h3 = 8.2 mm (PN-ISO 2904). Tolerance 7e is specified in the trapezoidal thread standard. Turn the shaft beforehand, leaving a small machining allowance. An undersized diameter will leave the crests unmachined and the profile too shallow. Check the finished thread with a thread ring gauge or a nut.
Threading with the 16 ER 1.5 TR insert – passes, feed, and cutting data
Feed of 1.5 mm per revolution and 5–11 progressively shallower passes
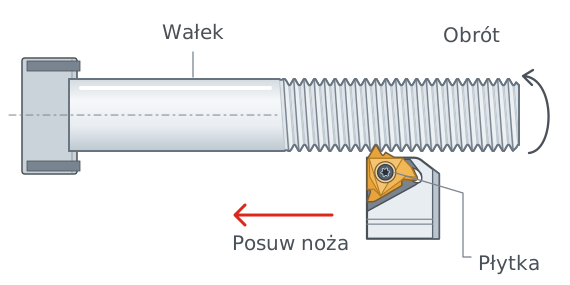
Schematic illustration: insert in a right-hand SER holder in front of the lathe axis. Gold highlights the insert.
One spindle revolution – 1.5 mm of feed
The shaft rotates while the insert advances along the axis by 1.5 mm per spindle revolution. In a typical setup, the right-hand insert feeds toward the chuck and cuts a right-hand thread. During the final passes, its side edges trim the crests to the thread diameter.
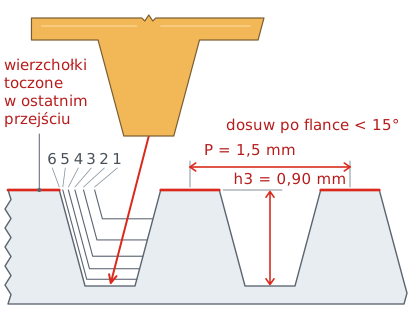
Schematic of the passes for a Tr 10 × 1.5 thread. The lines show successive cutting edge positions.
Successive passes to a depth of 0.90 mm
The insert reaches a depth of 0.90 mm in 5–11 passes; use 8 as a starting point. The first pass removes the most material; the final pass removes 0.05–0.08 mm. Use flank infeed at an angle slightly less than 15°, which is half the profile angle: the insert then cuts mainly on one flank.
At the end of the thread next to the shoulder, machine a runout groove at least 1.6 mm wide and at least 0.90 mm deep.
Cutting speed for MTA grade
MTA grade is a submicron carbide with a PVD TiAlN coating for steel, stainless steel and cast iron. The speeds in the table apply to thread turning.
| Workpiece material | Cutting speed vc [m/min] |
|---|---|
| P Unalloyed steel, cast steel, free-cutting steel | 120–180 |
| P Low-alloy steel and cast steel (up to 5% alloying elements) | 80–130 |
| P High-alloy and tool steel | 60–80 |
| M Stainless steel and stainless cast steel | 90–130 |
| K Gray cast iron | 120–130 |
| K Ductile and malleable cast iron | 100–130 |
Spindle speed and feed for Tr 10 × 1.5
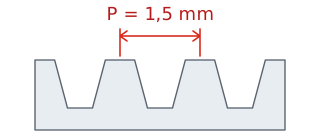
Pitch P is measured along the axis between corresponding points on adjacent thread turns.
For each spindle revolution, the insert advances by one pitch: fn = P = 1.5 mm/rev.
Example: Tr 10 × 1.5 in low-alloy steel, vc = 100 m/min
n = 1000 × vc / (π × d) = 1000 × 100 / (π × 10) ≈ 3180 rpm
vf = n × P = 3180 × 1.5
4770 mm/min
feed rate
d – thread diameter (10 mm), n – spindle speed, vc – cutting speed from the middle of the range in the table, vf – feed rate.
Calculate the helix angle β using tan β = P / (π × d), where P is the pitch and d is the thread diameter. For Tr 10 × 1.5: 1.5 / (π × 10) = 0.048, giving β ≈ 2.73°. Standard threading holder shims tilt the insert by 1–1.5°. This thread has a larger angle, so select a shim with an inclination closer to 2.7° using the holder manufacturer's table.
Trapezoidal threads with a 1.5 mm pitch – from Tr 8 × 1.5 to Tr 10 × 1.5
One insert, many diameters with the same pitch
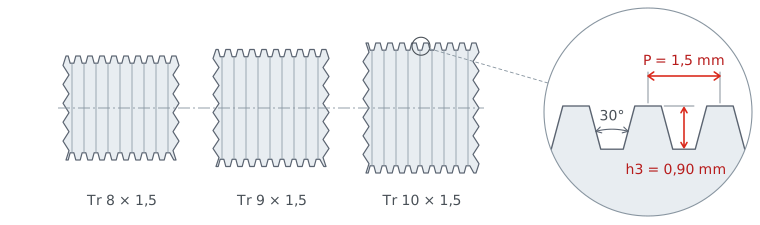
Shaft diameters shown to the same scale. The tooth profile and thread depth are identical on each.
The pitch and tooth profile are independent of diameter. The profile height of a thread with a 1.5 mm pitch is always 0.90 mm, for both Tr 8 × 1.5 and Tr 10 × 1.5. The shaft being machined determines the thread diameter, not the insert.
The 16 ER 1.5 TR insert can cut trapezoidal threads listed in the PN-ISO 2902 table with a 1.5 mm pitch.
| Group according to PN-ISO 2902 | Thread sizes with a 1.5 mm pitch |
|---|---|
| Tr threadsPN-ISO 2902, pitch 1.5 mm | Tr 8Tr 9Tr 10× 1.5 |
Tr 10 × 1.5 is highlighted in gold – the thread shown in the drawings and calculation example in this description.
Decoding the 16 ER 1.5 TR designation – element by element
Size, operating hand, pitch, profile and grade in the insert designation, holder selection
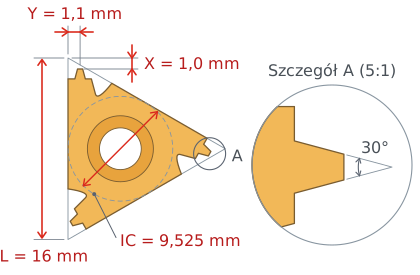
Dimensions according to catalogs for inserts of this standard. Enlarged corner detail.
16 ER 1.5 TR insert dimensions
Size 16 indicates an edge length of 16 mm and an inscribed circle IC of 9.525 mm, or 3/8 inch; it is not the thread diameter. Dimensions X = 1.0 mm and Y = 1.1 mm specify the cutting tip position relative to the sides of the insert. The corner reproduces the trapezoidal profile: a 30° angle, a flat root, and crest clearance ac = 0.15 mm.
16

Insert size
Edge 16 mm, IC 9.525 mm.
E

External thread
Turning on shafts and journals.
R

Right-hand version
SER holder, feed toward the chuck.
1.5

Thread pitch
1.5 mm; one insert for one pitch.
TR

Tr trapezoidal profile
30° angle, full profile, class 7e.
MTA

Carbide grade
Submicron, PVD TiAlN, P20–P40 and K20–K30.
Only for 1.5 mm pitch and external threads
The insert profile matches a single pitch. At a different feed, the insert flanks will not align with the thread flanks, resulting in a distorted thread. An internal thread has a different depth and radii, so it requires an internal threading insert in an internal holder.
Mount the threading insert in right-hand external SER holders for size 16 inserts, e.g. SER 1616 H16, SER 2020 K16 or SER 2525 M16. A right-hand external insert works only in a right-hand external holder.
The 16 ER 1.5 TR trapezoidal threading insert finishes a trapezoidal thread with a 1.5 mm pitch, including the crests. One insert can cut 3 sizes, from Tr 8 × 1.5 to Tr 10 × 1.5, always with the same profile height of 0.90 mm. It is suitable for lead screws and nuts with this pitch.
16 ER 1.5 TR – selection and application questions
Key information before selecting an insert
You can cut external trapezoidal threads with a 1.5 mm pitch from the PN-ISO 2902 table: Tr 8 × 1.5, Tr 9 × 1.5, and Tr 10 × 1.5.
Yes. The full profile cuts the thread crests at the major thread diameter, for example 10 mm for Tr 10 × 1.5. Simply turn the shaft beforehand, leaving a small machining allowance.
The profile height is 0.5 of the pitch plus the crest clearance ac: 0.75 + 0.15 = 0.90 mm (PN-ISO 2904). It is the same for every diameter with this pitch.
Right-hand external SER holders for size 16 inserts, e.g. SER 1616 H16, SER 2020 K16, SER 2525 M16 or SER 3232 P16.
Usually 5 to 11 passes; start with 8. For harder materials, add passes instead of increasing the cutting speed.
Product accessories

Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you






This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.