






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot

Machine tap M10x1.25 DIN 374/35 C SE
0000006958
€22.33 tax inc.
Net price: €18.16
Description
Material HSSE
Thread size M10x1.25
ChamferC (2–3) threads
Standard DIN 374
Technical data for the M10x1.25 blind hole tap
| Technical Data | |
|---|---|
| Nominal Diameter d1 | M10x1.25 |
| Thread Pitch P | 1.25 mm |
| Helix Angle | 35° |
| Overall Length l1 | 100 mm |
| Flute Length l2 | 20 mm |
| Length l3 | 39 mm |
| Shank Diameter d2 | 7 mm |
| Square Drive Size a | 5.5 mm |
| Tap Drill Diameter | 8.8 mm |
| Chamfer | C (2÷3) P |
| Thread tolerance | 6H |
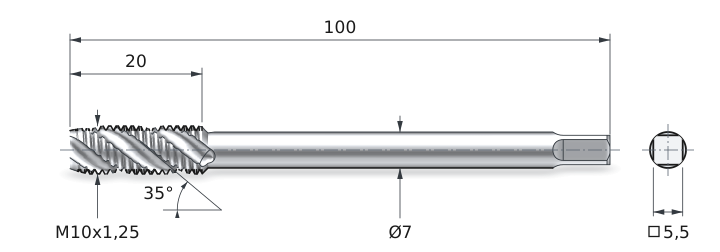
How a spiral flute tap evacuates chips from a blind hole
The 35° flute works like a screw conveyor
The flutes of this tap follow a right-hand helix at an angle of 35° to the axis. The tap rotates clockwise and advances into the hole. Chips cut by the chamfer enter the flute, and the helix carries them upward like the auger in a meat grinder. The bottom of the hole stays clear, and the cutting edges do not encounter packed chips. The M10x1.25 tap has a reduced shank to DIN 374: diameter 7 mm, square drive 5.5 mm.
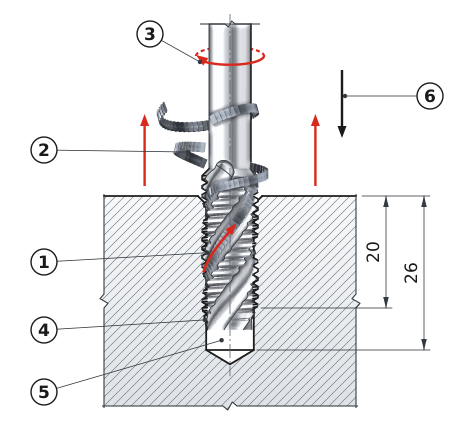
1
The 35° spiral flute carries chips upward from the chamfer.
2
The stepped chip exits the hole and breaks into short pieces.
3
The tap rotates clockwise to cut a right-hand thread.
4
Chamfer C: 2–3 incomplete threads on the tapered lead.
5
Clearance below the tap tip – min. 2 thread pitches above the bottom.
6
Feed 1.25 mm/rev, equal to the pitch of the M10x1.25 thread.
M10x1.25 spiral flute machine tap – for metric fine threads
In this product line, the manufacturer offers the M10x1.25 spiral flute machine tap with an intermediate pitch of 1.25 mm for precision mechanical connections. Made from HSSE steel with 5% added cobalt, the tool meets DIN 374 requirements for metric fine threads and provides a hardness of 65-67 HRC. The 35° spiral flute guarantees controlled chip evacuation when tapping blind holes. The form C chamfer allows tapping close to the bottom of a blind hole with minimal incomplete thread length.
Advantages and applications of the M10x1.25 spiral-flute machine tap
- Compatibility with ER16 and ER25 tool holders and tapping chucks with axial compensation for CNC machining centers and automatic lathes
- Tolerance class 6H precision in accordance with DIN 374 guarantees the dimensional repeatability required in series production of precision components
- Designed for steel structures includes welded components, machine frames, load-bearing structures, and bolted connections with increased strength
- Conforms to DIN 374 for metric fine threads ensures standardized shank dimensions and full interchangeability with European tools
- Durability of HSSE steel allows machining of structural steels up to 900 MPa, alloy steels, aluminum, and copper alloys
- 35° geometry with form C ensures consistent chip evacuation when tapping blind holes to a depth of 2D
The M10x1.25 machine tap is used in steel construction and industrial welding to produce connections with increased strength. The tap drill diameter for the M10x1.25 thread is 8.75 mm. The tool is compatible with standard mineral oil-based tapping lubricants and coolant emulsions.
Cutting data for the M10x1.25 blind hole machine tap
| Material | Cutting speed Vc [m/min] | Spindle speed n [rpm] | Feed f [mm/min] |
|---|---|---|---|
| PSteel | 5-20 | 159-637 | 199-796 |
| MStainless steel | 5-10 | 159-318 | 199-398 |
| KCast iron | 5-15 | 159-477 | 199-596 |
| NAluminum | 10-25 | 318-796 | 398-995 |
Thread preparation M10x1.25 in a blind hole
1 Spot drilling
NC spotting drill 90°
2 Drilling
Ø 8.8 mm
3 Tapping
M10x1.25
✓ Done!
Tolerance 6H
Standard: DIN 374 | Chamfer: C (spiral flute) | Application: blind holes
Tolerance 6H — metric thread tolerance classes
| Class | Accuracy | Application | Status |
|---|---|---|---|
| 4H / 4g | High | Precision connections, hydraulics | — |
| 6H / 6g | Standard | Machine building, general-purpose | SELECTED |
| 7H / 8g | Low | Large clearance, easy assembly | — |
6H = internal thread (nut, hole) | 6g = external thread (screw)
Frequently asked questions
The M10x1.25 HSSE metric fine machine tap is suitable for structural steels up to 900 MPa, stainless steels, aluminum, and brass. The intermediate pitch of 1.25 mm is used in steel structures requiring connections with increased strength.
For the M10x1.25 metric fine thread in tolerance class 6H, the tap drill diameter should be 8.75 mm. The permissible hole tolerance range is 8.75-8.95 mm. A smaller hole increases cutting torque and the risk of tool breakage.
Yes, cooling with an oil emulsion at a minimum concentration of 8% or with tapping oil is recommended and extends tool life by a factor of 2-3. Intensive cooling is required when machining stainless steels, while aluminum can be tapped with minimal lubrication.
Product accessories


Machine Tap M10X1.25 DIN 374 B HSSE
Reference: 0000005925 In stock > 10 items
€14.47
€17.80 brutto


Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.