





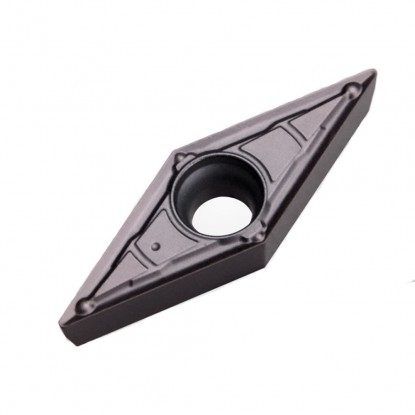

Description
| Technical data | |
|---|---|
| Side length l | 16.5 mm |
| Insert thickness s | 4.76 mm |
| Hole diameter d1 | 4.4 mm |
| Corner radius rε | 0.8 mm |
| Inscribed circle diameter IC | 9.525 mm |
| ANSI code | VBMT 332 |
finishing, semi-finishing and roughing — ISO P and M groups
| Material | Finishing | Semi-finishing | Roughing | ||||||
|---|---|---|---|---|---|---|---|---|---|
| Vc [m/min] | Feed f [mm/rev] | ap [mm] | Vc [m/min] | Feed f [mm/rev] | ap [mm] | Vc [m/min] | Feed f [mm/rev] | ap [mm] | |
| PSteel | 200-295 | 0.07 | 0.14 | 170-240 | 0.14 | 0.32 | 150-215 | 0.27 | 1.8 |
| MStainless steel | 110-230 | 0.07 | 0.14 | 70-175 | 0.14 | 0.32 | 50-135 | 0.27 | 1.8 |
single-sided 35° diamond with a hole and chip breaker
The VBMT 160408 turning insert is a single-sided, indexable diamond insert made of grade H6310 cemented carbide, designed for turning steel and stainless steel. The V shape, a diamond with a 35° corner angle, provides a narrow, sharp tip that facilitates copy turning and machining of profiles and undercuts. The positive geometry with a 5° clearance angle, designated by the letter B, reduces cutting resistance, allowing the insert to run smoothly on slender workpieces prone to vibration. The sharp diamond uses two corners on one side of the insert, providing a total of two cutting edges. The nose radius rε of 0.8 mm combines a good surface finish with corner strength at feed rates of 0.14–0.27 mm/rev.
Grade H6310 is a versatile cemented carbide with a PVD coating, covering ISO groups P20-P40 and M20-M40. The PVD coating increases the cutting edge's resistance to abrasive wear and high temperatures in the cutting zone, keeping the corner sharp longer during operation. The design with a mounting hole and a single-sided chip breaker controls chip flow and chip breaking, while tolerance class M provides repeatable cutting edge positioning after indexing the insert in the pocket. This combination of features makes the insert suitable for finishing and semi-finishing, where surface quality and dimensional accuracy matter.
The VBMT 160408 insert, also written without a space as vbmt160408, is suitable for copy turning of shafts, journals and profiles made of structural steels, as well as stainless steel components. Calculate spindle speed using n = 1000·Vc/(π·D): for a shaft with a diameter of 50 mm at Vc = 200 m/min, the result is approximately 1273 rpm. When machining stainless steels, maintain a cutting speed of 50–230 m/min and a constant feed rate to reduce work hardening of the layer being cut. Grade H6310 indexable inserts are supplied by the Korean brand Horn.
Grade H6310 is not intended for steels hardened above 45 HRC — for hard turning, select the version VBMT 160408 CBN with a cubic boron nitride cutting edge.
how to read the VBMT 160408 code — positions 1–7 of the designation
Designation VBMT 160408 according to the standard ISO 1832: 4 letters describe geometry and construction, 3 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
for VBMT 160408 steel and stainless steel
use, turning tool selection, and turning parameters
Two — the 35° diamond has 2 corners, while the positive, single-sided geometry (letter B) allows only one side of the insert to be used. Once both corners are worn, the insert is replaced with a new one; it cannot be flipped over like a double-sided insert.
Holders with a V-shaped diamond pocket (IC 9.525 mm): for external turning SVJBR/L, SVVBN, SVHBR/L and SVZBR/L with shank cross sections from 16×16 to 32×32 mm; for internal turning, boring bars S25S–S40U with an SVUBR/L, SVQBR/L or SVXBR/L head. See the compatible turning tools section for the complete list.
Only in corner radius: 0.4 mm (160404) is used for finishing at low feed rates, 0.8 mm (160408) is the general-purpose variant, while 1.2 mm (160412) is selected for heavier machining at higher feed rates. The other dimensions — IC 9.525 mm and thickness 4.76 mm — are identical.
Yes — grade H6310 covers group ISO M20-M40. Maintain a cutting speed of 50–230 m/min, a constant feed, and continuous cooling: austenitic steel dissipates heat poorly and work-hardens when cutting is too slow.

Reference: 0000004321 In stock > 10 items
€9.39 brutto
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


