





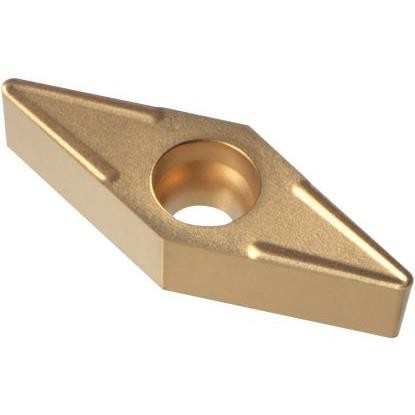

Description
| Technical data | |
|---|---|
| Side length l | 11 mm |
| Insert thickness s | 3.18 mm |
| Hole diameter d1 | 2.8 mm |
| Corner radius rε | 0.8 mm |
| ANSI code | VBMT 222 |
finishing, semi-finishing and roughing — ISO P and M groups
| Material | Finishing | Semi-finishing | Roughing | ||||||
|---|---|---|---|---|---|---|---|---|---|
| Vc [m/min] | Feed f [mm/rev] | ap [mm] | Vc [m/min] | Feed f [mm/rev] | ap [mm] | Vc [m/min] | Feed f [mm/rev] | ap [mm] | |
| PSteel | 200-295 | 0.07 | 0.13 | 170-240 | 0.13 | 0.3 | 150-215 | 0.26 | 1.7 |
| MStainless steel | 110-230 | 0.07 | 0.13 | 70-175 | 0.13 | 0.3 | 50-135 | 0.26 | 1.7 |
single-sided 35° diamond with a hole and chip breaker
The VBMT 110308 turning insert is a single-sided, diamond-shaped indexable insert made of grade H6310 cemented carbide, designed for turning steel and stainless steel. The V shape, an acute diamond with a 35° corner angle, facilitates copy turning and machining profiles with changing feed directions. Positive geometry with a 5° clearance angle reduces cutting forces, allowing the insert to perform well on slender shafts and smaller lathes. The rε 0.8 mm nose radius combines a satisfactory surface finish with edge durability at feeds up to 0.26 mm/rev.
The VBMT 110308 insert (also written without a space as vbmt110308) performs well in finish and semi-finish turning of shafts, bushings, and profiled components made of structural steels and stainless steel. The acute 35° diamond is a typical turning tool insert for copy turning, where the tool must follow a changing workpiece contour without the side of the insert colliding with the material. It also performs well in longitudinal turning of smaller diameters, where dimensional accuracy and low pressure on the slender workpiece are essential.
Calculate spindle speed using n = 1000·Vc/(π·D): for a shaft diameter of 30 mm at Vc = 250 m/min, the result is approximately 2653 rpm. The acute corner angle facilitates profile machining but weakens the insert tip, so select a smaller depth of cut than for diamond inserts with a 80° corner angle. Grade H6310 cemented carbide indexable inserts are supplied by the Korean brand Horn.
When turning stainless steel, maintain a cutting speed of 50–230 m/min, a constant feed, and a continuous supply of emulsion coolant. Austenitic steel conducts heat poorly and work-hardens when cutting is too slow, so avoid interrupting contact between the edge and the material. The insert's positive geometry reduces built-up edge and improves the quality of the turned surface.
Grade H6310 is not intended for steels hardened above 45 HRC — for a turning insert for hardened steel, select the version VBMT 110308 CBN with a cubic boron nitride edge. The acute 35° tip also requires a reduced depth of cut on interrupted surfaces.
how to read the VBMT 110308 code — positions 1–7 of the designation
Designation VBMT 110308 according to the standard ISO 1832: 4 letters describe geometry and construction, 3 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
holders with a VB 11 diamond pocket — external and internal turning
use, turning tool selection, and turning parameters
Two — the diamond has 2 corners with a 35° angle, while positive geometry (code B, 5° clearance angle) indicates a single-sided insert with only the upper rake face in use. Once one corner becomes dull, rotate the insert in its pocket to use the other.
Holders with a VB diamond pocket for size 11 (IC 6.35 mm): for external turning SVJBR/L (entering angle 93°), SVHBR/L, SVVBN and SVZBR/L with cross sections of 12×12–25×25 mm; for internal turning, boring bars S16P–S25S with the suffix SVUBR/L, SVQBR/L, or SVXBR/L. The choice of right-hand (R) or left-hand (L) depends on the feed direction.
Mainly in the nose radius: 0.4 mm (110304) is used for finishing at low feeds and lower radial forces, while 0.8 mm (110308) is a more versatile version with a stronger tip. The remaining dimensions — IC 6.35 mm, edge length 11 mm, and thickness 3.18 mm — are identical.
Yes — grade H6310 covers group ISO M20-M40. Maintain a cutting speed of 50–230 m/min, a constant feed, and continuous emulsion cooling: austenitic steel conducts heat poorly and work-hardens when cutting is too slow.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


