







Description
| Technical data | |
|---|---|
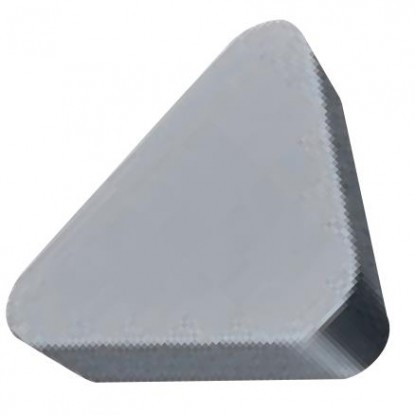
| Side length l | 11 mm |
| Insert thickness s | 3.18 mm |
| Inscribed circle diameter IC | 6.35 mm |
| Corner radius rε | 0.4 mm |
| ANSI code | TPMN 221 |
finishing, semi-finishing and roughing — ISO P and M groups
| Material | Finishing | Semi-finishing | Roughing | ||||||
|---|---|---|---|---|---|---|---|---|---|
| Vc [m/min] | Feed f [mm/rev] | ap [mm] | Vc [m/min] | Feed f [mm/rev] | ap [mm] | Vc [m/min] | Feed f [mm/rev] | ap [mm] | |
| PSteel | 200-295 | 0.1 | 1 | 170-240 | 0.15 | 2 | 150-215 | 0.3 | 3 |
| MStainless steel | 110-230 | 0.1 | 1 | 70-175 | 0.15 | 2 | 50-135 | 0.3 | 3 |
single-sided 60° triangle, positive geometry, 3 edges
The TPMN 110304 turning insert is a single-sided, triangular indexable insert made of MTC grade cemented carbide. The T shape, an equilateral triangle with a 60° corner angle, facilitates access to the workpiece contour during longitudinal turning and facing. Positive geometry with a 11° clearance angle reduces cutting resistance, while the type N design without a hole is secured with a top clamp. Three corners provide three cutting edges, and the corner radius rε 0.4 mm favors finishing at low feed rates. Size 11, with an inscribed circle diameter IC of 6.35 mm, matches a 1/4 inch pocket in turning tool holders.
The TPMN 110304 insert (also written without a space as tpmn110304) performs well when turning cast iron workpieces, as well as steel and stainless steel components, using the specified parameters. Calculate spindle speed using n = 1000·Vc/(π·D): for a shaft with a diameter of 50 mm at Vc = 200 m/min, the result is approximately 1273 rpm. For stainless steel, maintain a constant feed rate and continuous coolant supply to limit work hardening of the layer being cut. According to the manufacturer's data, MTC is a carbide grade designed for efficient cast iron machining at moderate speeds and medium or high feed rates. MTC grade indexable inserts are supplied by the Korean brand Horn.
Positive rake reduces heat generated in the contact zone, which helps when machining materials prone to work hardening. The absence of a chip breaker, indicated by the letter N in the ISO 1832 code, means that chip flow control depends on the pocket geometry and any separate chip breaker. In cast iron, chips are brittle and break naturally; for ductile steel, select a holder with an appropriate entering angle. The small corner radius of 0.4 mm facilitates the transition between roughing and finishing, at the cost of slightly lower corner strength at high feed rates.
The TPMN 110304 insert of type N has no hole or chip breaker — chip control relies on the holder geometry. For turning ductile, long-chipping steel, select a holder with a separate chip breaker; data for grade MTC are limited, so verify parameters for materials other than cast iron, steel, and stainless steel with the supplier.
how to read the TPMN 110304 code — positions 1–7 of the designation
Designation TPMN 110304 according to the standard ISO 1832: 4 letters describe geometry and construction, 3 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
design, chip control, and selection of turning parameters
Three — the triangle has 3 corners, and the single-sided, positive geometry (type N without a hole) allows use of one side of the insert. When a corner wears out, simply rotate the insert in its pocket to the next edge, without changing the holder.
No. The fourth letter N in the ISO 1832 code indicates an insert without a hole or chip breaker, secured with a top clamp. Chip control and breaking then depend on the holder geometry or a separate chip breaker.
The small radius rε 0.4 mm favors finishing at low feed rates: it provides a smooth surface finish and lower radial forces. The tradeoff is lower corner strength, so larger radii are selected for roughing at high feed rates.
Grade MTC is a cemented carbide recommended by the manufacturer for efficient semi-finishing and roughing of cast iron. The parameters listed on the product page also cover turning steel and stainless steel at appropriate speeds and feed rates.

Reference: 0000012829 In stock > 10 items
€22.66 brutto
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


