








Description
| Technical data | |
|---|---|
| Side length l | 11.0 mm |
| Insert thickness s | 3.18 mm |
| Inscribed circle IC | 6.35 mm |
| Corner radius rε | 0.4 mm |
| ANSI code | TPUN 221 |
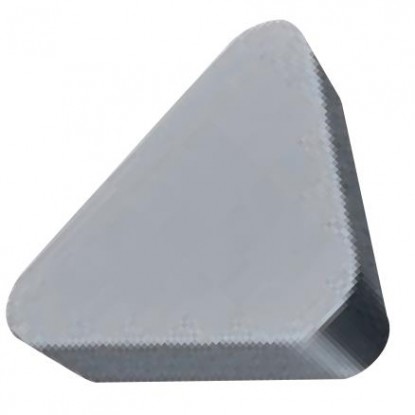
single-sided 60° triangle, positive geometry, without a hole or chip breaker
The TPUN 110304 turning insert is a triangular, single-sided indexable insert made of cemented carbide in grade S10s, designed for turning steel and cast steel. Shape T denotes an equilateral triangle with a corner angle of 60°, providing easier access to the workpiece profile during longitudinal turning and facing. The positive geometry with a clearance angle of 11° reduces cutting forces and is well suited to low feed rates and finishing. The insert has no hole or chip breaker, so it is secured with a top clamp and provides three cutting edges on one side.
The TPUN 110304 insert (also written without a space as tpun110304) is suitable for turning shafts, bushings, and flanges made of structural steels and low-alloy cast steel. Grade S10s is designed for finishing and semi-finishing at high cutting speeds and low feed rates. Calculate spindle speed using n = 1000·Vc/(π·D): for example, for a shaft diameter of 40 mm and a cutting speed Vc = 150 m/min, the result is approximately 1194 rpm. Select the speed to suit the specific steel and setup rigidity, and adjust it after the initial trial passes. TPUN 110304 cemented carbide indexable inserts are supplied by the Polish company Baildonit. This cutting insert is a common choice among turning tool inserts for finishing operations.
In finishing operations, the small nose radius of 0.4 mm provides dimensional accuracy and low surface roughness without overloading the cutting edge. Since the insert has no chip breaker, chip shape and breaking depend on the holder geometry and feed rate selection. For ductile steel, use emulsion cooling to reduce built-up edge and improve surface quality. For cast steel and higher-strength steels, reduce the cutting speed and maintain a constant feed rate to extend cutting edge life. Three edges on one side reduce the cost per cutting edge, while top clamping simplifies insert replacement. This combination of features makes this cemented carbide insert a practical choice for finish turning in series production.
Insert TPUN 110304 has no chip breaker, so it does not control chip flow at high feed rates — it is designed for finishing and semi-finishing. For rough turning with chip breaking, select an insert with a chip breaker (letter 4 G or M in the ISO 1832 designation).
how to read the TPUN 110304 code — designation positions 1–7
Designation TPUN 110304 according to the standard ISO 1832: 4 letters describe geometry and construction, 3 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
number of cutting edges, design, and selection for the workpiece material
Three — the triangle has 3 corners at 60° each, and the positive, single-sided geometry uses only one side of the insert. Once an edge is dull, simply rotate the insert in its pocket without changing the holder.
No — the fourth letter N denotes an insert without a hole or chip breaker. It is secured with a top clamp, and chip control depends on the holder geometry. This design is well suited to finishing at low feed rates.
Variants in the TPUN 1103 family differ mainly in nose radius: 0.4 mm is used for finishing and smooth surfaces, while larger radii increase cutting edge strength when producing thicker chips. The size (IC 6.35 mm) and thickness of 3.18 mm are the same across the family.
Grade S10s is designed for steel, cast steel and low-alloy cast steel in finishing and semi-finishing operations. Use high cutting speeds and low feed rates when using these inserts for finish turning on conventional and CNC machine tools.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


