







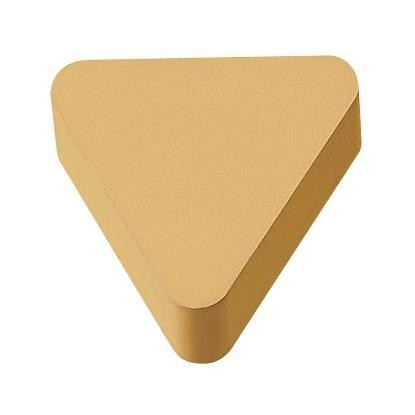

Description
| Technical data | |
|---|---|
| Side length l | 33 mm |
| Insert thickness s | 6.35 mm |
| Inscribed circle diameter IC | 19.05 mm |
| Corner radius rε | 2 mm |
| ANSI code | TNUN 645 |
double-sided 60° triangle without a hole or chip breaker
The TNUN 330620 turning insert is a triangular indexable insert made of S20 grade cemented carbide, intended for turning steel, cast steel and malleable cast iron. Shape T denotes an equilateral triangle with a 60° corner angle, which facilitates access to the workpiece contour during longitudinal turning and facing. Negative geometry with a 0° clearance angle allows both sides of the insert to be used — a total of six cutting edges. The large nose radius rε of 2 mm provides a strong, chip-resistant cutting edge that withstands demanding cutting conditions during roughing and semi-finishing.
The TNUN 330620 insert (also written without a space as tnun330620) performs well when turning shafts, discs and flanges made of structural steels and cast steel, as well as malleable iron castings. Calculate the spindle speed using n = 1000·Vc/(π·D): for a shaft with a diameter of 80 mm and an example cutting speed Vc = 140 m/min, the result is about 557 rpm. Turning tool inserts in this grade are supplied by the Polish company Baildonit.
Grade S20 is uncoated carbide in ISO group P15-P25, which performs best at high cutting speeds and moderate feed rates. When turning steel and cast steel, maintain a constant coolant supply and a uniform feed rate to limit heat generation at the cutting edge. The absence of a chip breaker means a solid rake face, so chip control depends on the selected feed rate, depth of cut and tool holder geometry. The insert performs well on both conventional lathes and CNC machine tools, and predictable cutting edge wear makes it easier to schedule edge changes in series production.
The triangular shape with a 60° corner angle generates lower radial forces than inserts with a 80° or 90° corner, making it well suited to turning more slender shafts where limiting vibration and the risk of workpiece deflection is essential.
Grade S20 is uncoated, so it has lower heat resistance than coated carbides. When turning dry or at very high speeds, the cutting edge wears faster — for hardened steels above 45 HRC and difficult-to-machine alloys, choose a coated insert or a version with CBN.
how to read the TNUN 330620 code — positions 1–7 of the designation
Designation TNUN 330620 according to the standard ISO 1832: 4 letters describe geometry and construction, 3 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
design, material and turning parameters
Six — the triangle has 3 corners per side, and the negative geometry (0° clearance angle) allows both sides of the insert to be used. Once an edge becomes dull, simply rotate the insert in its pocket without changing the holder.
This is type N according to ISO 1832: an insert without a mounting hole or chip breaker, secured with a top clamp. The solid, smooth rake face increases cutting edge rigidity, while chip control is achieved by selecting the feed rate and depth of cut.
Grade S20 is uncoated carbide in group ISO P15-P25, intended for finishing and semi-finishing of steel, cast steel and low-alloy cast steel at high speeds and moderate feed rates. According to the cutting data table, it is also suitable for malleable cast iron (group K).
The large nose radius 2 mm strengthens the insert tip and distributes the load over a longer section of the cutting edge, so it withstands roughing and higher feed rates better. Smaller radii provide a smoother surface when finishing but are more prone to chipping.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


