






- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot
Description
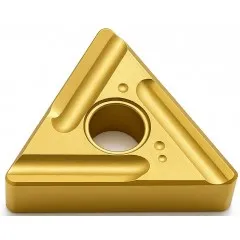
TNMG 160408 turning insert – indexable 60° triangle
| Technical data | |
|---|---|
| Side length l | 16.5 mm |
| Insert thickness s | 4.76 mm |
| Hole diameter d1 | 3.81 mm |
| Corner radius rε | 0.8 mm |
| ANSI code | TNMG 332 |

Cutting data for the TNMG 160408 insert for steel and stainless steel
finishing, semi-finishing and roughing — ISO P and M groups
| Material | Finishing | Semi-finishing | Roughing | ||||||
|---|---|---|---|---|---|---|---|---|---|
| Vc [m/min] | Feed f [mm/rev] | ap [mm] | Vc [m/min] | Feed f [mm/rev] | ap [mm] | Vc [m/min] | Feed f [mm/rev] | ap [mm] | |
| PSteel | 250-350 | 0.1 | 0.1 | 180-270 | 0.2 | 0.4 | 170-220 | 0.4 | 1.5 |
| MStainless steel | 125-260 | 0.1 | 0.1 | 100-220 | 0.2 | 0.4 | 80-200 | 0.4 | 1.5 |
Grade H6310 cemented carbide indexable insert – applications and construction
double-sided 60° triangle with a hole and chip breaker
The TNMG 160408 turning insert is a double-sided, triangular indexable insert made of grade H6310 cemented carbide, designed for turning steel and stainless steel. The T shape denotes an equilateral triangle with a corner angle of 60°, providing easy access to the workpiece contour during longitudinal turning and facing. Negative geometry with a 0° clearance angle allows both sides of the insert to be used, providing a total of six cutting edges. The nose radius rε of 0.8 mm combines a good surface finish with edge strength at feed rates of 0.2–0.4 mm/rev. The hole and double-sided chip breaker control chip flow and breaking during continuous cutting.
Key advantages of the H6310 cemented carbide insert
- Six cutting edges — 3 corners on each of the two sides reduce the cost per cutting edge compared with single-sided inserts.
- Grade H6310 for ISO groups P and M — PVD-coated carbide covers steel (P20-P40) and stainless steel (M20-M40), as well as occasional use on cast iron.
- Corner radius rε 0.8 mm — a general-purpose option spanning finishing and roughing, without changing the insert between operations.
- Tolerance class M ensures repeatable edge positioning after indexing the insert in the holder pocket.
- Dimensions according to ISO 1832: cutting edge length 16.5 mm, IC 9.525 mm (3/8″), thickness 4.76 mm — compatible with holders with a 16 pocket.
- A 60° corner angle produces lower radial forces than a 80° corner — less vibration on slender workpieces.
Applications and parameter selection for the triangular insert
The TNMG 160408 insert (also written without spaces as tnmg160408) performs well when turning shafts, bushings, and flanges made of structural steels, as well as stainless steel components. Calculate spindle speed using n = 1000·Vc/(π·D): for a shaft diameter of 60 mm at Vc = 250 m/min, the result is approximately 1326 rpm, and for a diameter of 40 mm, approximately 1989 rpm. For stainless steels, maintain a cutting speed in the range of 80–260 m/min and a constant feed rate to avoid work hardening of the layer being cut. Grade H6310 indexable inserts are supplied by the Korean brand Horn.
Grade H6310 is PVD-coated carbide covering ISO groups P20-P40 and M20-M40, allowing one insert to handle both structural steel and stainless steel, as well as occasional use on cast iron. The 60° corner angle generates lower radial forces than a 80° corner, reducing vibration when machining slender shafts. For finishing passes, use lower feed rates and depths of cut with speeds at the upper end of the range; for roughing, reduce speed and increase the feed rate and depth of cut ap. Continuous emulsion cooling removes heat from the cutting zone and extends edge life, especially with difficult-to-machine materials.
▲
Application limitation
Grade H6310 is not intended for steels hardened above 45 HRC — for hard turning, select the version TNMG 160408 CBN with a cubic boron nitride cutting edge.
Triangular insert designation decoder according to ISO 1832
how to read the TNMG 160408 code — positions 1–7 of the designation
Designation TNMG 160408 according to the standard ISO 1832: 4 letters describe geometry and construction, 3 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
Compatible turning tools
holders with a 16 triangular pocket — external and internal turning
TTJNR/L 2020 K1620×20 × 125 mmR right-hand
←L left-hand
→
←L left-hand
→
TTJNR/L 2525 M1625×25 × 150 mmR right-hand
←L left-hand
→
←L left-hand
→
TTJNR/L 3232 P1632×32 × 170 mmR right-hand
←L left-hand
→
←L left-hand
→
TTENN 2020 K1620×20 × 125 mmNeutral
↔
↔
TTENN 2525 M1625×25 × 150 mmNeutral
↔
↔
TTENN 3232 P1632×32 × 170 mmNeutral
↔
↔
TTGNR/L 2020 K1620×20 × 125 mmR right-hand
←L left-hand
→
←L left-hand
→
TTGNR/L 2525 M1625×25 × 150 mmR right-hand
←L left-hand
→
←L left-hand
→
TTGNR/L 3232 P1632×32 × 170 mmR right-hand
←L left-hand
→
←L left-hand
→
TTFNR/L 2020 K1620×20 × 125 mmR right-hand
←L left-hand
→
←L left-hand
→
TTFNR/L 2525 M1625×25 × 150 mmR right-hand
←L left-hand
→
←L left-hand
→
TTFNR/L 3232 P1632×32 × 170 mmR right-hand
←L left-hand
→
←L left-hand
→
MTJNR/L 2020 K1620×20 × 125 mmR right-hand
←L left-hand
→
←L left-hand
→
MTJNR/L 2525 M1625×25 × 150 mmR right-hand
←L left-hand
→
←L left-hand
→
MTJNR/L 3232 P1632×32 × 170 mmR right-hand
←L left-hand
→
←L left-hand
→
MTENN 2020 K1620×20 × 125 mmNeutral
↔
↔
MTENN 2525 M1625×25 × 150 mmNeutral
↔
↔
MTENN 3232 P1632×32 × 170 mmNeutral
↔
↔
S25S TTUNR/L-16ø25 × 250 mm | D min ≥32R right-hand
←L left-hand
→
←L left-hand
→
S32T TTUNR/L-16ø32 × 300 mm | D min ≥40R right-hand
←L left-hand
→
←L left-hand
→
S25S TT-NR/L-16ø25 × 250 mm | D min ≥32R right-hand
←L left-hand
→
←L left-hand
→
S32T TT-NR/L-16ø32 × 300 mm | D min ≥40R right-hand
←L left-hand
→
←L left-hand
→
S20R MTUNR/L-16ø20 × 200 mm | D min ≥25R right-hand
←L left-hand
→
←L left-hand
→
S25S MTUNR/L-16ø25 × 250 mm | D min ≥32R right-hand
←L left-hand
→
←L left-hand
→
S32T MTUNR/L-16ø32 × 300 mm | D min ≥40R right-hand
←L left-hand
→
←L left-hand
→
S40U MTUNR/L-16ø40 × 350 mm | D min ≥50R right-hand
←L left-hand
→
←L left-hand
→
S20R MTQNR/L-16ø20 × 200 mm | D min ≥25R right-hand
←L left-hand
→
←L left-hand
→
S25S MTQNR/L-16ø25 × 250 mm | D min ≥32R right-hand
←L left-hand
→
←L left-hand
→
S32T MTQNR/L-16ø32 × 300 mm | D min ≥40R right-hand
←L left-hand
→
←L left-hand
→
S40U MTQNR/L-16ø40 × 350 mm | D min ≥50R right-hand
←L left-hand
→
←L left-hand
→
Frequently asked questions about the TNMG 160408 insert
use, turning tool selection, and turning parameters
Six — the triangle has 3 corners per side, and the negative geometry (0° clearance angle) allows both sides of the insert to be used. Once a cutting edge becomes dull, simply index the insert in the tool holder pocket without replacing it.
Holders with a 16 triangular pocket (IC 9.525 mm): for external turning TTJNR/L and MTJNR/L (entering angle 93°), TTFNR/L and TTGNR/L (90°) and neutral TTENN/MTENN (60°) with shank cross sections of 20×20–32×32 mm; for internal turning, boring bars S20R–S40U with a TTUNR/L, MTUNR/L or MTQNR/L designation suffix.
Only in corner radius: 0.4 mm is used for finishing at low feed rates, 0.8 mm is the general-purpose version, and 1.2 mm is selected for roughing at feed rates up to 0.4–0.5 mm/rev. The other dimensions (IC 9.525 mm, thickness 4.76 mm) are identical.
Yes — grade H6310 covers group ISO M20-M40. Maintain a cutting speed of 80–260 m/min, a constant feed, and continuous emulsion cooling: austenitic steel conducts heat poorly and work-hardens when cutting is too slow.
Product accessories


Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you




Viewed products


This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.