





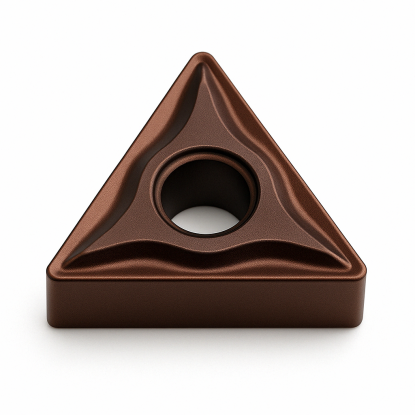

Description
| Technical data | |
|---|---|
| Side length l | 22 mm |
| Insert thickness s | 4.76 mm |
| Hole diameter d1 | 5.16 mm |
| Corner radius rε | 0.8 mm |
| ANSI code | TNMG 432 |
finishing, semi-finishing and roughing — ISO P and M groups
| Material | Finishing | Semi-finishing | Roughing | ||||||
|---|---|---|---|---|---|---|---|---|---|
| Vc [m/min] | Feed f [mm/rev] | ap [mm] | Vc [m/min] | Feed f [mm/rev] | ap [mm] | Vc [m/min] | Feed f [mm/rev] | ap [mm] | |
| PSteel | 250-350 | 0.1 | 0.25 | 180-270 | 0.2 | 1.5 | 170-220 | 0.4 | 2.5 |
| MStainless steel | 125-260 | 0.1 | 0.25 | 100-220 | 0.2 | 1.5 | 80-200 | 0.4 | 2.5 |
double-sided 60° triangle with a hole and chip breaker
The TNMG 220408 turning insert is a double-sided, triangular indexable insert made of H6310 grade cemented carbide, designed for turning steel and stainless steel. The T shape, an equilateral triangle with a 60° corner angle, facilitates access to the workpiece contour during longitudinal turning and facing. Negative geometry with a 0° clearance angle allows both sides of the insert to be used — a total of six cutting edges. The nose radius rε 0.8 mm combines a good surface finish with edge strength at feed rates of 0.2–0.4 mm/rev. The hole with a chip breaker on both sides (type G per ISO 1832) controls chip flow and breaking.
The TNMG 220408 insert (also written without a space as tnmg220408) is suitable for turning shafts, sleeves and flanges made of structural steels, as well as stainless steel components. The larger inscribed circle IC 12.7 mm (1/2″) and edge length of 22 mm withstand higher cutting forces than the variant for a size 16 pocket, making the insert suitable for heavier roughing passes. Calculate spindle speed using n = 1000·Vc/(π·D): for a shaft diameter of 80 mm at Vc = 250 m/min, the result is approximately 995 rpm. When machining stainless steels, maintain a cutting speed of 80–260 m/min and a constant feed to avoid work hardening of the layer being cut. H6310 grade indexable inserts are supplied by the Korean brand Horn.
In semi-finishing and roughing, effective chip control protects the machined surface and removes heat from the cutting zone. The double-sided type G chip breaker forms short, easily broken chips at feed rates as low as 0.15 mm/rev, facilitating operation on automatic lathes and turning centers. For external turning, select holders with a size 22 triangular pocket; for boring holes, select boring bars with a shank diameter of at least 32 mm. Use pressurized emulsion cooling, especially with austenitic stainless steel, which conducts heat poorly and work-hardens readily.
Grade H6310 is not intended for steels hardened above 45 HRC — for hard turning, select the version TNMG 220408 CBN with a cubic boron nitride cutting edge.
how to read the TNMG 220408 code — positions 1–7 of the designation
Designation TNMG 220408 according to the standard ISO 1832: 4 letters describe geometry and construction, 3 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
holders with a 22 triangular pocket — external and internal turning
use, turning tool selection, and turning parameters
Six — the triangle has 3 corners per side, and the negative geometry (0° clearance angle) allows both sides of the insert to be used. Once an edge becomes dull, simply rotate the insert in its pocket without changing the holder.
Holders with a 22 triangular pocket (IC 12.7 mm): for external turning TTJNR/L and MTJNR/L (entering angle 93°), TTFNR/L and TTGNR/L (90°) and TTENN and MTENN (60°) with shank cross sections of 25×25–40×40 mm; for internal turning, boring bars S32T–S50V with a TTUNR/L, MTUNR/L or MTQNR/L designation suffix.
Only in corner radius: 0.4 mm is used for finishing at low feed rates, 0.8 mm is the general-purpose version, and 1.2 mm is selected for roughing at feed rates up to 0.4–0.5 mm/rev. The other dimensions (IC 12.7 mm, thickness 4.76 mm) are identical.
Yes — grade H6310 covers group ISO M20-M40. Maintain a cutting speed of 80–260 m/min, a constant feed, and continuous emulsion cooling: austenitic steel conducts heat poorly and work-hardens when cutting is too slow.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


