





- 98% satisfied customers
- 72h delivery
- 30 dni na zwrot
Description
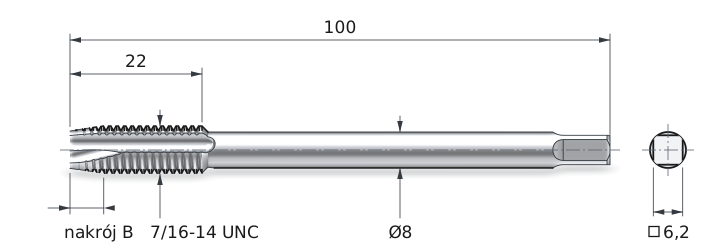
Technical data for the 7/16-14 UNC machine tap
| Technical data | |
|---|---|
| nominal diameter d1 | 7/16-14 |
| thread pitch P | 14 threads per inch |
| overall length l1 | 100 mm |
| flute length l2 | 22 mm |
| working length l3 | 15 mm |
| shank diameter d2 | 8 mm |
| square drive size | 6.2 mm |
| tap drill diameter | 9.3 mm |
| Chamfer | B (3.5÷5.5) P |
How the type B through-hole chamfer pushes chips down the hole
Chips exit at the bottom instead of returning through the thread
Through-hole chamfer B has a chip breaker at the front of the tap – an angled grind on the cutting edges. The chip breaker directs chips down the hole, ahead of the tap tip. The chips curl into coils, break into short pieces, and exit the hole on the other side of the workpiece. The threads already cut stay clean because chips do not pass through them on their way upward. The UNC 7/16-14 tap has a reduced shank in accordance with DIN 376: diameter 8 mm, square 6.2 mm.
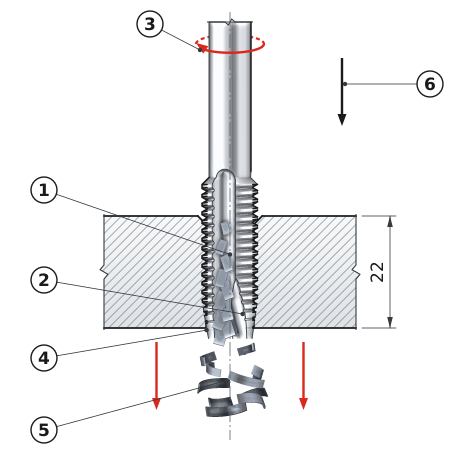
1
Straight flute – chips do not enter it; the flute carries lubricant to the cutting edges.
2
The chip breaker at the tip of the tap directs chips down the hole.
3
The tap rotates clockwise to cut a right-hand thread.
4
B chamfer: 3.5–5.5 incomplete threads on the entry taper.
5
The chips break into segments: individual pieces at the top of the hole, with progressively more farther down. They fall out below the workpiece.
6
The UNC 7/16-14 thread has 14 threads per inch; the feed is approximately 1.814 mm/rev.
7/16-14 UNC American machine tap for stainless steel
Modern 7/16-14 UNC machine tap with an extended reduced shank, compliant with DIN 376. The tap has a form B chamfer – for machining through holes and blind holes of various depths in materials producing short chips. Thread diameter: 7/16 inch, 14 threads per inch, tolerance class of the threads produced: 2B. Available from our store 7/16-14 UNC machine taps for Unified threads are made from special high-speed steel containing 5% cobalt – HSSE. This is an advanced steel with exceptional properties that significantly enhance the cutting capabilities of the taps. Above all, the tools withstand demanding operating conditions, including the high temperatures generated during high-speed cutting.
These machine taps also enable highly productive and precise machining. They can significantly reduce machining time and allow more efficient use of workstations. The taps are suitable for machining alloy steels, nonferrous metals, cast iron, cast steel, stainless steels, acid-resistant steels, and other hard materials.
Product accessories


UNC 7/16-14 DIN 376/37 C HSSE tapping
Reference: 0000006283 In stock < 10 items
€10.53
€12.95 brutto


Hand tap UNC 7/16-14 DIN 352/2 HSS 2B Fra
Reference: 0000007803 In stock < 10 items
€15.79
€19.42 brutto

Reviews
No customer reviews for the moment.
Shipping
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
Recommended for you


Viewed products

This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.
Cookie preferences
Functional cookiesTechnical
Functional cookies are strictly necessary to provide the services of the shop, as well as for its proper functioning, so it is not possible to refuse their use. They allow the user to browse through our website and use the different options or services that exist on it.
Advertising Cookies
These are cookies that collect information about the advertisements shown to users of the website. They can be anonymous, if they only collect information about the advertising spaces shown without identifying the user, or personalised, if they collect personal information about the user of the shop by a third party, for the personalisation of these advertising spaces.
Analytics cookies
Collect information about the user's browsing experience in the shop, usually anonymously, although sometimes they also allow the user to be uniquely and unequivocally identified in order to obtain reports on the user's interests in the products or services offered by the shop.