







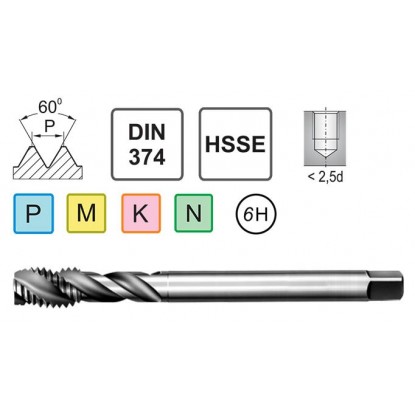

Description
| Technical Data | |
|---|---|
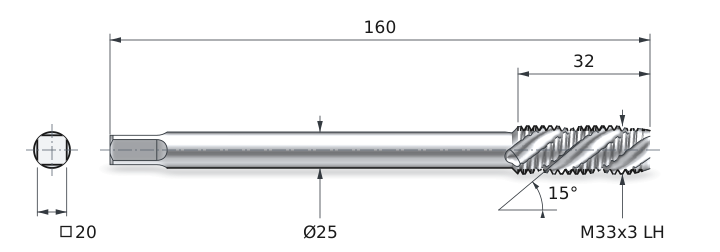
| Nominal Diameter d1 | M33x3 |
| Thread Pitch P | 3 mm |
| Overall Length l1 | 160 mm |
| Flute Length l2 | 32 mm |
| Shank Diameter d2 | 25 mm |
| Square Drive Size a | 20 mm |
| Tap Drill Diameter | 30 mm |
| Chamfer | C (2÷3) P |
| Thread tolerance | 6H |
| Cutting edge helix angle | 15° |
The 15° flute works like a screw conveyor
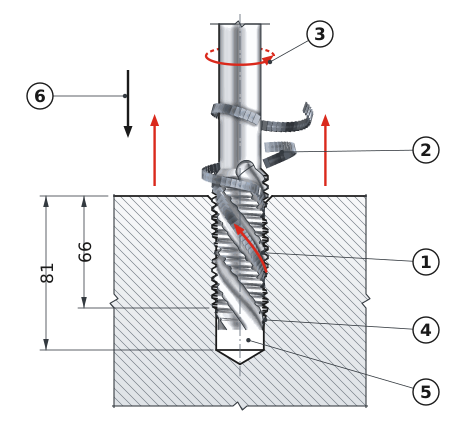
The flutes of this tap follow a left-hand helix at an angle of 15° to the axis. The tap rotates counterclockwise and advances into the hole. The chip cut by the chamfer enters the flute, and the helix feeds it upward like the auger in a meat grinder. The bottom of the hole stays clean, and the cutting edges do not encounter packed chips. The M33x3 tap has a reduced shank according to DIN 374: diameter 25 mm, square size 20 mm.
The HSSE series for manufacturing special components includes an M33x3 INOX left-hand machine tap with a 15° left-hand flute helix angle. The 6H tolerance conforming to DIN 374 ensures the dimensional repeatability required in manufacturing components with left-hand threads. Flute geometry with a 15° helix angle optimizes chip evacuation when tapping blind holes. HSSE steel construction with 5% cobalt ensures a hardness of 66 HRC and long cutting edge life in stainless and difficult-to-machine steels.
The M33x3 left-hand HSSE machine tap is designed for machining special components requiring left-hand threads. The M33x3 left-hand universal machine tap is compatible with automatic tool change systems with reverse rotation. The tap drill diameter is 30 mm.
| Material | Cutting speed Vc [m/min] | Spindle speed n [rpm] | Feed f [mm/min] |
|---|---|---|---|
| PSteel | 5-20 | 48-193 | 144–579 |
| MStainless steel / INOX | 5-10 | 48-96 | 144–288 |
| KCast iron | 5-15 | 48-145 | 144–435 |
| NAluminum | 10-25 | 96-241 | 288–723 |
NC spotting drill 90°
Ø 30 mm
M33x3
Tolerance 6H
Standard: DIN 374 | Chamfer: C (spiral flute) | Application: general-purpose (through and blind holes)
| Class | Accuracy | Application | Status |
|---|---|---|---|
| 4H / 4g | High | Precision connections, hydraulics | — |
| 6H / 6g | Standard | Machine building, general-purpose | SELECTED |
| 7H / 8g | Low | Large clearance, easy assembly | — |
6H = internal thread (nut, hole) | 6g = external thread (screw)
The M33x3 left-hand HSSE tap is suitable for 304 and 316 austenitic stainless steels, structural steels up to 800 MPa, ductile cast iron, and aluminum and brass alloys. It is not recommended for hardened steels above 45 HRC.
The nominal tap drill diameter for the M33x3 left-hand thread is 30 mm. The hole tolerance should be within the range of 29.9–30.1 mm. A hole at the lower tolerance limit produces a fuller thread profile, while one at the upper limit reduces tapping torque.
M33x3 left-hand threads are used in components protected against self-loosening, clockwise-rotating drive shafts, and screws securing grinding wheels. They prevent the joint from loosening under vibration.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


