





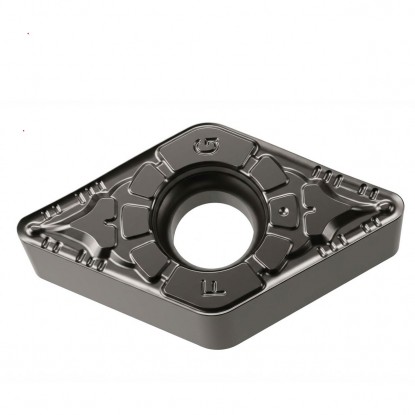

Description
| Technical data | |
|---|---|
| Side length l | 11.6 mm |
| Insert thickness s | 4.76 mm |
| Hole diameter d1 | 3.81 mm |
| Corner radius rε | 0.8 mm |
| ANSI code | DNMG 332 |
precision machining, medium machining, and roughing — ISO group K
| Material | Finishing | Semi-finishing | Roughing | ||||||
|---|---|---|---|---|---|---|---|---|---|
| Vc [m/min] | f [mm/rev] | ap [mm] | Vc [m/min] | f [mm/rev] | ap [mm] | Vc [m/min] | f [mm/rev] | ap [mm] | |
| KGray cast iron | 200–350 | 0.10 | 0.20 | 150–250 | 0.15 | 2.00 | 120–200 | 0.25 | 3.50 |
| KDuctile cast iron | 180–280 | 0.10 | 0.20 | 130–220 | 0.15 | 2.00 | 100–180 | 0.30 | 3.50 |
double-sided 55° diamond with a hole and chip breaker for cast iron
The DNMG 110408 turning insert is a double-sided, diamond-shaped indexable insert made of grade H5115 cemented carbide, designed for cast iron turning. Shape D, a diamond with a 55° corner angle, facilitates profile turning and access to the workpiece contour while maintaining a strong cutting edge. Negative geometry with a 0° clearance angle allows both sides of the insert to be used — a total of four cutting edges. The nose radius rε of 0.8 mm combines a good surface finish with edge durability when turning castings. The hole with a chip breaker on both sides (type G according to ISO 1832) controls chip flow.
Grade H5115 belongs to ISO group K, which covers cast irons. The hard CVD coating increases cutting edge wear resistance in contact with the abrasive structure of the casting. This allows the insert to maintain stable workpiece dimensions during longer turning runs. Tolerance class M ensures repeatable corner positioning after indexing the insert in the tool holder pocket. The CVD coating is thicker than a thin PVD coating, so it withstands wear better during long production runs, but performs best with continuous cutting edge contact and rigid workpiece clamping.
The DNMG 110408 insert (also written without spaces as dnmg110408) is suitable for precision external turning and boring of gray, ductile, and malleable iron castings. The CVD coating dissipates heat and allows high cutting speeds, reaching approximately 350 m/min in gray cast iron. Calculate spindle speed using n = 1000·Vc/(π·D): for a shaft diameter of 60 mm at Vc = 250 m/min, the result is approximately 1326 rpm. For ductile cast iron, reduce the cutting speed to 100–280 m/min, as the material is more ductile and places a greater load on the cutting edge. During interrupted turning, ensure rigid workpiece clamping to limit corner chipping. Indexable inserts in grade H5115 are supplied by the Korean brand Horn.
Grade H5115 with a coating of CVD is dedicated to cast iron (ISO group K). For turning stainless steel or gummy materials, choose a general-purpose grade with a coating of PVD — on these materials, the hard CVD coating and negative geometry promote built-up edge formation.
how to read the DNMG 110408 code — designation positions 1–7
Designation DNMG 110408 according to the standard ISO 1832: 4 letters describe geometry and construction, 3 numeric codes describe dimensions. Each field has a number, an icon, and a brief description.
holders with a 11 diamond-shaped pocket — external and internal turning
use, turning tool selection, and turning parameters
Four — the diamond has 2 corners of 55° per side, and the negative geometry (0° clearance angle) allows both sides of the insert to be used. Once an edge becomes dull, simply rotate the insert in its pocket without changing the holder.
Holders with a 11 diamond-shaped pocket (IC 9.525 mm): for external turning TDJNR/L (entering angle 93°) and TDNNN (62.5°) with shank cross sections of 16×16–25×25 mm; for internal turning, boring bars S25S and S32T with a TD-NR/L, TDQNR/L, or TDUNR/L head.
Only in corner radius: 0.4 mm is used for finishing at low feed rates, 0.8 mm is the general-purpose version, and 1.2 mm is selected for roughing at higher feed rates. The remaining dimensions (IC 9.525 mm, thickness 4.76 mm) are identical.
Grade H5115 with a CVD coating is optimized for cast iron (group ISO K). Steel can be turned occasionally, but for structural steel it is better to select a grade dedicated to group P, which will provide longer cutting edge life.
No customer reviews for the moment.
All orders are delivered by courier company GLS. For orders exceeding 369 PLN gross shipping is FREE
| Courier GLS | Przelew24 / Prepayment | 14,76 zł gross | Delivery time 1 working day |
| Courier GLS | Cash on delivery | 17,26 zł gross | Lead time 1 working day |
This website uses its own and third-party cookies to improve our services and show you advertising related to your preferences by analyzing your browsing habits. To give your consent to its use, press the Accept button.


